How do you choose a mountaineering backpack manufacturer? You evaluate five technical systems rather than a catalogue: the suspension (framesheet, stay and back panel), the load transfer interface (hip belt and lumbar contact), the fabric and coating specification, the load-bearing hardware and stitch schedule, and the water management strategy. A manufacturer who can quote all five with numbers, show a sample room separate from mass production, and document inline QC is a mountaineering manufacturer; one who can only quote capacity and colour is a general bag factory. JUNYUAN BAGS builds technical packs to standard MOQ of 500 pcs per style and colour, sampling in 6–10 business days, bulk production in 35–50 days, AQL 2.5 / 4.0 inspection, FOB Xiamen with DDP available by arrangement.
Mountaineering is the most specification-sensitive segment in the bag industry. A daypack that carries 6 kg can survive imprecise construction; a 55 L pack that carries 20 kg across uneven ground cannot. Every shortcut in the suspension or the stitch schedule becomes a field failure, and field failures in this category are read as safety failures.
What Makes a Mountaineering Backpack Different From a Hiking Daypack?
Three structural thresholds separate the categories, and each one changes what the factory has to be able to do.
- Load magnitude. A daypack carries 5–8 kg on the shoulders. A mountaineering pack carries 15–25 kg, which must be transferred to the hips through a frame rather than hung from the shoulders.
- Structural frame. Below roughly 12 kg, foam and a stiffener are sufficient. Above it, you need a framesheet with an aluminium or composite stay, and a hip belt structurally connected to that frame rather than sewn to the back panel.
- Failure consequence. A torn daypack pocket is an inconvenience. A failed shoulder attachment at altitude is an emergency. This is why the stitch schedule, not the fabric, is the real quality differentiator in this category.
The Five Technical Systems You Are Actually Buying
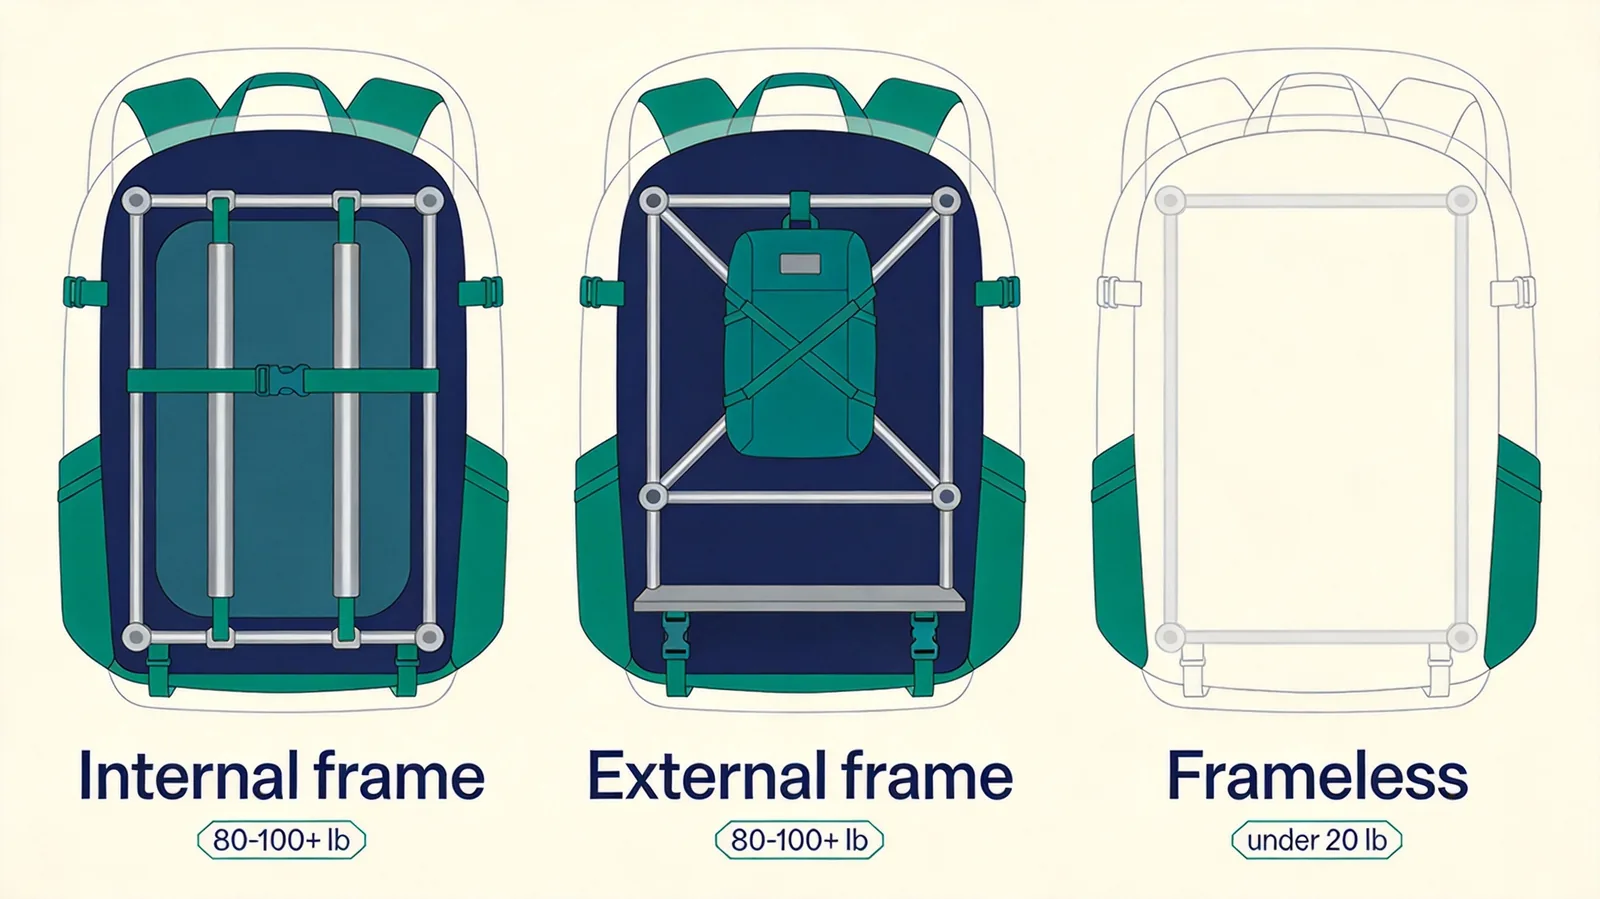
When you place a mountaineering order, you are not buying a bag. You are buying five engineering decisions, and each one has to be specified numerically or the factory will choose for you.
1. Suspension: framesheet, stay and back panel
The suspension is the pack’s skeleton. Specify the framesheet material and thickness (HDPE sheet at 1.5–2.0 mm is the common baseline), the stay type (single aluminium stay, twin stays, or a composite rod), and the back panel construction (moulded foam with a ventilation channel, or a flat padded panel).
Two specification failures recur. First, a framesheet that is stiff enough but not wide enough — the load concentrates at the centre of the back instead of spreading across the lumbar. Second, a stay pocket that is not reinforced at the base, so the stay wears through the fabric at the point of maximum flex after a season of use.
2. Load transfer: hip belt and lumbar interface
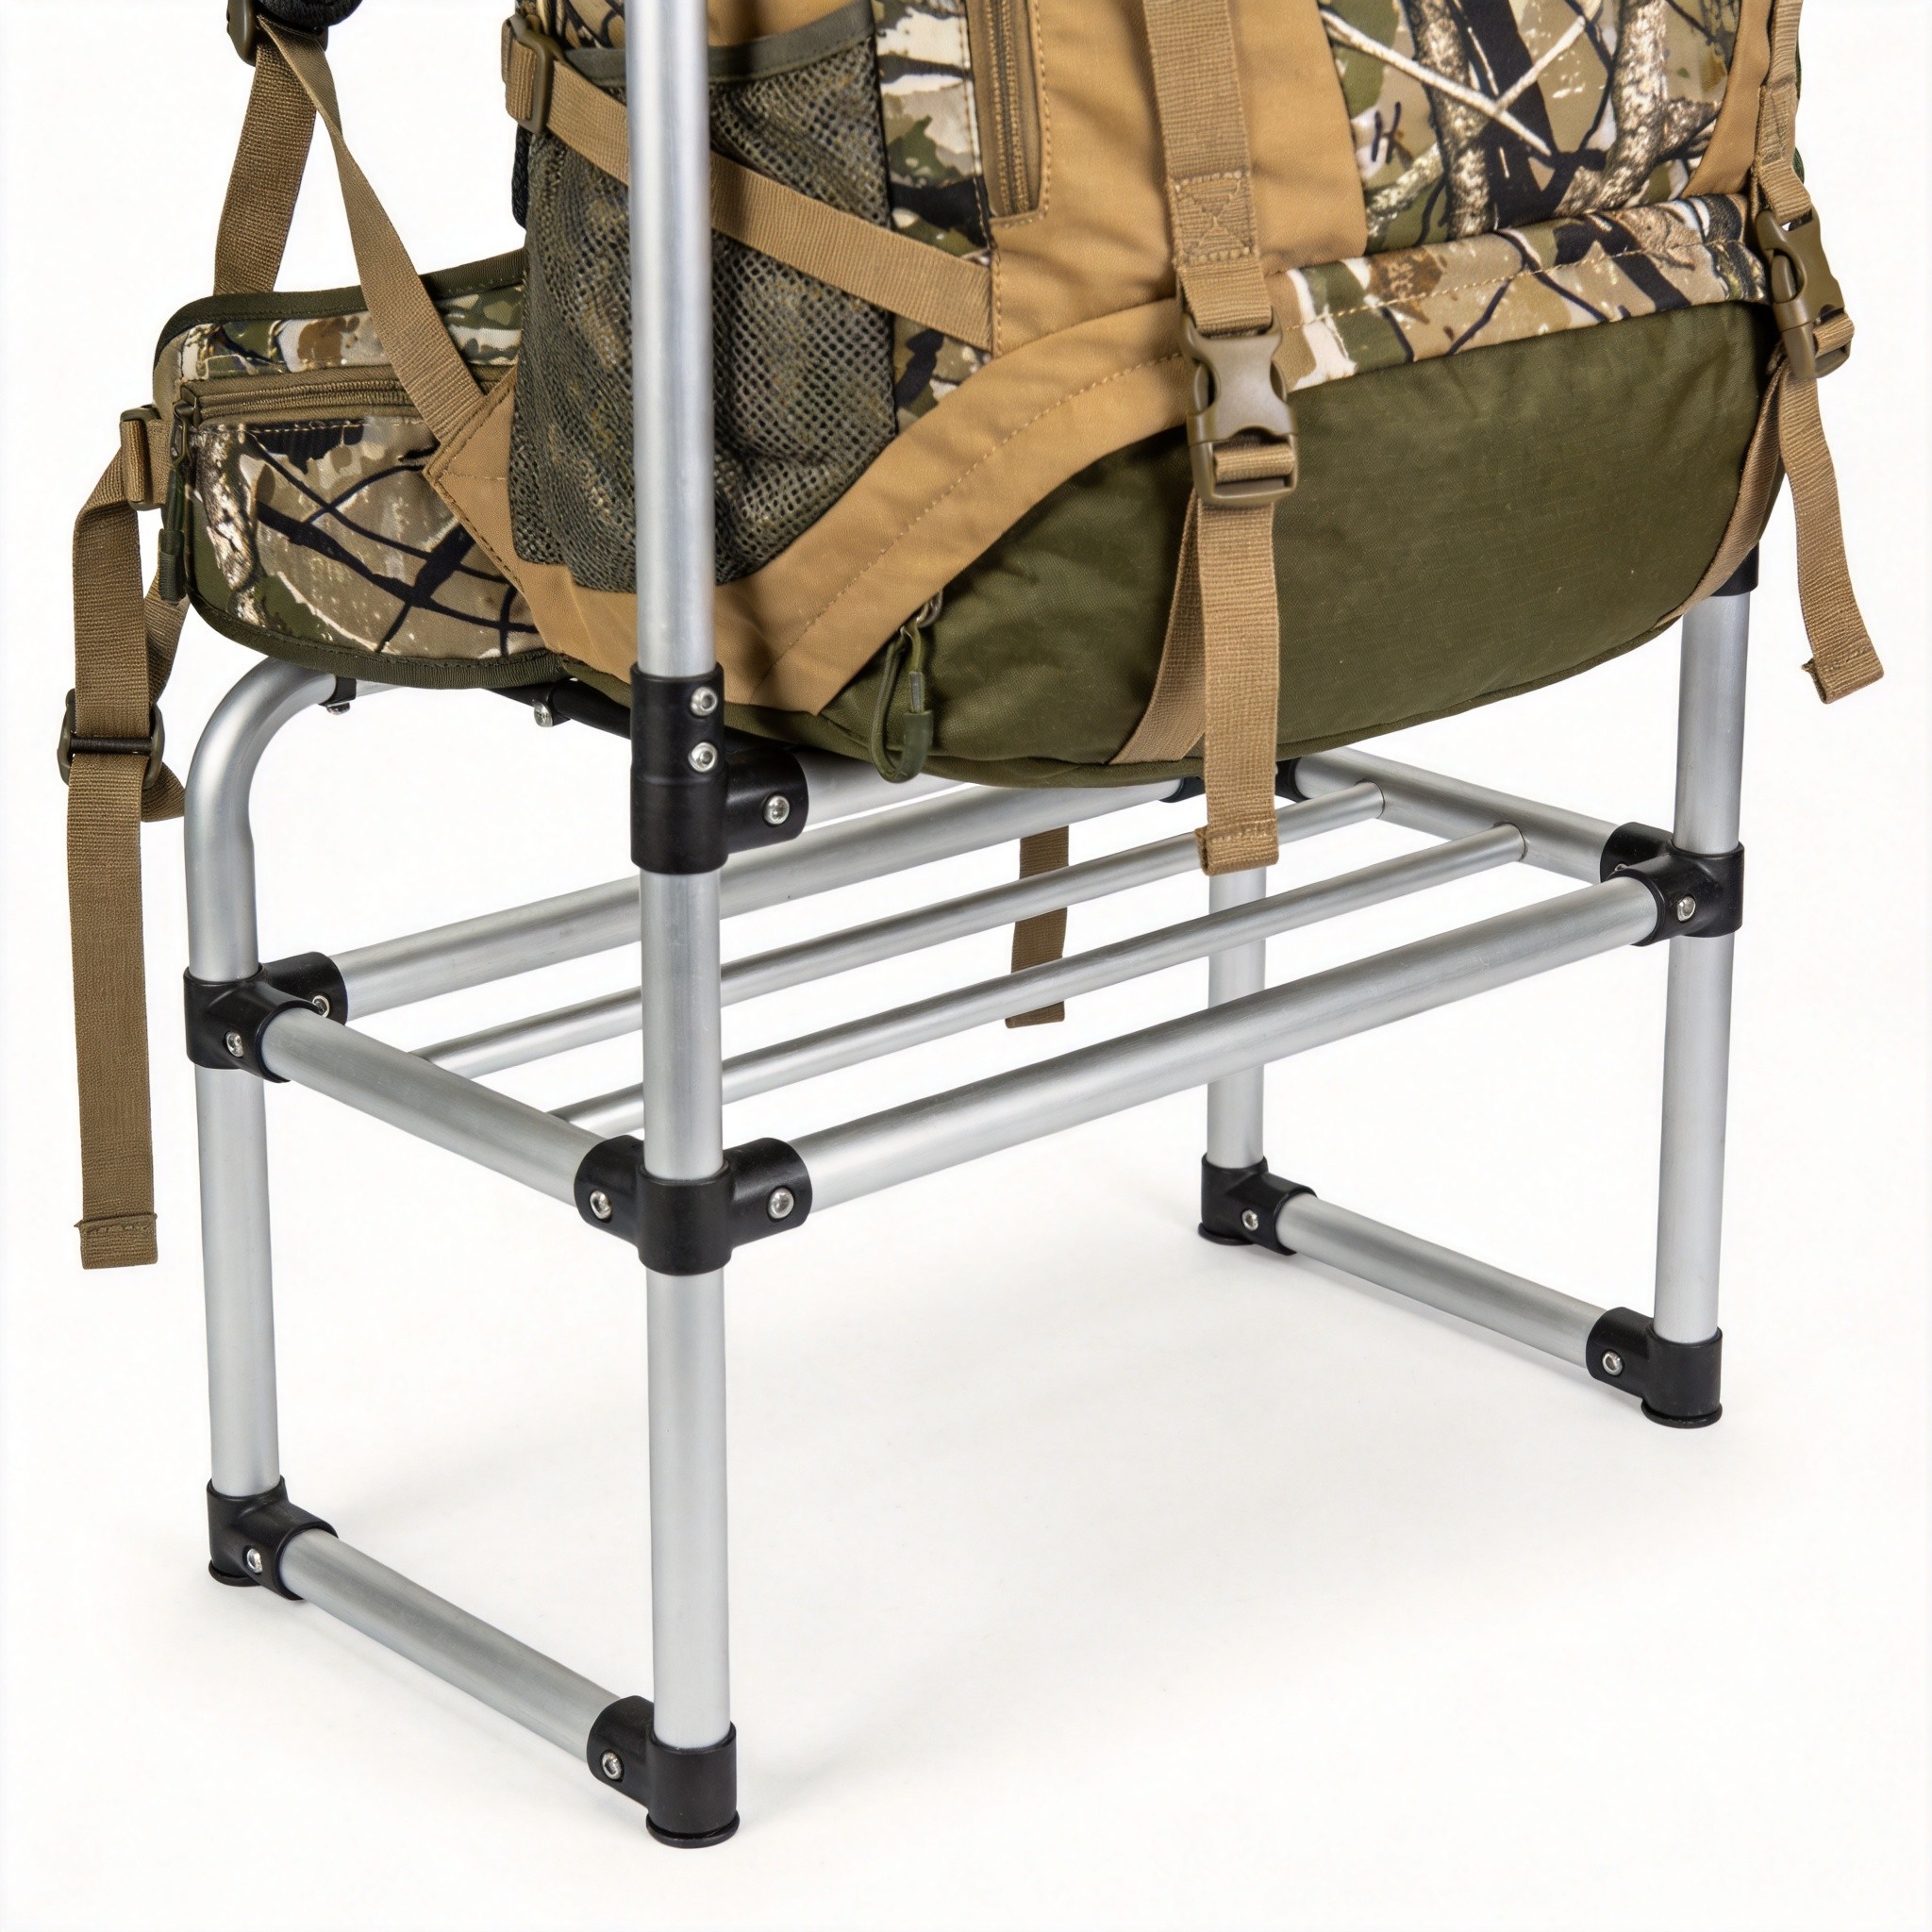
The hip belt is where a mountaineering pack succeeds or fails. The belt has to be structurally continuous with the frame, which means the attachment is bar-tacked through the framesheet rather than sewn to the back panel shell.
Specify belt foam thickness (20–30 mm for a load-bearing belt), belt width at the iliac crest (100–130 mm), and the closure system (single buckle, double buckle, or a cam-lock). A belt that is wide but thin will roll under load; a belt that is thick but narrow will dig in. Both are visible in a loaded wear test and neither is visible in a photograph.
3. Fabric: CORDURA, X-PAC and ripstop nylon
Fabric selection in this category is a trade between abrasion resistance, weight and waterproofing. Denier alone tells you very little — ask for grams per square metre and the coating type alongside the denier figure, because a 500D fabric at 200 g/m² and a 500D fabric at 320 g/m² behave differently in the field and cost differently per metre.
Coating matters as much as the weave. PU coating is flexible and cheap but degrades with hydrolysis over years in storage. TPU and TPEE coatings resist hydrolysis better and cost more. Aqueous coatings are the current low-VOC option and require the factory to control drying temperature carefully, which is a capability question rather than a material question.
4. Hardware: buckles, webbing and load-bearing stitches
Hardware in this category is not decorative. Specify buckle brand and model — YKK and Duraflex are the two names most technical brands specify — and specify the webbing (polyester vs nylon, 20 mm vs 25 mm, and the tensile rating).
The stitch schedule is the specification most buyers omit and the one that decides field life. A load-bearing seam should be double-row stitched at 8–10 stitches per inch with bonded polyester thread, box-X or bar-tacked at every terminal point. A single-row seam at 6 stitches per inch will pass a visual inspection and fail under cyclic load.
5. Water management: coating, seam sealing and drainage
Water resistance is a system, not a fabric property. Specify the coating on the shell fabric, whether critical seams are taped or sealed, whether the zippers are water-resistant with a sealed garage, and whether the pack body has a drainage eyelet at the base.
A common specification error is treating a water-resistant zipper as waterproof without sealing the seam it is sewn into. The zipper tape seam is the actual leak path, and it is the cheapest place to fix a problem before production and the most expensive after.
Fabric Selection by Segment
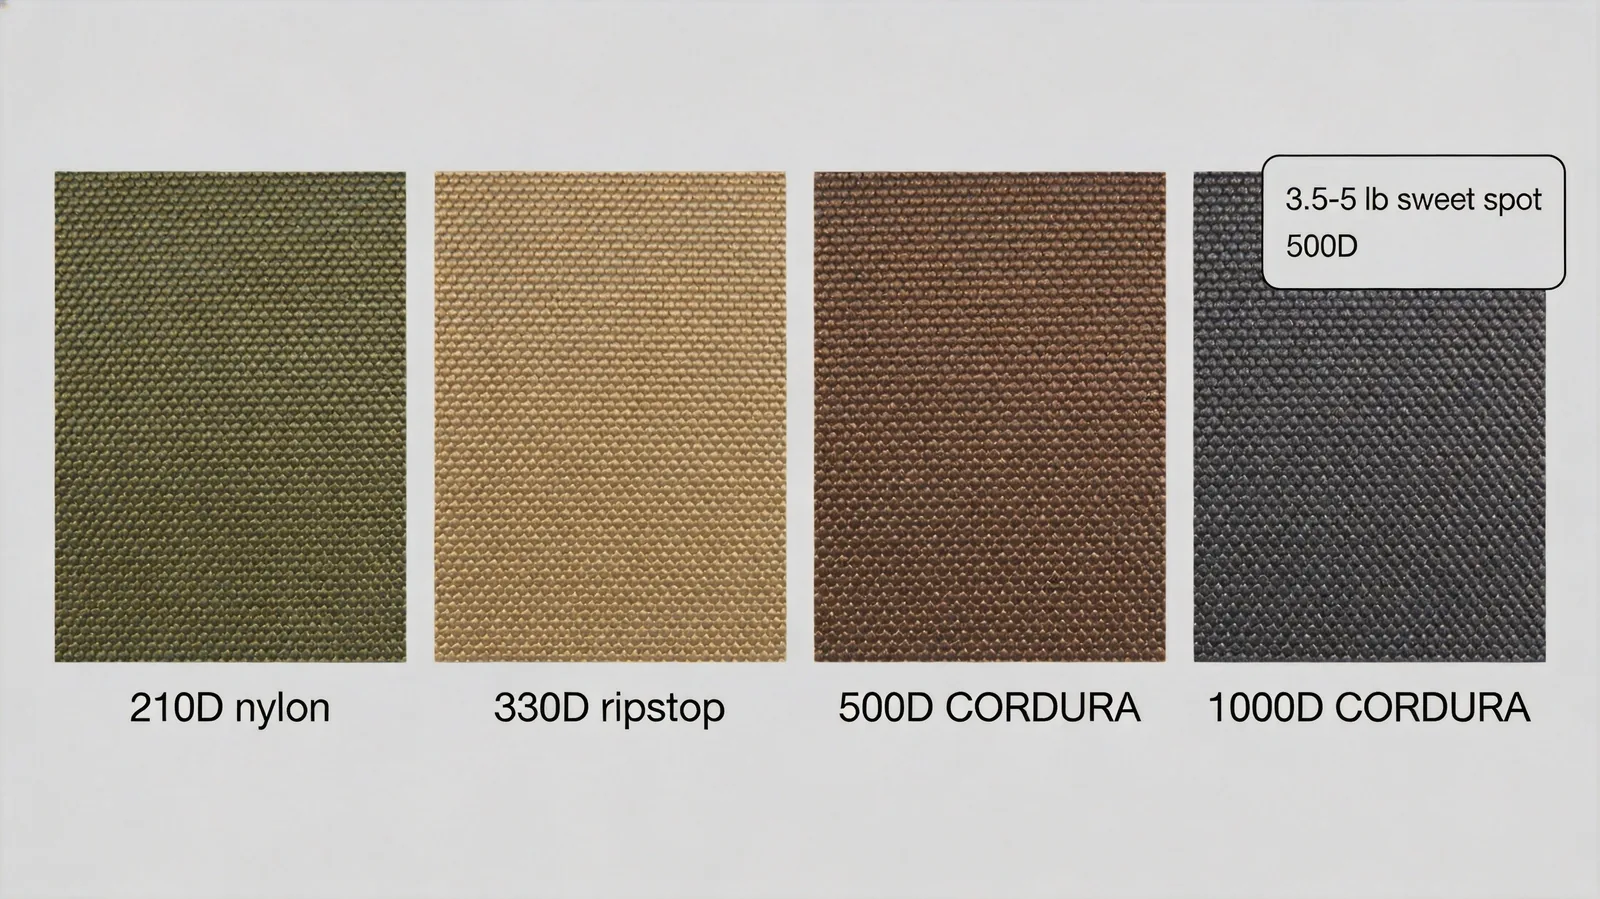
| Segment | Shell fabric | Weight range | Coating | Typical use |
|---|---|---|---|---|
| Ultralight | 70–100D ripstop nylon | 60–110 g/m² | Silicone or PU 1,000–1,500 mm | Fast-and-light, summer alpine |
| Standard alpine | 210D ripstop nylon | 130–180 g/m² | PU 1,500–2,000 mm | Three-season mountaineering |
| Technical / expedition | 420D–500D high-tenacity nylon | 200–280 g/m² | PU or TPU 2,000–3,000 mm | Winter and expedition loads |
| Abrasion-critical panels | 500D–1,000D CORDURA® | 250–400 g/m² | PU, often uncoated base | Base, side panels, crampon zone |
| Weatherproof laminate | X-PAC® style laminate | 150–220 g/m² | Inherent laminate, taped seams | Wet climates, high-exposure use |
Branded fabrics carry a specification and a cost: CORDURA® and laminate systems such as X-PAC® are verifiable by the mill’s own documentation, which means a factory quoting them can be held to them. Unbranded equivalents may be functionally similar and cannot be verified, which matters if your brand makes a fabric claim on the product page.
Hardware and Stitch Specifications
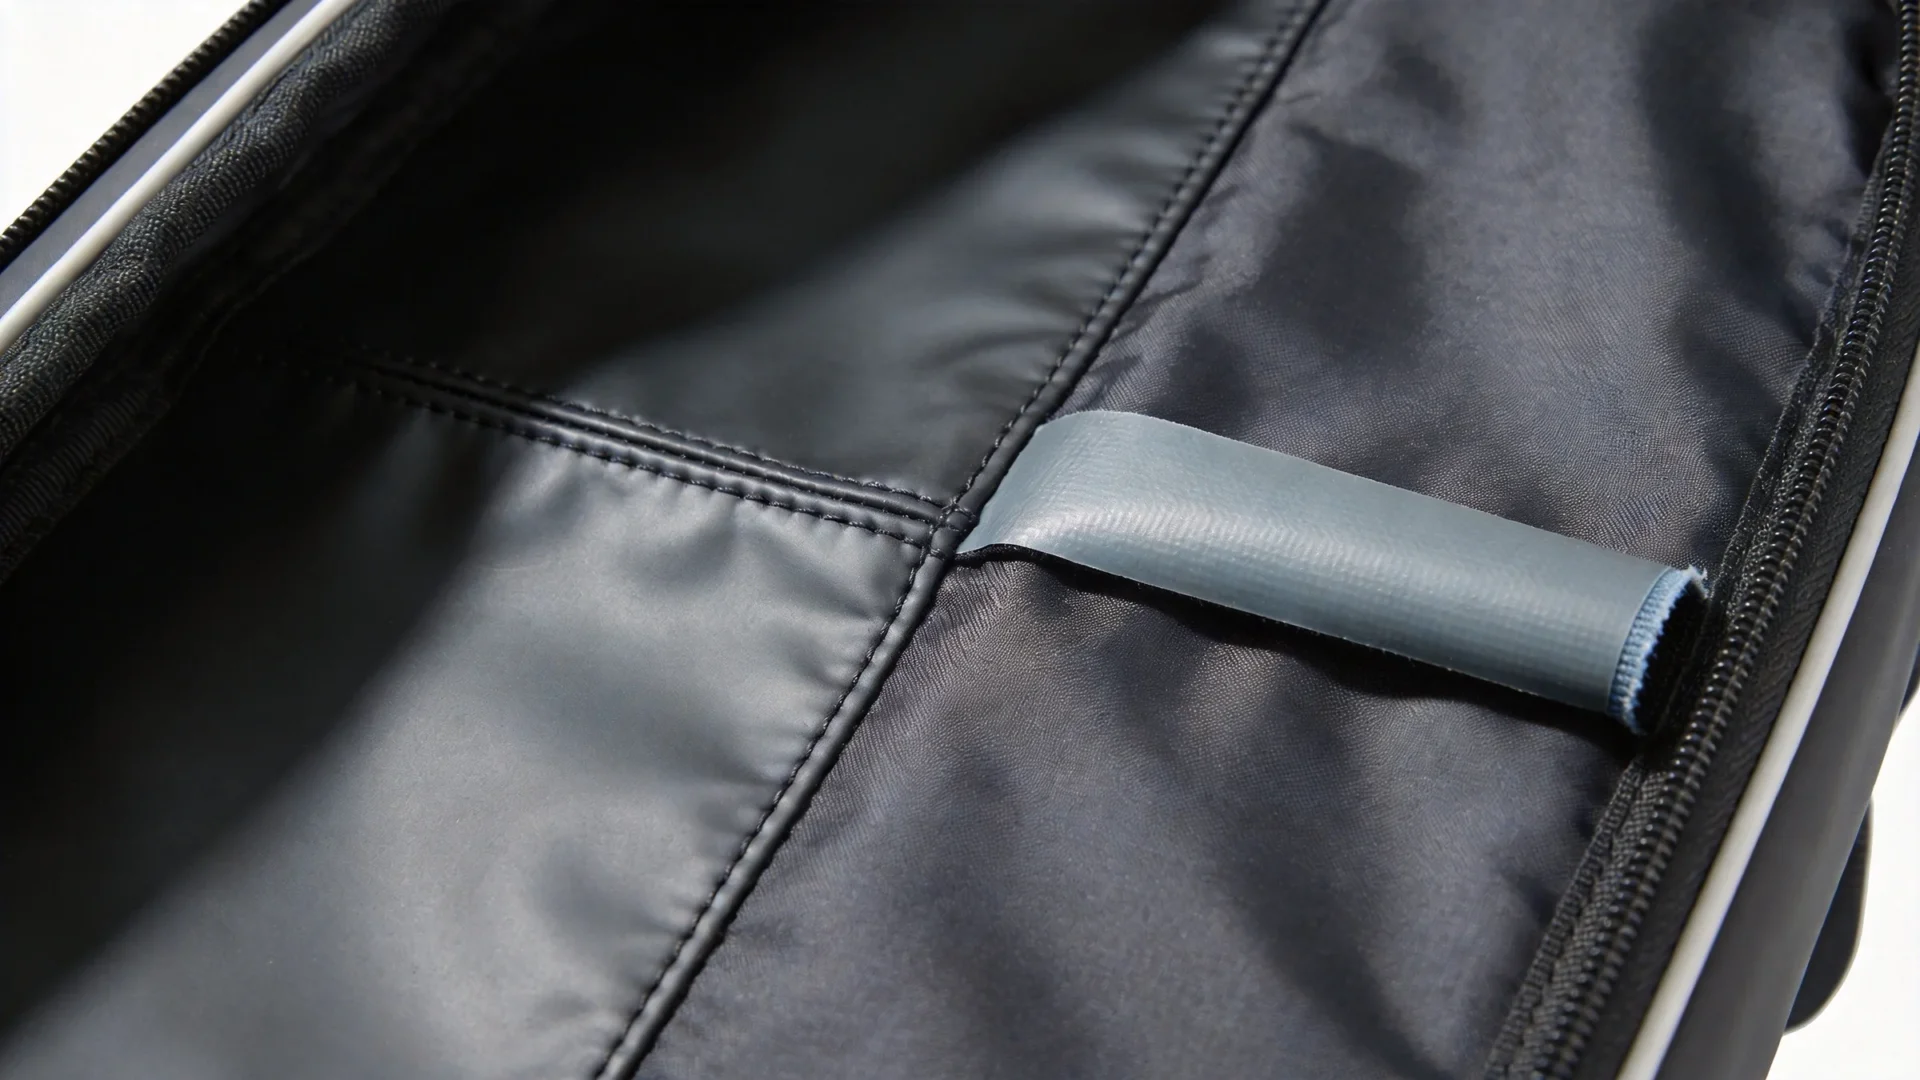
| Component | Minimum specification | Where it fails if under-specified |
|---|---|---|
| Main compartment zipper | #8 or #10 coil, branded slider | Slider splits under load; coil deforms at the curve |
| Load-bearing webbing | 25 mm polyester, rated tensile | Stretch and creep over a season |
| Buckles | Branded acetal, 20–25 mm | Brittle fracture in cold |
| Load-bearing seam | Double-row, 8–10 SPI, bonded thread | Seam failure under cyclic load |
| Terminal points | Box-X or bar-tack at every end | Ripping starts at the seam end |
| Stay pocket base | Reinforced patch at flex point | Stay wears through the fabric |
| Hip belt attachment | Bar-tacked through framesheet | Belt separates from pack under load |
What Separates a Mountaineering Manufacturer From a General Bag Factory
| Capability | Mountaineering manufacturer | General bag factory |
|---|---|---|
| Structural engineering | In-house pattern and frame design, load path modelled | Copies an existing shape |
| Sample room | Dedicated technical sample room, separate from production | Sample made on the production line between orders |
| Fabric handling | Laminates, ripstop and high-tenacity nylon; controlled cutting tension | Polyester and 600D oxford |
| Seam sealing | Hot-air taping or seam sealing capability | Not available |
| Stitch control | Documented SPI and thread spec per seam | Operator discretion |
| Testing | Load, tear and abrasion testing with recorded results | Visual inspection only |
| Inline QC | Staged checks during assembly, not only at final | Final inspection only |
| Technical documentation | Bill of materials with mill references | Generic material description |
The clearest single test is the bill of materials. A manufacturer who can issue a BOM naming the mill, the article number and the measured g/m² for each fabric is operating at the technical level this category requires. A factory that answers a fabric question with “strong nylon” is not.
Capacity, Load and Frame Matching
| Volume | Design load | Frame requirement | Hip belt requirement |
|---|---|---|---|
| 20–30 L | 6–10 kg | Foam stiffener or light framesheet | Minimal, removable webbing belt |
| 30–40 L | 10–14 kg | Framesheet with single stay | Padded belt, 20 mm foam |
| 40–55 L | 14–20 kg | Framesheet with single or twin stay | Load-bearing belt, 25 mm foam, bar-tacked to frame |
| 55–75 L | 20–25 kg | Twin stay or composite frame, load-lifter straps | Load-bearing belt, 30 mm foam, dual closure |
| 75 L+ | 25 kg+ | Full external or heavy internal frame | Full wrap belt with structural connection |
Volume and load are not the same number. A 45 L pack built for 12 kg and a 45 L pack built for 20 kg use the same shell dimensions and different frames, belts and stitch schedules. Specify the design load, not just the volume, or the factory will default to the lighter construction because it costs less to make.
Testing and Certification You Should Require
| Test | What it verifies | How to require it |
|---|---|---|
| Static load test | Frame and belt attachment hold at rated load | Specify load and hold time; request recorded results |
| Cyclic load test | Seams survive repeated loading | Specify cycle count; request a test report |
| Tear strength | Fabric resistance to propagation | Request mill data or in-house test values |
| Abrasion resistance | Base and panel durability | Request Martindale or Taber results if claimed |
| Coating adhesion and hydrostatic head | Water resistance claim is real | Request mm rating per fabric, per colour |
| Colourfastness to light and rubbing | Colour holds in UV and against straps | Request grade values for each colourway |
| Final inspection to AQL 2.5 | Workmanship consistency across the lot | Specify ISO 2859-1 sampling and attend inspection |
Testing is where a technical program differs most from a volume program. A general factory will offer a visual final inspection; a mountaineering manufacturer will have recorded load and seam data it can show you before you ask. Ask for one test report at the quotation stage and judge the answer by how quickly it arrives.
How to Evaluate a Mountaineering Backpack Manufacturer
- Ask for a BOM before a price. A manufacturer who can issue a bill of materials with mill references, article numbers and measured weights is operating technically. One who quotes a price first is selling a shape.
- Request one test report at the quotation stage. Static load or seam strength. Speed of response tells you whether the data exists or has to be produced for the occasion.
- Ask how the sample room is staffed. A dedicated technical sample room with its own pattern makers and sewers is the single strongest capability signal in this category.
- Confirm the framesheet and belt attachment method in writing. Bar-tacked through the framesheet, not sewn to the back panel shell. This is the specification most often quietly downgraded between quote and production.
- Walk the line, live or by dated video. Look for the seam-sealing station and the stitch-length gauge at the machines. Their presence or absence answers most of the capability question.
- Ask what the factory will not make. A technical manufacturer has a clear boundary — it will tell you which constructions it declines. A factory that says yes to everything has not understood the question.
- Confirm inspection access and AQL. You or a third party should be able to attend final inspection. A manufacturer who resists inspection access is subcontracting or has no inline QC to protect.
- Ask for two references in the same segment. Not brand names in general — references for packs in the same volume and load class, contacted about on-time delivery and field returns.
The verification logic here is the same as in general bulk sourcing channel selection, but the bar is higher because the failure consequence is higher. Buyer-side screening frameworks such as this manufacturer versus supplier comparison apply here with less tolerance for ambiguity.
Sampling and Production Timelines for Technical Packs
| Stage | Duration | What happens | What can delay it |
|---|---|---|---|
| Tech pack review | 1–2 days | Feasibility, frame and load path review, fabric availability | Incomplete load specification |
| Pattern and prototype | 3–5 days | Pattern making, frame forming, first assembly | New hardware moulds |
| Sample build | 2–3 days | Sewing, seam sealing, hardware fitting | Coating or laminate lead time |
| Internal review and ship | 1–2 days | Load test on the sample, photo set, courier | Load test failure and rework |
| Total sampling | 6–10 business days | JUNYUAN standard for technical packs | — |
| Bulk production | 35–50 days | Cutting, assembly, sealing, final inspection | Dyed-to-Pantone fabric, new moulds |
Common Failures in Mountaineering Backpack Programs
- Specifying volume but not design load. The factory builds the lighter construction because it costs less, and the pack fails at the rated weight.
- Accepting a framesheet without specifying width. Load concentrates at the spine instead of spreading across the lumbar.
- Leaving the stitch schedule to the factory. Single-row seams at low SPI pass visual inspection and fail under cyclic load.
- Treating a water-resistant zipper as waterproof. The zipper tape seam is the leak path and it is rarely sealed unless specified.
- Skipping the loaded wear test on the sample. Unloaded samples hide belt roll, shoulder slip and frame flex, which are the three failures buyers actually notice.
- Choosing fabric by denier alone. Two 500D fabrics at different g/m² and different coatings are different products at different prices.
Mountaineering Backpack Manufacturing Questions
Q1: What is the MOQ for custom mountaineering backpacks?
JUNYUAN BAGS standard MOQ is 500 pcs per style and colour for custom technical packs, with volume pricing from 5,000 pieces. Technical construction carries a higher effective minimum than a simple daypack because pattern making, frame forming and seam-sealing setup are fixed costs that do not shrink with order size.
Q2: How long does sampling and production take for a technical pack?
The schedule is 6–10 business days for sampling, then 35–50 days for bulk once the sample is approved and the deposit has cleared. Both windows extend if you specify fabric dyed to a Pantone reference or a new hardware mould, since those sit upstream of the pattern stage.
Q3: Which fabric should I choose for a mountaineering backpack?
Match the fabric to the segment rather than the price. Ultralight packs use 70–100D ripstop at 60–110 g/m²; three-season alpine packs use 210D ripstop at 130–180 g/m²; expedition packs use 420–500D high-tenacity nylon at 200–280 g/m², with 500D–1,000D CORDURA® on the base and abrasion-critical panels. Always specify g/m² and coating type alongside denier.
Q4: Do I need a framesheet or is foam enough?
Below roughly 12 kg design load, foam with a stiffener is sufficient. Above it, a framesheet with an aluminium or composite stay is required, and the hip belt has to be structurally connected to that framesheet rather than sewn to the back panel shell. Specify design load, not volume, when briefing the factory.
Q5: What stitch specification should I require?
Double-row stitching at 8–10 stitches per inch with bonded polyester thread on all load-bearing seams, and box-X or bar-tack reinforcement at every terminal point. Put the SPI and thread specification in the tech pack. Left unspecified, the factory will use the fastest setting that passes a visual check.
Q6: How can I tell if a factory really makes technical packs?
Three signals: a bill of materials with mill references and measured weights, a sample room staffed separately from production, and a seam-sealing station on the line. A general bag factory has none of the three, and will answer a fabric question with a generic description rather than an article number.
Q7: What testing should a mountaineering backpack manufacturer provide?
At minimum static load, cyclic load and seam strength, plus fabric tear and abrasion data where claimed, coating adhesion and hydrostatic head per fabric and colour, and colourfastness grades. Final inspection should run to AQL 2.5 under ISO 2859-1. Ask for one report at the quotation stage and judge the response time.
Q8: Is CORDURA worth the cost premium over generic nylon?
It is worth it where the brand makes a durability claim, because branded fabric is verifiable against the mill’s documentation and can be held to in production. Generic high-tenacity nylon may perform similarly and cannot be verified. Use branded fabric on abrasion-critical panels and generic fabric where the claim is not made.
Q9: How do I keep water out of a mountaineering backpack?
Treat it as a system: coated shell fabric with a stated hydrostatic head, taped or sealed critical seams, water-resistant zippers with a sealed garage, and a drainage eyelet at the base. The most common error is specifying a water-resistant zipper without sealing the tape seam it is sewn into, which is where the water actually enters.
Q10: What is a realistic design load for each volume class?
20–30 L: 6–10 kg. 30–40 L: 10–14 kg. 40–55 L: 14–20 kg. 55–75 L: 20–25 kg. 75 L and above: 25 kg+. These are design targets rather than limits, and they determine the frame and belt specification. A pack built for 12 kg at 45 L and one built for 20 kg at 45 L share dimensions and not much else.
Q11: Can I visit the factory before placing an order?
Yes, and for a technical program you should. What you are looking for on the line is specific: the seam-sealing station, stitch-length gauges at the machines, a separate sample room, and documented inline checks between assembly stages. A dated video walkthrough is an acceptable substitute if travel is impractical.
Q12: What payment terms are normal for technical pack orders?
30% deposit with 70% before shipment is standard, with letters of credit used for larger orders. For a first technical program, tie the balance to a passed final inspection rather than a shipping date, and put inspection rights, rework liability and the approved sample reference into the purchase order.
Q13: How do I protect a technical design from being copied?
Use an NDA before sharing the tech pack, and share pattern files only after the order is confirmed. Practical protection also comes from specification depth: a design defined by a full BOM, stitch schedule and frame drawing is harder to copy meaningfully than a design defined by photographs.
Q14: What is AQL 2.5 and is it strict enough for technical packs?
AQL 2.5 is the acceptance quality limit defined under ISO 2859-1 and used across most consumer goods programs. For technical packs, AQL 2.5 on workmanship is a reasonable baseline, but it does not substitute for the structural tests — load, seam and belt attachment — which verify engineering rather than appearance. Run both.
Start a Mountaineering Backpack Program
Send JUNYUAN BAGS a dimensioned tech pack with design load, frame requirement and target fabric specification. You will get back a BOM-level review, a structural recommendation and a firm FOB Xiamen price within 12 hours. Sampling runs 6–10 business days, bulk production 35–50 days, and final inspection to AQL 2.5 is open to you or your third-party inspector.
Further reading across adjacent categories: what top-rated hiking backpacks specify, choosing a bulk sourcing channel, classifying travel backpacks by capacity and load, first-time buyer tips, and the wholesale laptop backpack specification guide. Capability detail sits on the custom backpack manufacturing page, the company profile and QC process, or contact the OEM/ODM team.