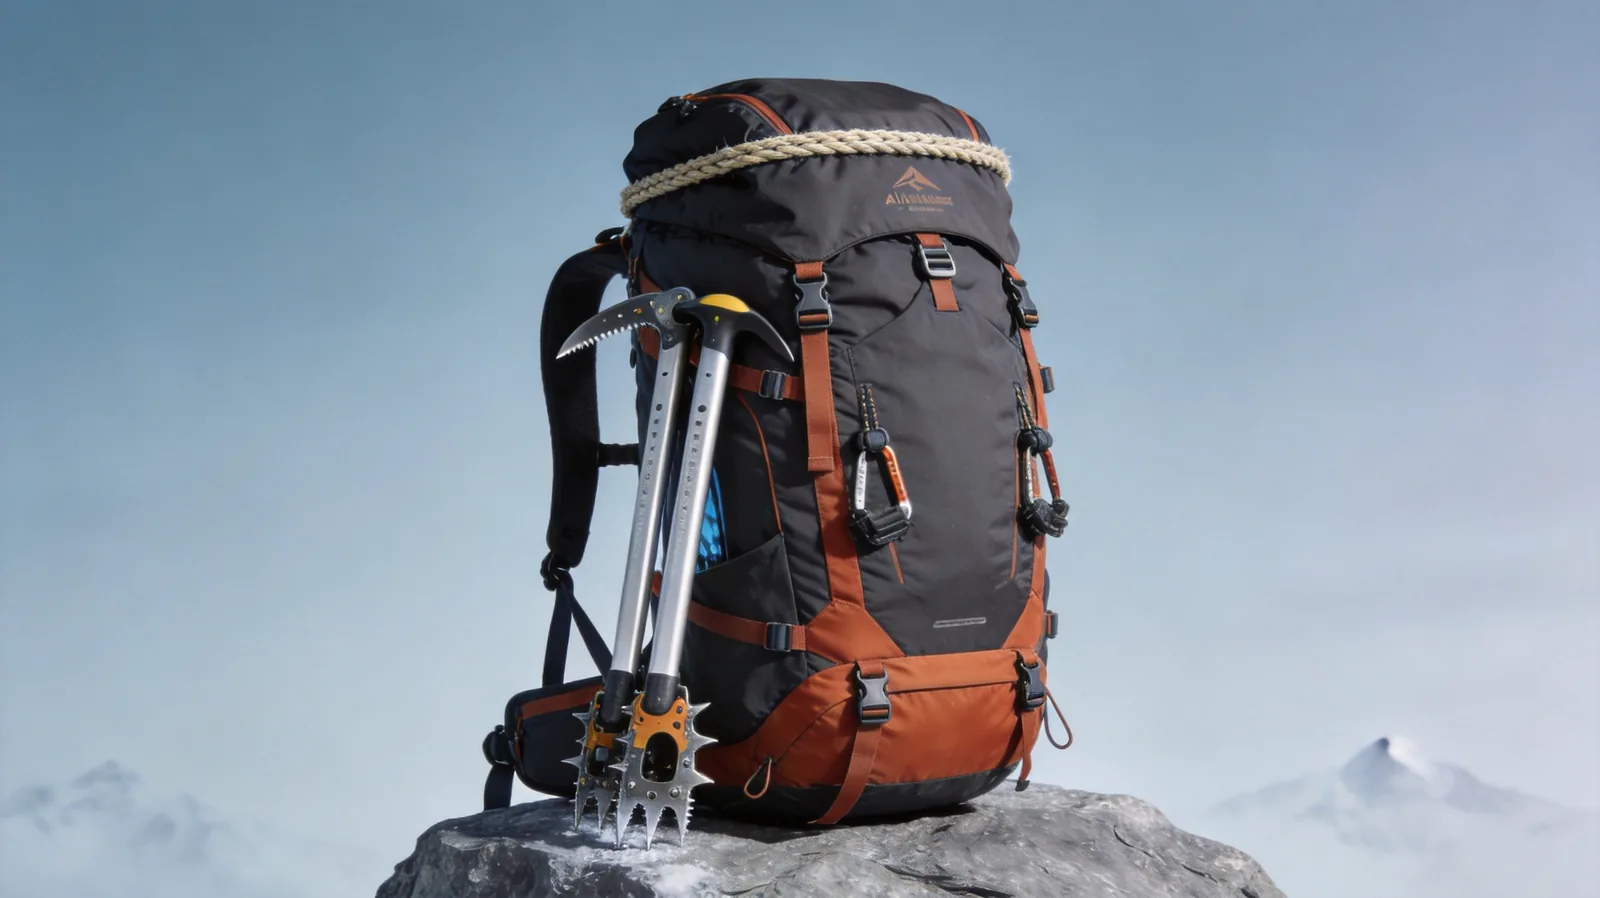
Mountaineering packs are the hardest category in the bag industry to manufacture well, and the easiest to manufacture badly without anyone noticing until a customer is on a north face at minus fifteen with a broken buckle. The category sits at the intersection of three constraints that pull against each other: functional attachment systems that have to survive dynamic shock loads, materials and hardware that must keep working below freezing, and a weight budget that buyers negotiate in tens of grams.
It is also the highest-value category per unit in the outdoor bag segment. A technical alpine pack that retails at €280–€450 carries a very different margin structure from a 40 L daypack, and the buyers are different people: professional guiding outfits, alpine equipment brands, ski mountaineering specialists and expedition logistics companies, not general consumers browsing a marketplace.
This guide is written for the brand or sourcing manager who is building a technical pack line and needs to know what actually has to be engineered, what actually has to be tested, and what the European regulatory position actually is. That last point matters more than most suppliers admit, because mountaineering is one of the few bag categories where there is a real certification regime, and almost nobody applies it correctly.
Why Mountaineering Packs Are a Different Manufacturing Problem
The cleanest way to understand the category is to stop thinking about capacity and start thinking about failure consequences. A trekking pack that fits badly produces a sore shoulder. A mountaineering pack whose ice axe loop tears out at the wrong moment produces a dropped tool on a belay ledge. The engineering tolerance for functional failure is simply narrower, and that changes what you specify, how you test, and what you are willing to accept in a sample.
Three constraints define the design space, and every technical decision is a trade against at least one of them.
| Constraint | What it forces | What it costs | Typical failure if neglected |
|---|---|---|---|
| Attachment functionality | Reinforced bar-tack zones, load-bearing webbing paths, dedicated tool and crampon interfaces | Weight, labour time, pattern complexity | Anchor tears out under dynamic load; tool lost |
| Cold-weather reliability | POM or impact-modified nylon hardware, TPU or PU coatings, cold-flex-tested foam | Unit cost of hardware, coating cost | Buckle shatters at first impact below freezing |
| Weight budget | Thinner face fabrics, reduced foam, frameless or minimal-frame construction | Durability, comfort margin, repair rate | Pack fails abrasion at high-stress points within a season |
What makes this category difficult for a factory is that these three constraints are not independent. Cutting 150 g by dropping from 210D to 70D face fabric also removes the substrate that a bar-tacked ice axe loop is anchored into, which means the reinforcement has to be redesigned rather than simply carried over. Dropping foam from the hip belt to save weight changes how the belt behaves at −20 °C, because EVA loses rebound resilience as it approaches its glass transition. A supplier who treats a technical pack as a hiking pack with extra straps will produce something that looks correct in a photograph and fails in the field.
There is also a manufacturing discipline difference. Technical packs are low-volume, high-variation products. A single brand might run 28 L, 35 L, 45 L and 65 L alpine models in three colourways each, with shared hardware but different pattern geometry, different frame specifications and different attachment layouts. That is a production-planning problem as much as a sewing problem, and it is why the factories that are genuinely good at this category tend to be the ones that have invested in pattern engineering rather than just cutting capacity.
The 2026 Alpine Market: Sub-40L Growth Against Expedition Decline
The headline growth number for the category is modest, but the composition shift underneath it is not, and the composition shift is what should drive your product plan.
Global mountaineering bag revenue was USD 3,250.0 million in 2025 and is projected to reach USD 4,712.06 million by 2032, a CAGR of 5.45%, with 2026 estimated at USD 3,300.55 million (PW Consulting, 2026). Regional distribution in 2025 was North America USD 1,020 million, Europe USD 952.1 million, Asia Pacific USD 880.1 million, Latin America USD 239.5 million and Middle East and Africa USD 160.2 million.
The more useful data point is the sell-through split. Specialty outdoor retail data for 2024–2025 shows pack volumes under 40 L growing 14% while traditional expedition packs above 60 L declined 3% (Outdoor Industry Association and European Outdoor Group, cited in the same report). The same source puts the under-40L segment at 38.5% of 2025 volume, the largest single capacity band.
By application, hiking and trekking still dominate at 56.3% of the market, but the technical segments are where the margin sits: mountaineering and climbing accounted for USD 935.52 million in 2025, with skiing and snowboarding at USD 485.18 million. The climbing backpack sub-segment specifically was valued at USD 810.0 million in 2025, projected to USD 1,283.77 million by 2032 at a 6.8% CAGR, with 2026 at USD 874.13 million. Within that, expedition and technical packs took 50.10% of revenue (USD 405.81 million), daypacks 39.93% and specialised bouldering bags 9.97% (PW Consulting, 2026).
Europe represents roughly 31% of the climbing pack market and close to 29% of the broader mountaineering bag market, which is disproportionately high relative to its population because alpine terrain, established guide culture and a dense specialty retail footprint concentrate technical demand. If you are building a technical pack line for European distribution, you are targeting the second-largest regional pool with the most demanding specification expectations.
One caution on market sizing. Published figures for this category diverge sharply depending on definition: some houses put mountaineering backpacks at USD 2.8 billion in 2025, others at USD 1.2 billion in 2024, because they draw the boundary between hiking, trekking, climbing and mountaineering differently. Do not build a business case on a single number. Use the direction and the composition shift, which are consistent across sources, rather than the absolute value.
Four Technical Pack Archetypes
“Mountaineering backpack” is not one product. It covers at least four distinct archetypes with different engineering priorities, and a factory that can build one cannot necessarily build the others well. Before you brief a supplier, decide which archetype you are actually ordering.
| Archetype | Capacity | Carried load | Priority | Frame | Weight target |
|---|---|---|---|---|---|
| Alpine climbing pack | 28–45 L | 7–14 kg | Strip-down modularity, tool access while wearing gloves | Removable framesheet or single stay | 700–1,100 g |
| Expedition pack | 65–110 L | 20–30 kg | Load transfer, snow skirt, expandable collar | Dual aluminium stays plus HDPE board | 2,000–2,900 g |
| Ski touring pack | 30–45 L | 8–15 kg | Ski and snowboard carry, airbag compatibility, back access | Framesheet with rigid ski-carry load path | 1,000–1,500 g |
| Cragging / bouldering pack | 20–40 L | 6–12 kg | Abrasion resistance, gear loops, rope tarp integration | Frameless or minimal | 600–1,000 g |
Alpine climbing packs (28–45 L)
The defining requirement is that the pack must be strippable. Lid, frame, hip belt and sometimes the entire back panel come off so the pack can be compressed for a summit push and rebuilt for the approach. That modularity is a design and tooling problem, not a materials problem: every removable component needs a reliable attachment interface that does not rattle, does not ice up and does not add 40 g of hardware per connection point.
Expedition packs (65–110 L)
Here the engineering returns to load transfer, but at a load level that makes trekking packs look easy. A 28 kg expedition load with a week of food and fuel puts continuous compressive load through the frame and the hip belt for ten hours a day. Frame stay diameter, hip belt wingspan and lumbar contact area all have to be specified for that sustained case, and the pack has to survive being dragged, sled-hauled and sat on. Expedition packs are where cheap hardware fails most visibly, because the loads find every weak point.
Ski touring packs (30–45 L)
Ski carry is a structural requirement disguised as a feature. A diagonal or A-frame ski carry puts the ski’s mass outside the pack body, on a lever arm, transmitting torque into the side panel and the compression straps during a traverse. The load path has to run from the upper ski strap anchor through the side panel into the frame, and it has to hold when the pack is wet, icy and being loaded and unloaded with gloves on. Back-panel access is also common in this archetype, which conflicts with the frame position and has to be resolved in the pattern.
Cragging and bouldering packs (20–40 L)
This is the archetype that overlaps most with climbing rather than mountaineering, and it is covered in more detail in the climbing section below. The engineering priority flips from cold performance to abrasion resistance, because these packs live on granite, sandstone and gym floors rather than on snow.
Attachment System Engineering: The Real Differentiator
Attachment systems are where technical packs earn or lose their reputation, and where most OEM samples fail first. The reason is that attachment points are almost never loaded statically. An ice axe clipped to a shaft holder sees a dynamic shock every time the wearer steps down hard, catches a branch, or drops the pack onto rock. A crampon pouch loaded with steel spikes at −15 °C becomes a rigid mass that levers against its own stitching. A rope strap loaded with a wet 60 m half rope carries roughly 4 kg of dead weight swinging on a single bar-tack line.
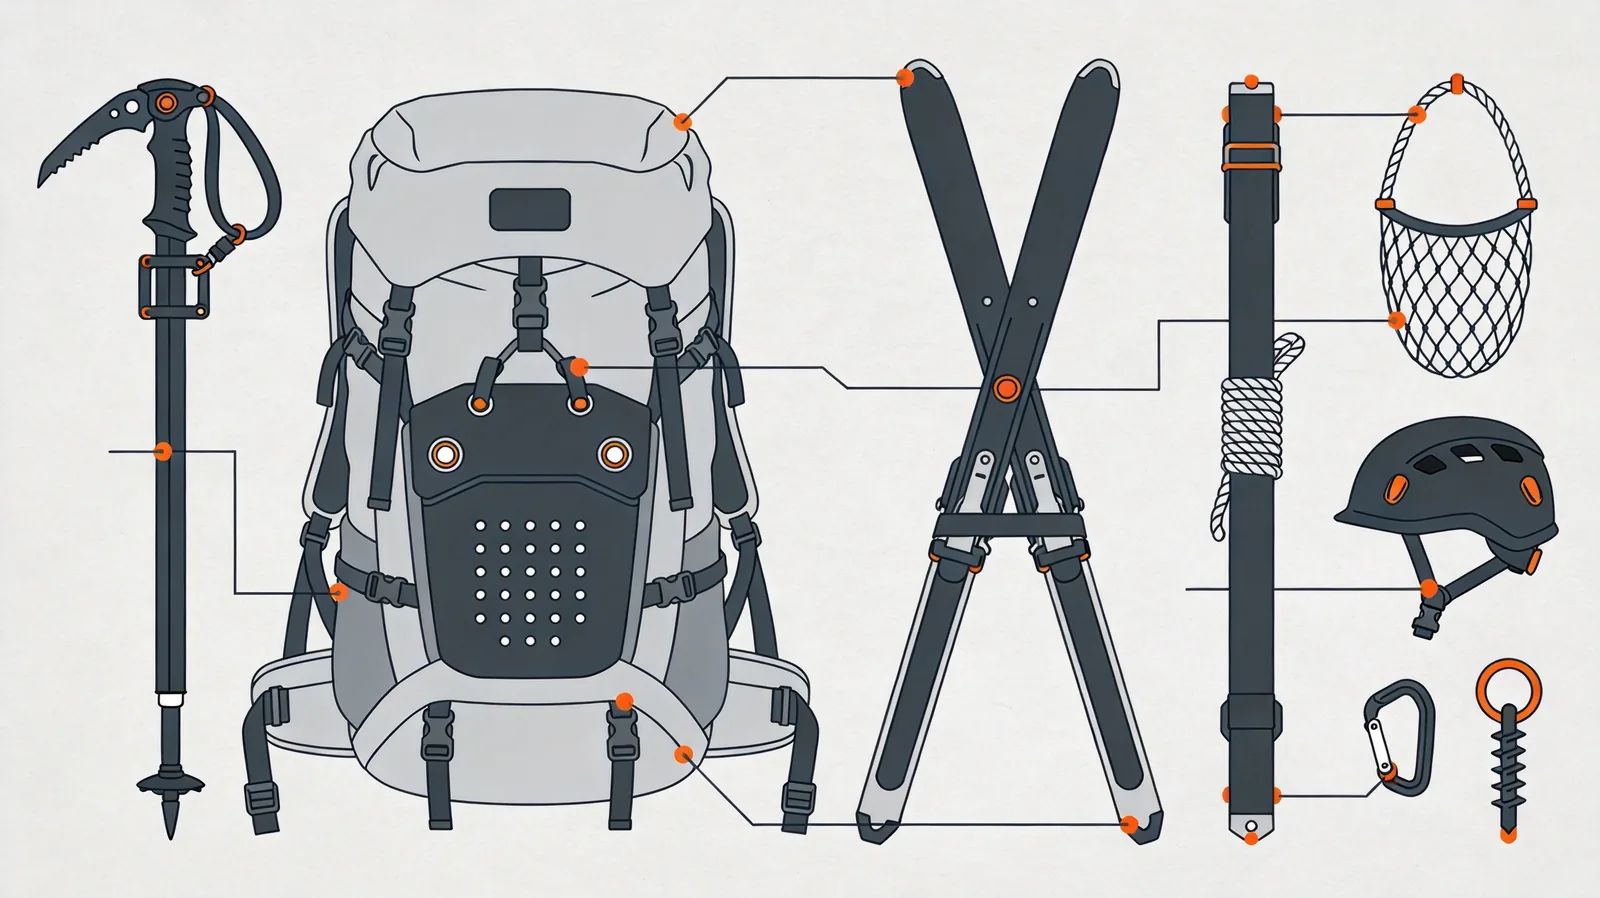
The table below sets out the attachment interfaces we engineer as standard on a technical pack, the load case each one has to survive, and the failure mode we see most often when a sample is under-specified.
| Interface | Function | Load case to design for | Common failure mode |
|---|---|---|---|
| Ice axe head loop | Retains pick head, allows one-handed stow | Dynamic shock from tool weight on a 200–300 mm arm | Bar-tack pulls through unreinforced face fabric |
| Ice axe shaft holder | Secures shaft to pack body | Repeated insertion and removal with gloves | Hook deforms or elastic loses tension below freezing |
| Crampon pouch | Stores steel points away from fabric | 4–8 kg rigid mass, abrasion from spikes | Points puncture pouch base; no drainage, water freezes inside |
| A-frame ski carry | Carries pair of skis on pack sides | Torque through side panel during traverse | Side panel distortion; lower strap anchor tears |
| Diagonal ski carry | Carries skis across the back | Asymmetric load, swinging mass | Upper anchor migrates; strap abrades on ski edges |
| Rope strap | Secures coiled rope under lid | 3–5 kg wet rope, dynamic swing | Single-stitch anchor; strap cuts into lid fabric |
| Helmet net | External helmet retention | 400–600 g helmet, wind load | Elastic over-stretch; net hooks bend |
| Ice screw / carabiner loops | Rack attachment | Repeated clipping with metal hardware | Webbing edge abrasion from carabiner gate |
| Daisy chain | General lashing and clip-in points | Multiple small loads, abrasion | Loop stitching abrades; chain anchors into thin fabric |
| Probe and shovel sleeve | Avalanche rescue tool storage | Fast access under stress, rigid aluminium shaft | Too tight for gloved access; sleeve drains poorly |
How attachment anchors are actually built
An attachment anchor is a load path, not a patch of webbing. The load enters at the hardware, travels through the webbing, transfers into the face fabric at the stitch line, and then has to be distributed into the pack body or the frame. If any link in that chain is weaker than the load, the anchor fails at the weakest link, which is almost always the point where the webbing meets unreinforced fabric.
Our standard build for a load-bearing anchor is a bar-tack at eight stitches per 30 mm, backed by a reinforcement panel of the same or higher denier as the face fabric, with the anchor positioned so the load path runs toward a seam or a frame element rather than into an unsupported panel centre. On sub-100 g/m² face fabrics we add a laminated or bonded reinforcement patch rather than relying on stitching alone, because a bar-tack in 70D fabric will simply tear out under dynamic load regardless of how many stitches it has.
For reference on what a serious load case looks like: EN 16716, the avalanche airbag standard, tests the carrying system by mounting the pack on a test torso to EN 12277, loosening the shoulder straps against the load direction, and applying 3 kN for one minute. That is a normative requirement for airbag packs specifically, not for general mountaineering packs, but it is a useful sanity check on what “load-bearing” should mean when you are writing a specification for a pack that will be worn while someone is being loaded onto a belay.
Testing attachment points in production
We pull-test every load-bearing attachment on a sampled basis at 200–400 N held for one minute, with no visible stitch deformation, no fabric distortion and no movement of the anchor. On airbag-compatible models the carrying system is tested to the 3 kN case above. Inline hardware such as buckles and hooks is functionally cycled at the specified cold temperature rather than at room temperature, because a buckle that releases cleanly at 20 °C can be immovable at −15 °C with gloves on.
Cold-Environment Material Behaviour: What Changes Below −15 °C
Cold is not a gradual performance penalty. It is a set of thresholds, and materials cross them at different temperatures. A pack specified only at room temperature can pass every test in a factory and still fail on its first winter outing, and the failures cluster in predictable places.
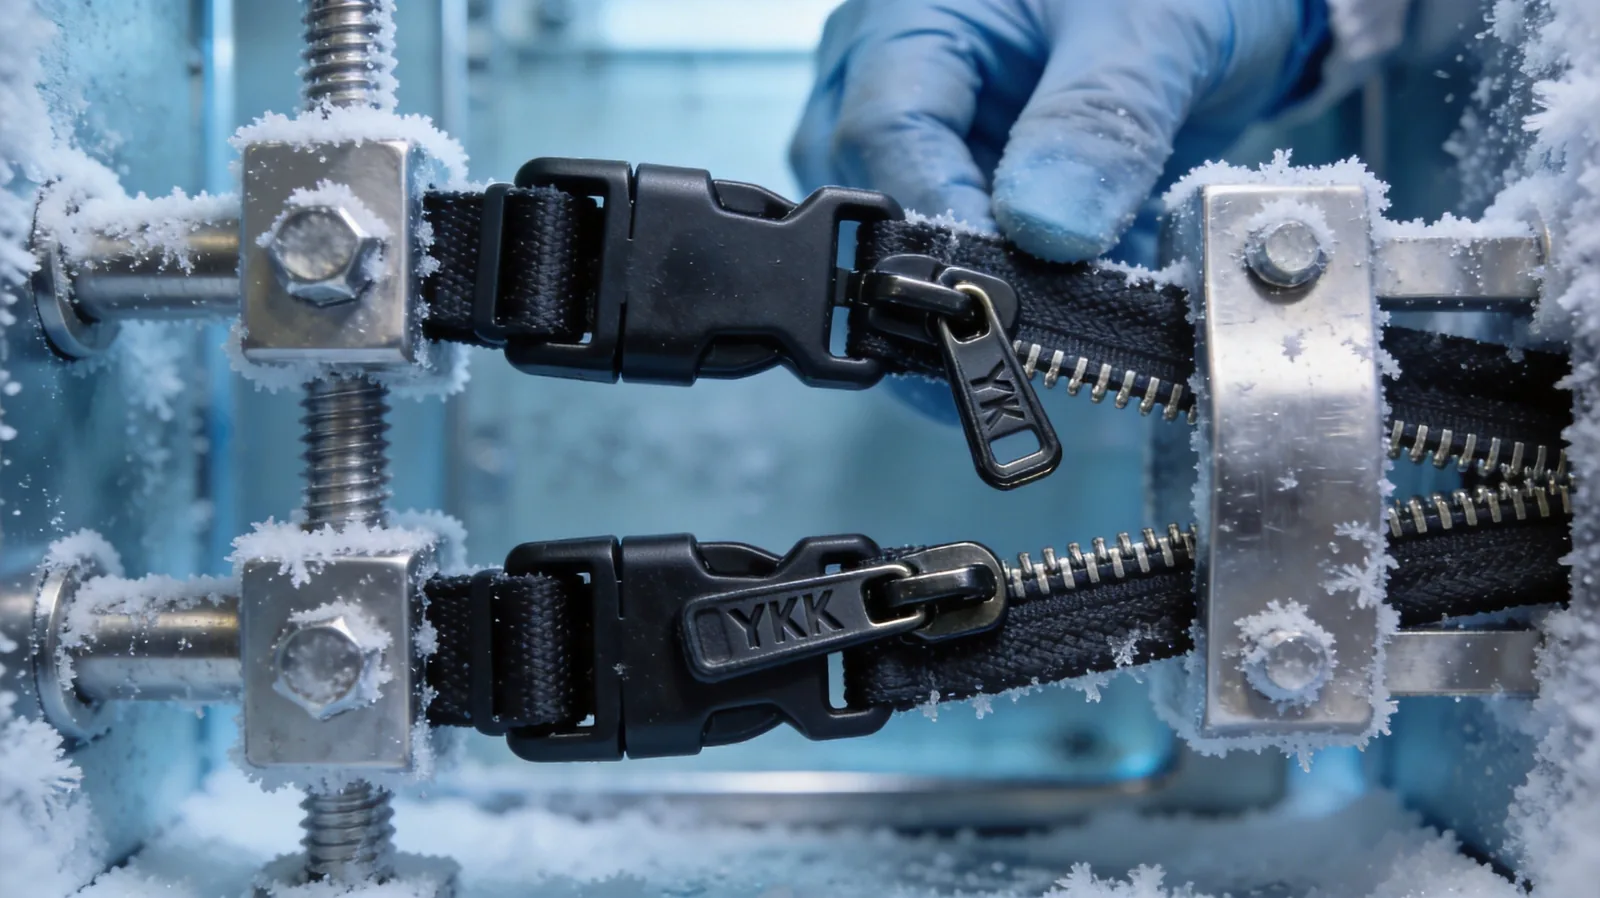
Hardware: the single most common failure point
Standard polypropylene buckles and cheap ABS hardware become brittle and crack below freezing. This is not an edge case or a quality-control outlier; it is the normal behaviour of the material. Polypropylene’s ductile-to-brittle transition sits close to 0 °C, so a PP side-release buckle that flexes happily in a warm warehouse will shatter on the first impact at −5 °C.
Acetal (POM) and impact-modified nylon retain flexibility and structural integrity down to roughly −40 °C. The cost difference at component level is small, typically cents per buckle, but the consequence difference is a customer complaint with photographs attached versus no complaint at all. For any pack sold into a market with a real winter, POM or impact-modified nylon is the specification floor, not an upgrade.
Coatings and laminates
PVC coatings lose flexibility at low temperature and split under repeated flex, which is why they should not be specified on a pack that will be folded and stuffed at −20 °C. TPU film laminates and two-pass PU coatings hold flexibility considerably better. Laminated constructions — a film or membrane bonded to a woven face — generally behave better in cold than a heavy knife-coated PU, because the coating layer is thinner and the flex stress is distributed differently.
The practical test is not a tensile test at room temperature. It is a cold-crack test on the finished laminate at the service temperature, which is why we specify coating performance by test method rather than by generic description.
Foams
EVA foam loses rebound resilience as temperature falls. At −20 °C a shoulder strap that feels supportive in the workshop feels noticeably firmer and transmits more pressure, because the foam is no longer absorbing energy the same way. This is why cold-climate packs often specify a softer base foam grade or a lower-density EVA than a warm-climate equivalent, and why a foam substitution to save cost can quietly destroy the comfort case in the target market.
Textiles and frame elements
Nylon and polyester lose some tensile strength at low temperature but remain entirely serviceable; the bigger issue is differential shrinkage between face fabric, coating, reinforcement panel and webbing, which concentrates stress at stitch lines. UHMWPE (Dyneema) performs exceptionally well in cold, retaining strength and flexibility, which is one reason it dominates the ultralight alpine segment. Aluminium frame stays are effectively immune to cold embrittlement — 6061-T6 and 7075 both behave well below −40 °C — so the frame is rarely the cold-weather problem; the hardware attached to it is.
| Component | Behaviour at −20 °C | Specify instead | Cost impact |
|---|---|---|---|
| PP buckle | Brittle, shatters on impact | POM (acetal) or impact-modified nylon | Low, cents per unit |
| Standard ABS hardware | Brittle, stress whitening at flex points | POM or glass-filled nylon | Low to moderate |
| PVC coating | Splits under repeated flex | TPU film or two-pass PU | Moderate |
| Standard EVA foam | Reduced rebound, firmer under load | Softer grade or lower density EVA | Neutral to low |
| Standard coil zip | Stiffens, hard to operate with gloves | YKK reverse coil, sized up | Low |
| Elastic cord | Loses tension, may not recover | Higher-grade elastomer or mechanical retention | Low |
| 6061-T6 / 7075 aluminium stay | No embrittlement, strength retained | No substitution needed | — |
| UHMWPE / Dyneema laminate | Strength and flexibility retained | No substitution needed | High but justified |
Cold-Temperature Testing Protocol
There is no single standard that says “a mountaineering backpack must pass at −20 °C”. What exists is a family of material-level test methods that can be applied to the components, plus our own finished-goods protocol built on top of them. Understanding the difference between the two is important, because a supplier can honestly claim to test to ASTM standards while never having tested a finished pack.
The applicable material test methods
ASTM D746 — Standard Test Method for Brittleness Temperature of Plastics and Elastomers by Impact. This determines the temperature at which 50% of specimens exhibit brittle failure under specified impact conditions, by cooling specimens in a bath, striking them at a specified linear speed and examining the result. The current edition is ASTM D746-24, which revised D746-20. It is technically equivalent to ISO 974 when using the Type B fixture and Type III specimen, though the ISO method requires a minimum of 100 specimens (ASTM International).
Related methods matter because they apply to different component types: ASTM D1790 covers brittleness temperature of plastic sheeting by impact, which is the right method for a coating film, while ASTM D2137 covers rubber impact brittleness. Using D746 on a coating film is a category error that produces a meaningless number.
Our finished-goods cold protocol
Material test data tells you what the raw component does. It does not tell you what happens when that component is assembled into a pack, stitched under tension and then frozen. So we run a finished-goods protocol on hardware and attachment assemblies, structured to reproduce the actual service condition rather than a laboratory abstraction.
| Step | Condition | Duration | Pass criteria |
|---|---|---|---|
| 1. Wet-out | Submerge assembly in water (simulates wet snow and meltwater) | 4 hours | — |
| 2. Deep freeze | Transfer immediately to −20 °C chamber | 24 hours | — |
| 3. Impact | 10 kg weight dropped from 0.5 m onto the release mechanism | Immediate, still frozen | No fracture, no cracking |
| 4. Function cycling | Open and close mechanism 50 times while still frozen | Immediate | Full travel, positive engagement |
| 5. Visual inspection | Bend points examined under 10× magnification | — | No stress whitening, no micro-cracks |
| 6. Spring retention | Release and observe return | — | Snaps back to original shape immediately |
For coated fabrics and laminates we run a cold-fold test at the specified service temperature, folding the material 180° over a mandrel and inspecting for crazing, cracking or delamination, then re-testing hydrostatic resistance on the folded area. A coating that passes a flat hydrostatic test can fail on a fold, and folds are exactly what a pack does when it is stuffed in a cold tent.
What to ask your supplier for
Ask for a low-temperature impact test report on the specific buckle model and material you are specifying, not a generic tensile report and not a room-temperature function test. Ask which test method was used and at what temperature. If the answer is “we froze it and hit it with a hammer”, that is a workshop check, not a test report, and it will not protect you when a customer returns a pack with a shattered buckle.
Technical Suspension at 8–30 kg
The suspension brief for a mountaineering pack is not simply a heavier version of the trekking brief. Trekking packs optimise for continuous comfort over many hours at a roughly constant load. Mountaineering packs optimise for a load that changes radically during the day — full approach load at the trailhead, stripped to a summit pack at the col — and for a suspension that can be partly removed.
| Architecture | Construction | Load range | Weight penalty | Where it belongs |
|---|---|---|---|---|
| Frameless | Padded back panel only, no structural element | Up to 8 kg | None | Cragging, bouldering, fast-and-light alpine |
| Removable framesheet | HDPE or composite sheet in a sleeve, optionally one stay | 8–16 kg | 150–300 g | Alpine climbing, ski touring |
| Dual-stay frame | Two aluminium stays (6061-T6 or 7075) plus framesheet, anchored into hip belt | 15–30 kg | 400–700 g | Expedition |
The critical interface is where the frame meets the hip belt. On a trekking pack this is a permanent, heavily engineered junction. On an alpine pack it is often a removable connection, and that is where weight-saving decisions become structural: a hip belt that detaches with two side-release buckles transfers load through those buckles, so the buckle rating becomes a load-bearing specification rather than a convenience detail. This is precisely the point where a POM versus PP decision stops being about cold performance and becomes about whether the belt stays attached under a 20 kg dynamic load.
Shoulder strap design also diverges. Alpine packs typically use thinner, less padded straps because the pack spends part of its life compressed and light, and because a heavily padded strap is dead weight on a summit push. The trade is real: a 10 mm foam strap is comfortable at 8 kg and punishing at 20 kg. If you are building one pack to cover both cases, specify a medium-density 15 mm strap and accept that it is a compromise at both ends, or build two models.
Ultralight Construction: Where the Grams Actually Go
The ultralight alpine segment is where material selection becomes the product. A sub-800 g 40 L pack is not a lighter version of a 1,400 g pack; it is a different construction logic, and the weight has to come out in the right order.
| Material | Typical face weight | Abrasion | Water resistance | Relative cost | Best use |
|---|---|---|---|---|---|
| Dyneema Composite Fabric (DCF) | ~50–150 g/m² | Low to moderate | Effectively waterproof | Very high | Main body on sub-700 g packs |
| X-Pac VX21 | ~210 g/m² | Moderate | High | High | Main body, high-wear alpine |
| X-Pac VX42 | ~330 g/m² | High | High | High | Base panels, expedition bodies |
| Challenge Ultra 200 / 400 | ~120–240 g/m² | High for weight | High | High | Ultralight bodies requiring abrasion |
| ALUULA Graflyte | Very low | Moderate | High | Very high | Premium ultralight (used on Arc’teryx Alpha SL, 2025) |
| Coated ripstop nylon 70–210D | 70–210D | Scales with denier | Moderate (PU/TPU) | Low to moderate | Volume models, cost-controlled lines |
| Cordura 500D | ~500D | Very high | Low without coating | Moderate | Base panels, cragging packs |
The weight budget, line by line
A realistic 40 L alpine pack at 850 g breaks down roughly as follows. These proportions matter more than the absolute numbers, because they tell you where a cost-driven substitution will hurt.
| Element | Share of weight | What drives it | Where weight can safely come out |
|---|---|---|---|
| Face fabric and coating | 35–45% | Denier and laminate choice | Main body only — never the base or strap roots |
| Hardware (buckles, hooks, cord locks) | 15–20% | Number of components more than material | Component count reduction, not material downgrade |
| Webbing and straps | 10–15% | Width and count | Narrower webbing where loads are light |
| Foam (straps, back panel, belt) | 10–15% | Thickness and density | Back panel first, shoulder straps last |
| Frame element | 5–10% | Stays versus framesheet | Removable design rather than lighter material |
| Stitching, seam tape, reinforcements | 5–10% | Anchor count | Not safely reducible — this is where strength lives |
The single most effective weight reduction is component count. Removing four cord locks, two compression strap buckles and one lid buckle typically saves more than switching the face fabric from 210D to 100D, and it does so without touching the abrasion margin. The single most dangerous weight reduction is thinning the reinforcement under load-bearing anchors, which is invisible in the finished product and shows up as a field failure six months later.
The 2026 correction: away from “stupid light”
The market has moved. Sourcing analysis for 2026 shows a retreat from frameless ultra-minimalism: for loads above roughly 9 kg, buyers are showing a clear preference for minimal frame support over raw weight savings. The same analysis shows a shift toward targeted reinforcement — high-tenacity materials at high-stress points such as hip belts and shoulder strap roots, with the main body kept light — and toward modularity, with lidless and roll-top designs where frame, lid or hip belt can be removed to strip the pack down for lighter missions.
That is a useful correction for anyone planning a 2026 line. The sub-700 g frameless pack still sells, but it sells as a specialist item. The volume is in the 850–1,200 g pack with a removable frame and targeted reinforcement, which is a more demanding product to manufacture because it has to be light and structurally honest at the same time.
The UIAA Myth: Mountaineering Packs Have No Certification Standard
This is the point where a lot of sourcing conversations go wrong, so it is worth being precise.
The UIAA, the International Climbing and Mountaineering Federation, has published safety standards since 1960, when it began with rope testing. It now maintains standards for more than twenty categories of mountaineering equipment and collaborates with CEN on harmonisation, in some cases requiring additional tests that make the UIAA standard stricter than the equivalent EN standard (UIAA).
The published list covers ropes, accessory cord, tape, slings, harnesses, helmets, low-stretch ropes, belay lanyards, connectors and karabiners, pitons, rock anchors, chocks, frictional anchors, rope clamps, pulleys, energy absorbing systems, braking devices, load sharing devices, ice anchors, ice tools, crampons, snow anchors, snow pickets, avalanche rescue shovels, avalanche probes and crash pads.
There is no UIAA standard for backpacks. There never has been. The pack is not on the list, and it is not on the list for a defensible reason: a backpack is a carrying system, not a piece of protective or load-bearing safety equipment in the way a harness or a karabiner is. Its failure modes are functional and commercial rather than life-safety in the sense the UIAA standards address.
| Standard | Covers | Applies to a backpack? |
|---|---|---|
| UIAA 101 | Dynamic ropes | No |
| UIAA 105 | Harnesses | No |
| UIAA 106 | Helmets for mountaineers | No — applies to the helmet you carry in it |
| UIAA 152 | Ice tools | No — applies to the axe you attach to it |
| UIAA 153 | Crampons | No — applies to the crampons in the pouch |
| UIAA 156 / 157 | Avalanche rescue shovels / probes | No — applies to the tools in the sleeve |
| UIAA 161 | Crash pads | No |
| EN 16716 | Avalanche airbag systems | Yes, when the pack integrates an airbag system |
| Regulation (EU) 2016/425 | Personal protective equipment | Yes, for airbag packs specifically |
To be concrete about how the UIAA standards do work, take UIAA 106 for helmets. Version 4.0 was published in September 2025 and became effective in January 2026. It is based on EN 12492:2025, and it imposes an additional requirement over the EN standard: the force transmitted to the head form must not exceed 8 kN, where EN 12492 permits up to 10 kN. Certification requires a test report from a UIAA-approved laboratory. That is what a real certification regime looks like — and it applies to the helmet, not to the pack that carries it.
Avalanche Airbag Packs: The One Case Where Your Pack Becomes PPE
There is exactly one exception to everything above, and it is commercially significant because airbag-compatible packs command premium pricing and are increasingly expected in the ski touring segment.
In the European Union, an avalanche airbag pack is regulated as personal protective equipment. EN 16716 — “Mountaineering equipment — Avalanche airbag systems — Safety requirements and test methods” — was published in 2017 and is cited in the Commission communication implementing Regulation (EU) 2016/425 on personal protective equipment. A revision, prEN 16716:2025, is in progress; the German draft DIN EN 16716:2025-02 runs to 72 pages, which gives some indication of how detailed the requirements are.
The technical content is specific and demanding. The standard does not address personal protection against impact or cold temperature — it is about the airbag system’s ability to prevent burial. Key requirements include the following.
| Parameter | EN 16716 requirement |
|---|---|
| Mechanical activation force | 50 N to 150 N |
| Maximum activation travel (mechanical) | 100 mm |
| Inflation time | Full inflation within 5 s of activation |
| Inflation retention | Remains inflated for at least 3 minutes |
| Minimum airbag volume | 150 litres fully inflated |
| Rated deployments | Declared rating of at least 20; tested to twice the rating |
| Pressure tolerance | Operating pressure +0.1 bar for 30 min without damage; +0.25 bar without bursting |
| Airbag fabric tensile strength | Referenced to EN ISO 13934-1 |
| Cold performance | Must activate and inflate after at least 24 h at −30 °C without external support |
| Operating temperature range | Manufacturer-declared range, or −30 °C to +50 °C, whichever is wider |
| Electrical systems | Low-battery indication required; deployable for at least 6 h after indication |
| Airbag impact test | 10 kg cylindrical steel weight, 120 mm diameter, 1 mm edge radius, dropped vertically from 2 m onto the inflated centre |
| Carrying system strength | Pack mounted on test torso per EN 12277, shoulder strap loosened against load direction, 3 kN applied for 1 min |
Because the pack is PPE, the manufacturer’s obligations extend well beyond product performance. Under Regulation (EU) 2016/425, the manufacturer must ensure design and manufacture conform to the regulation, subject each item to the relevant conformity assessment procedure, keep technical documentation and the EU declaration of conformity for ten years, carry out sample testing, maintain a register of complaints and non-conforming items, and provide registered trade name and postal address on packaging or accompanying documents.
For a real-world illustration of the full path: Decathlon’s WEDZE AIRBAG 30 is certified by TÜV Süd and declared as complying with both EN 16716:2017 and Regulation (EU) 2016/425 on personal protective equipment, with a declared operating range of −30 °C to +50 °C and a 150 litre airbag volume. That is what a compliant airbag pack looks like on paper.
Climbing Packs: Cragging, Sport, Trad and Bouldering
Climbing and mountaineering overlap heavily in search behaviour and in customer mind, but they are not the same product brief, and conflating them produces a pack that does neither job well. Climbing packs optimise for rock, abrasion and gear access. Mountaineering packs optimise for cold, altitude and tool carry. If your line needs to cover both, it needs two specifications, not one compromise.
| Sub-type | Capacity | Primary requirement | Key features | Cold rating needed |
|---|---|---|---|---|
| Cragging pack | 20–40 L | Abrasion resistance on rock and at the base | 500D–1000D base, wide mouth, rope strap, tarp integration | Moderate |
| Sport climbing pack | 25–35 L | Rack and rope organisation, quick access | Drawstring closure, rope tarp, gear loops, minimal frame | Low |
| Trad climbing pack | 30–45 L | Load carry with rack weight, gear accessibility | Framesheet, gear loops, helmet carry, tool loops | Moderate |
| Bouldering bag | 25–45 L plus pad | Pad integration, ground protection | Removable pad, tarp base, brush pocket, closure flap | Low |
The specific engineering difference that matters most in production is abrasion specification. A cragging pack spends its life being set down on granite, dragged through chimneys and loaded onto sandy ground, so base and lower side panels go to 500D–1000D with bound seams and often a double-layer base wrap. A mountaineering pack of the same capacity uses a 100–210D laminated body because it is optimised for weight, and would be destroyed by the same treatment. This is why the two product families should not share a pattern.
Gear loop construction is the other divergence. Climbing packs need a rack of gear loops that will accept repeated clipping and unclipping with metal hardware, which abrades webbing edges quickly. We specify bar-tacked webbing loops rather than stitched-through fabric loops, because the fabric version abrades through at the loop edge within a season of regular use. For background on how the climbing pack category has evolved and what the reference products look like, see our earlier breakdown of technical climbing backpacks, and for the plain-language category distinction see backpack versus mountaineering bag.
Hardware and Component Specification
Hardware specification is where cost pressure most often translates directly into field failure, because the savings are visible on the bill of materials and the failure is not visible until winter. The table below is the specification baseline we use for technical packs.
| Component | Specification baseline | Cold requirement | Cost note |
|---|---|---|---|
| Side-release buckles | POM (acetal) or impact-modified nylon | Function and impact resistance to −20 °C minimum | Cents more than PP; not a real cost driver |
| Hip belt connection | Load-rated POM buckle or metal hook | Must hold rated load frozen | Moderate; this is a structural part, not trim |
| Main zipper | YKK #8 reverse coil, or #10 on expedition | Operable with gloves at −15 °C | Low; reverse coil is the correct default |
| Water-resistant zipper | YKK AquaGuard or equivalent where specified | Operability degrades in cold; test before specifying | Moderate |
| Cord locks | POM body, stainless spring | No cracking; spring retains tension frozen | Low; count matters more than unit cost |
| Webbing | Nylon or UHMWPE (Dyneema) for load paths | Strength retained; UHMWPE preferred where weight-critical | UHMWPE is high; use only on real load paths |
| Frame stays | 6061-T6 (general) or 7075 (high strength) | No cold embrittlement | Moderate |
| Framesheet | HDPE sheet, 1.0–2.0 mm depending on load class | Retains stiffness | Low |
| Foam | EVA, closed cell; density graded by location | Cold-flex grade on shoulder straps | Low; grade substitution is a false economy |
| Elastic cord | Higher-grade elastomer, UV stabilised | Recovers tension at −20 °C | Low |
Two specification rules are worth stating explicitly because they are routinely violated in cost-down exercises. First, never downgrade hardware on a load path. The difference between a POM and a PP buckle is cents; the difference in outcome is a warranty claim in a market you cannot easily service. Second, never substitute foam grade without re-testing the cold comfort case, because a foam substitution that looks like a 2% cost saving can change how the pack feels at −15 °C more than any other single change.
For broader material selection logic across waterproof and coated constructions, see our guide to waterproof bag material selection.
Manufacturing: Stitch, Seam, Seal and Bar-Tack
Technical packs are a stitching-intensive product, and the manufacturing discipline required is different from volume bag production. The sewing operations that matter are the ones under load, and they are the ones most likely to be rushed in a factory optimising for pieces per hour.
Stitch specification
Load-bearing seams are sewn with a minimum stitch density of 8–10 stitches per inch, using bonded nylon or polyester thread sized to the fabric weight. Bar-tacks at attachment anchors run eight stitches per 30 mm. Stitch type matters: a lock stitch is standard for structural seams, while chain stitch is faster but has no failure containment, so it should not be used anywhere the seam carries load.
Seam strength testing
We verify seam performance against recognised methods rather than visual inspection. Grab tensile strength is measured to ASTM D5034, which is the standard test for breaking strength of textile fabrics, and tear strength to ASTM D2261 (trapezoid procedure). Both are run on seamed assemblies, not just on flat goods, because a seam is where the failure will actually occur. A 500 N seam on a load-bearing anchor is a defect regardless of what the face fabric is rated at.
Waterproofing and seam sealing
On laminated and coated constructions, the waterproofness of the finished pack depends more on the seams than on the fabric. Critical seams — main body side seams, base seams, and any seam below the waterline — are seam-taped or sealed. Welded construction is used where the pattern allows it and the volume justifies the tooling; on lower-volume technical packs, taped seams are usually the more economical route to the same performance. We test hydrostatic resistance on finished seams rather than on flat goods, because that is the number the customer experiences.
Reinforcement logic
Reinforcement is placed where the load path terminates: attachment anchors, strap roots, base corners, and the frame-to-hip-belt junction. On lightweight face fabrics, reinforcement is laminated or bonded rather than merely stitched, because a stitched patch in a 70–100D fabric concentrates stress at the stitch holes. On heavier fabrics, stitched reinforcement is acceptable and more economical.
| Operation | Specification | Verification |
|---|---|---|
| Structural seams | Lock stitch, 8–10 SPI, bonded nylon thread | Grab tensile ASTM D5034; visual 100% |
| Attachment bar-tacks | 8 stitches per 30 mm, reinforced substrate | Pull test 200–400 N / 1 min on sampled basis |
| Strap roots | Box-X stitch plus bar-tack | Pull test; visual 100% |
| Base seams | Bound or taped, double-stitched | Hydrostatic on finished seam |
| Critical waterproof seams | Seam tape or weld | Hydrostatic; water spray test |
| Tear resistance | Per material specification | ASTM D2261 trapezoid |
QC Protocol for Technical Packs
Quality control on a technical pack has to be structured around the failure modes that matter, not around a generic cosmetic checklist. A pack with a perfect stitch line and a PP buckle is a defective product.
| Stage | What is checked | Method | Acceptance |
|---|---|---|---|
| Incoming material | Face fabric weight and coating, hardware material certificate, webbing tensile, foam density | Supplier certificate plus in-house verification | Per specification; hardware material must be confirmed, not assumed |
| Incoming hardware | Cold impact on sampled lots | −20 °C / 24 h then impact and function cycle | Zero fracture, zero micro-cracks |
| In-process | Bar-tack placement and density, seam allowance, reinforcement presence at anchors | Visual and measurement at each station | 100% at anchor stations |
| Attachment pull test | Every load-bearing anchor type | 200–400 N held 1 min | No stitch deformation, no fabric distortion |
| Airbag-compatible carrying system | Harness strength where applicable | 3 kN / 1 min on test torso per EN 12277 arrangement | No failure, no elongation beyond spec |
| Finished goods | Hardware function, zipper operation, strap adjustment, cosmetic | 100% functional check | AQL 2.5 major / 4.0 minor, critical 0 |
| Cold functional (sampled) | Buckle release and closure, zipper operation, with gloves | −15 °C chamber, gloved operation | Full function without excessive force |
The one non-negotiable item in that table is the hardware material confirmation at incoming inspection. A factory that accepts a hardware shipment on the supplier’s word, without confirming the polymer, has no control over the single most common cold-weather failure mode in the category. We require material certification on buckles and cord locks, and we verify by cold impact on sampled lots.
OEM/ODM Programme: MOQ, Sampling and Lead Time
For a technical pack line, the commercial terms are the same as our broader programme, but the sampling stage is longer in practice because there are more specification decisions to close.
| Parameter | Terms |
|---|---|
| MOQ | 500 pcs per colour per design |
| Sampling time | 6–10 days from approved specification |
| Bulk production | 35–50 days from sample approval |
| Sample fee | Charged, refunded against the bulk order |
| Customisation | Full OEM (your pattern and specification) or ODM (our existing platform with your branding and specification changes) |
What to bring to the first technical discussion
Technical pack development moves fastest when the brief is specific. The five items that most affect quotation and timeline are: the archetype and capacity range, the carried load the pack must support, the minimum service temperature for hardware and coatings, the attachment interfaces required, and the target weight ceiling. With those five settled, the specification, bill of materials and testing scope can be fixed in one round rather than three.
If you are still deciding between OEM and ODM structure, our comparison of OEM versus ODM and private label sets out the trade-offs, and the sample to bulk production process covers what happens between approved sample and shipped order. For landed cost planning, including how Incoterms change the number, see FOB versus EXW versus DDP.
Frequently Asked Questions
Is there a UIAA or EN certification required for mountaineering backpacks?
No. There is no UIAA standard for backpacks and no EN product standard that a general mountaineering pack must meet. The UIAA maintains standards for more than twenty categories of climbing and mountaineering equipment — ropes, harnesses, helmets, karabiners, ice tools, crampons, avalanche rescue tools and others — but the backpack itself is not among them. What applies to your pack is general product safety law, chemical compliance such as REACH, and national EPR registration for the markets you sell into. The single exception is the avalanche airbag pack, which is covered below.
Do avalanche airbag packs need CE marking and PPE certification?
Yes. In the European Union an avalanche airbag pack is regulated as personal protective equipment under Regulation (EU) 2016/425, and EN 16716 is the harmonised product standard cited under that regulation. That means a conformity assessment procedure, an EU declaration of conformity, technical documentation retained for ten years, sample testing, and a complaints register. The airbag system itself is typically a third-party certified module, so integration and system certification are separate workstreams. An ordinary mountaineering pack without an airbag has no equivalent certification path.
What temperature should mountaineering pack hardware be rated to?
Specify −20 °C as the minimum for hardware function and impact resistance on any pack sold into a market with a real winter, and −30 °C for airbag-compatible and high-altitude models. This is achievable with standard POM (acetal) or impact-modified nylon hardware. The failure you are avoiding is specific: polypropylene and cheap ABS buckles become brittle below freezing and can shatter on impact. The cost difference between PP and POM at component level is cents, so there is no commercial argument for the downgrade.
How do you test ice axe and crampon attachment points?
Every load-bearing attachment type is pull-tested at 200–400 N held for one minute, with acceptance requiring no stitch deformation, no fabric distortion and no movement of the anchor. On airbag-compatible models the carrying system is tested to the EN 16716 arrangement: pack mounted on a test torso per EN 12277, shoulder straps loosened against the load direction, 3 kN applied for one minute. Hardware on those anchors is also function-cycled at the specified cold temperature, because a hook that works at 20 °C can be unusable at −15 °C with gloves on.
Can you produce sub-800 g alpine climbing packs?
Yes, in the 28–45 L alpine range using laminated UHMWPE constructions such as Dyneema Composite Fabric, X-Pac or Challenge Ultra, with a removable framesheet and reduced component count. Two things need to be agreed up front: the minimum service temperature, because very light hardware and thin coatings have less margin, and the reinforcement strategy at load-bearing anchors, because a bar-tack in 70D fabric will tear out regardless of stitch count. We would also flag that the 2026 market has moved away from frameless ultra-minimalism above roughly 9 kg of carried load, so the volume opportunity is in the 850–1,200 g band with targeted reinforcement rather than in the sub-700 g band.
Which fabrics do you recommend for expedition packs?
For 65–110 L expedition packs carrying 20–30 kg, we generally specify a 210–420D laminated or coated nylon for the body with a 500D–1000D base panel, rather than pushing ultralight laminates. The reasoning is that expedition packs are dragged, sled-hauled and set down on rock and ice, and the abrasion and puncture margin matters more than 200 g of weight. X-Pac VX42 and comparable heavy laminates are a good middle path where waterproofness and abrasion both matter. Ultralight laminates belong on the alpine climbing and fast-and-light models, not on the expedition flagship.
What is the difference between a mountaineering pack and a climbing pack?
Climbing packs optimise for rock: abrasion resistance on granite and sandstone, gear loop racks that survive repeated clipping with metal hardware, rope organisation, and bouldering pad integration. Mountaineering packs optimise for cold and altitude: ice axe and crampon attachment systems, ski carry load paths, cold-rated hardware, and strippable modular construction for summit pushes. There is overlap in the 30–45 L range, but the two briefs pull in different directions, and a single pattern that tries to serve both usually does neither well.
What is the MOQ for custom mountaineering backpacks?
500 pieces per colour per design. Technical packs are a low-volume, high-variation category, so a programme typically runs several capacity variants and colourways; the MOQ applies per colour per design rather than to the whole programme. Sampling takes 6–10 days from an approved specification, bulk production 35–50 days from sample approval, and the sample fee is refunded against the bulk order.
Can you build a pack that is compatible with a third-party airbag system?
Yes, as a pack. Integration with a specific airbag module — Alpride, ABS and similar — has to be designed against that module’s mounting and routing requirements, and the module’s own certification remains with the module manufacturer. What changes on our side is the carrying system, which must be built to the EN 16716 test arrangement, and the documentation, which has to support your conformity assessment if you intend to sell the combined product as PPE in the EU. We would scope that as a separate programme rather than as a variant of a standard technical pack.
What lead time should I plan for a technical pack programme?
Allow 6–10 days for sampling once the specification is fixed, 35–50 days for bulk production after sample approval, and additional time for any cold-impact or seam-strength testing you require as part of approval. The part that most often extends a first programme is not production but specification: settling the archetype, load case, minimum service temperature and attachment interfaces. Bringing those five decisions to the first technical discussion typically removes one full sampling round.
Start Your Mountaineering Pack Programme
Build a Technical Alpine Range With JUNYUAN
We manufacture custom mountaineering and climbing backpacks from 28 L alpine strippable packs to 110 L expedition models, in coated nylon, X-Pac and laminated UHMWPE constructions, with engineered attachment systems, POM hardware rated to −20 °C, documented cold-impact and pull-test protocols, and full technical documentation for your compliance file. MOQ 500 pcs per colour per design, sampling 6–10 days, bulk production 35–50 days, sample fee refunded against the order.
Talk to our technical team about your alpine pack specification →
If your line spans categories, the outdoor backpack manufacturer matrix explains how hiking, trekking, mountaineering and camping packs differ on one factory platform, and the hiking backpack OEM blueprint and trekking backpack manufacturing guide cover the adjacent briefs in detail. For a wider view of the supplier landscape, see our review of custom backpack manufacturers in China.