Short answer: a custom golf travel cover programme at Junyuan Bags runs at MOQ 500 pieces per style, samples in 6–10 working days, bulk in 35–50 days, inspected to AQL 2.5 major / 4.0 minor. We are a bag manufacturer established in 2014, with our founder in the golf and bag trade since 2004. A travel cover is the one golf product where the specification is set by the airline rather than the player: a 130×36×36 cm cover measures 202 cm linear, which is 44 cm over the 158 cm standard checked-piece template most network carriers publish. Everything else follows from that number — the moulded hard top that takes the club-head impact, the 3,090 g weight budget, the 75 mm wheels that carry 76 N per wheel when the bag is loaded, and the 0.135 CBM carton that decides whether your landed cost is USD 38.50 or USD 45.00. This page is the procurement document for the brand owner or sourcing manager placing that order. For the bags that go inside it, start on our custom golf staff bag page or the custom golf cart bag page; for the airline rules themselves, read can you take a golf bag on a plane.
Where the money actually goes. Take a mid-market soft cover with a moulded EVA hard top, 1680D ballistic shell and 75 mm wheels at USD 38.50 FOB. Fabric and foam are 17% of that. The moulded hood is 11%, the frame and skid base 7%, and wheels, housings and trolley are 14% — the largest hardware block in any golf bag we build, because the wheel assembly is what fails first in airline baggage handling. Zippers and hardware 8%, pockets and webbing 6%, decoration 4%, overheads and packing 10%, factory margin 4%, and labour 19%. Add wheels to labour and 33% of the price sits in the two areas the buyer never inspects until the first claim. There is a second number most factories will not put on the table: at 0.135 CBM per carton a 40HQ holds 503 covers, so ocean freight alone is USD 5.17 per piece at USD 2,600 per 40HQ — 13.4% of FOB, before duty. A cover that is 3 cm wider in every direction costs you more in freight than a 5% fabric downgrade saves.
What a Golf Travel Cover Is — and the Five Products It Gets Confused With
A golf travel cover is a transport shell for a full set: 130–135 cm long, 34–40 cm in section, with a padded or moulded club-head compartment at the top, a stiffened spine along the shaft line, two wheels at the base and a telescopic handle. It is not a bag you play out of. It exists for the six to ten hours a year when a USD 2,500 set of clubs is inside an aircraft hold at −50 °C and 0.8 bar, being thrown by people who are paid per tonne.
That single sentence sets the design brief, and it is why a travel cover is specified differently from every other product in a golf line. The player never sees it on the course, so brand visibility has to be bought with a large flat panel and a clean logo lock-up. The caddie never carries it, so strap ergonomics do not matter. The airline does the handling, so the failure modes are impact at the club head, crushing in the stack, wheel and handle breakage, and water ingress on the apron. A cover that survives all four at 3 kg beats a cover that survives three at 2.4 kg, because the fourth one generates the warranty claim.
Five products get called “golf travel cover” in a purchase order, and each one has a different pattern, a different tooling bill and a different price. Settle the name before the PO:
- Soft travel cover. Padded 1680D or 600D shell over 10 mm EPE foam, HDPE spine board, soft padded top. 2,400–2,900 g. Folds roughly flat for retail and for owner storage. This is the volume product and the one most private-label programmes start with.
- Soft cover with moulded hard top (the workhorse). Same body, but the top 30–35 cm is a moulded EVA hood with a 5 mm wall and a reinforced rim. 2,900–3,400 g. The hood absorbs the club-head impact that destroys soft tops, at roughly USD 4.24 of BOM and one mould. About 60% of the covers we ship are this architecture.
- Full hard case. Moulded ABS or polycarbonate clamshell, 2.0–2.8 mm wall, hinge, two or three latches, sometimes a TSA-style lock. 4,200–5,600 g. Highest protection, highest freight, and a completely different tooling conversation — a clamshell mould is USD 3,800–7,500 on its own, so it only makes sense above 1,000 pieces.
- Wheeled golf bag / cart bag with a hood. Not a cover. It is a playing bag with a removable rain hood, sold as “travel-ready”. If your reference sample is one of these, you are buying from our cart bag line, not this one.
- Staff / tour bag cover. A cover sized for a 9.5–10.5 inch staff bag rather than a cart bag: 38–40 cm section instead of 34–36 cm, and a taller hood. Same pattern family, 8–12% more fabric and 0.02 CBM more freight per piece. If your range includes a staff bag, specify the cover to match it or the staff bag will not fit.
One more distinction that saves money: a travel cover is not a flight bag for rental clubs. Rental and tour-operator fleets need a lighter, cheaper cover with a soft top because the clubs inside are not the customer’s and the cover is replaced every two seasons. We quote those at a lower BOM with a 600D shell and no moulded hood, and they are usually ordered in the same 500-piece run as the retail version so the pattern cost is shared.
Airline Reality: The Cover Is a Dimensional Product Before It Is a Bag
Most network carriers publish 158 cm (62 in) linear as the standard checked-piece size, and most accept a golf bag as one checked piece. A golf travel cover cannot meet that limit — the clubs are 115–125 cm long before you put anything around them. So the product is, in practice, an oversize item by definition, and the design job is to stay inside the smallest oversize band your customers fly on rather than to chase a limit you cannot reach.
| Build | Dimensions (cm) | Linear (cm) | Linear (in) | Over 158 cm by | Practical consequence |
|---|---|---|---|---|---|
| Compact soft cover | 125 × 34 × 34 | 193 | 76.0 | 35 cm | Fits the tightest oversize band; tight for 10.5 in staff bags |
| Standard soft cover + hard top | 130 × 36 × 36 | 202 | 79.5 | 44 cm | Our default; takes a cart bag plus shoes and a rain suit |
| Staff-size cover | 132 × 38 × 38 | 208 | 81.9 | 50 cm | Required for 10.5 in staff bags; check carrier templates |
| Full hard case | 134 × 40 × 40 | 214 | 84.3 | 56 cm | Highest protection, highest oversize exposure |
The dimensional table is not a technicality. Two of the four numbers above decide three commercial outcomes: which fee band the customer pays, how many pieces fit a 40HQ, and whether the cover fits the boot of a normal car. A 4 cm reduction in section sounds like a design nicety; on a 130 cm length it removes 0.03 CBM from the carton, which is 40 more pieces per 40HQ, which is USD 0.40 per piece of freight. Multiply that by 5,000 pieces and it pays for the hood mould.
Two practical rules we build to, and both are worth writing into your own spec sheet:
- Design to the smallest carrier you care about, not the largest. Published limits, weight allowances and oversize fees differ by carrier, route and fare class, and they change. We do not quote airline policy as a guarantee; we quote a cover that measures 202 cm linear and weighs 3.1 kg empty so that a 14-club set plus shoes lands around 15.5 kg — comfortably inside a 23 kg allowance with room for a rain suit. Your customer then pays the oversize fee their own ticket specifies, not a second fee for weight.
- Put the loaded weight on the spec sheet, not the empty weight. A cover is judged at 15.5 kg. Every handle, wheel housing and base rail on this page is specified against that number, and the static pull test is 500 N — 51 kg, more than three times the loaded weight — because a handler lifts the trolley handle, not the bag.
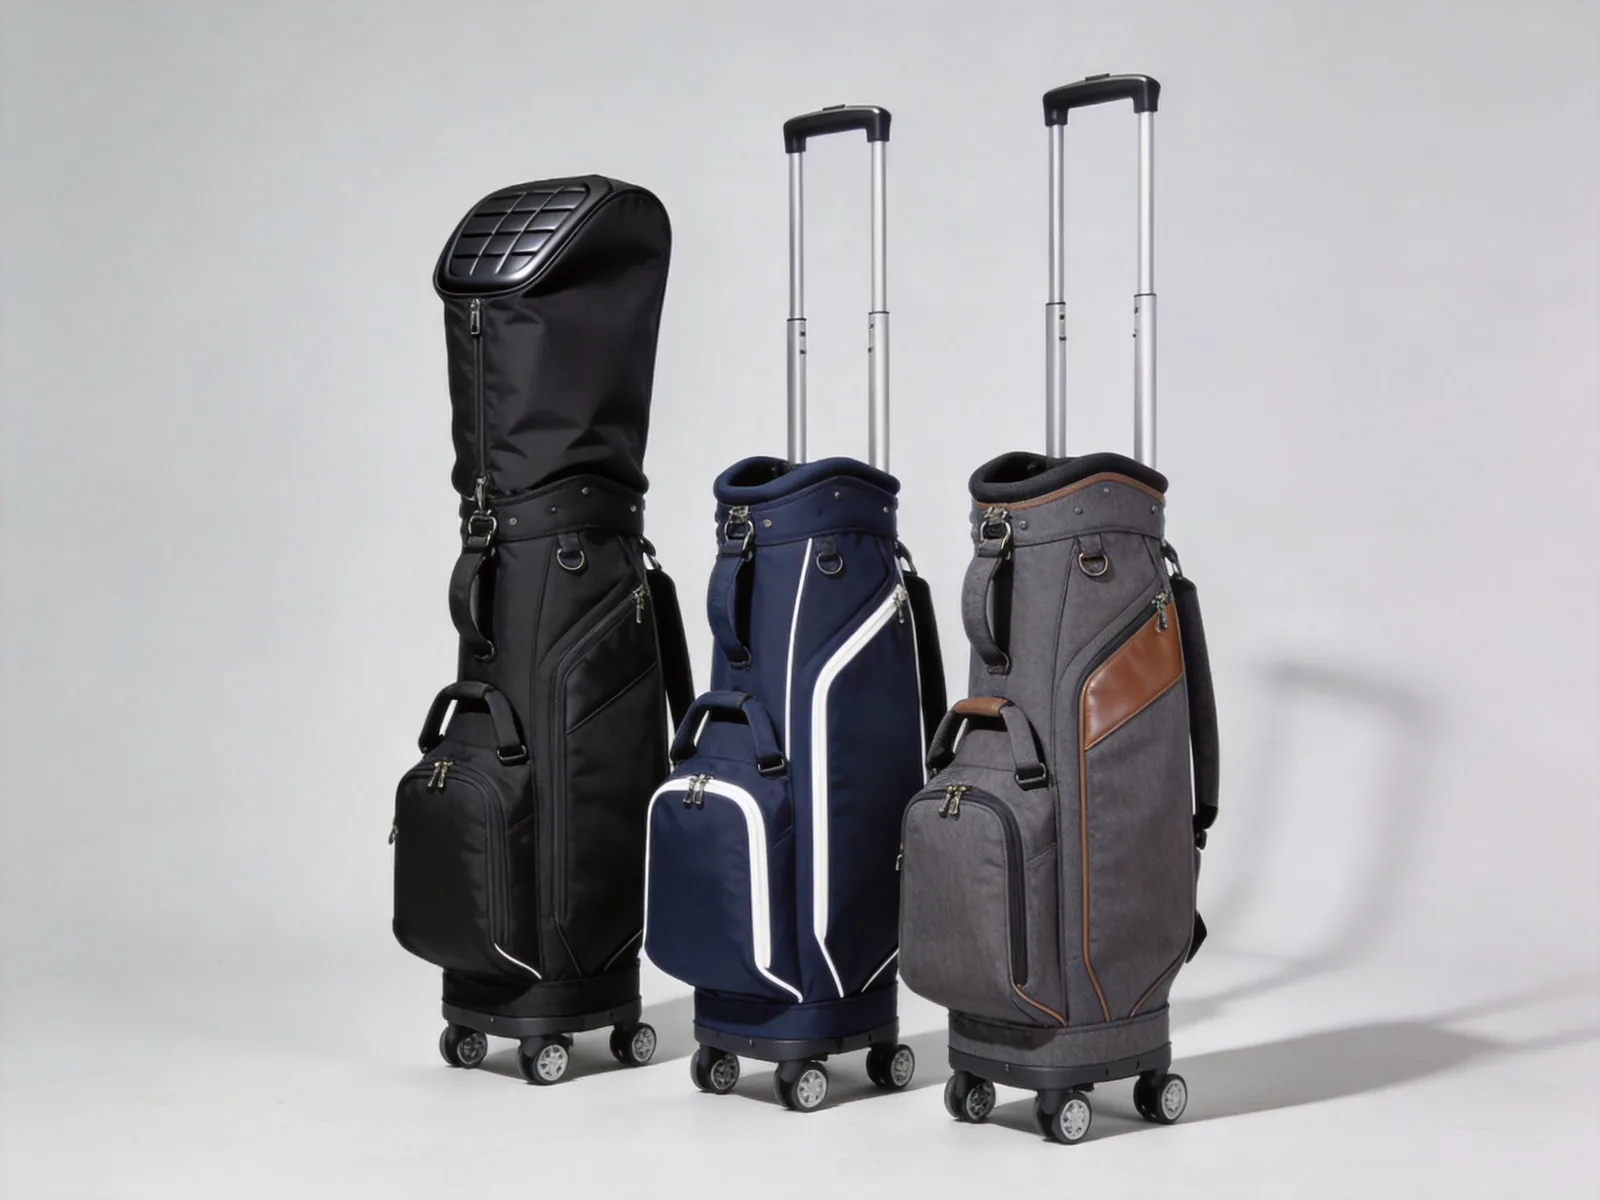
Three builds from one pattern family: black 1680D ballistic with a moulded EVA hard top, navy with white piping, and charcoal with a PU leather panel. Same 130 × 36 × 36 cm envelope, three BOM levels.
Three Architectures, Thirteen Decision Metrics
Before a price, a buyer needs an architecture. The table below compares the three builds we actually produce, on the metrics that show up in a claim file rather than in a catalogue. Read it as a specification menu: any row can be moved, and moving it moves the price by the amount in the last column.
| # | Decision metric | Soft cover | Soft + moulded hard top | Full hard case | Cost effect vs soft |
|---|---|---|---|---|---|
| 1 | Empty weight | 2,400–2,900 g | 2,900–3,400 g | 4,200–5,600 g | +0 / +USD 4–6 |
| 2 | Club-head protection | 10 mm foam + padded top | 5 mm EVA hood + egg-crate lid | Rigid shell + internal cradle | +USD 4.24 / +USD 14–22 |
| 3 | Crush resistance (static, packed) | ~120 kg before permanent set | ~250 kg | ~600 kg | included above |
| 4 | Tooling | pattern only: USD 350–600 | + hood mould USD 2,200–3,800 | + clamshell mould USD 3,800–7,500 | one-off |
| 5 | Carton cube per piece | 0.118 CBM | 0.135 CBM | 0.162 CBM | +USD 0.66 freight/pc |
| 6 | 40HQ loading | 576 pcs | 503 pcs | 419 pcs | — |
| 7 | Fold-flat for retail / storage | Yes, ~1/3 volume | Body folds, hood does not | No | affects retail packing |
| 8 | Wheel set | 60 mm PU, fixed | 75 mm PU, replaceable housing | 75–90 mm, bolt-on | +USD 1.60–2.80 |
| 9 | Water resistance | PU back coating, 3,000 mm | TPU laminate, 5,000 mm | Sealed shell + gasket | +USD 0.90–1.70 |
| 10 | Decoration area | Full front panel, print | Front panel + hood badge | Front panel + moulded logo insert | mould insert USD 320–600 |
| 11 | MOQ at a workable price | 500 | 500 | 1,000 (mould amortisation) | — |
| 12 | Typical channel | Promotional, rental fleets, entry retail | Golf retail, DTC, private label | Premium travel, tour operators | — |
| 13 | First failure in the field | Top seam and club-head wear | Wheel housing and zipper slider | Latch and hinge | — |
The honest recommendation, if you are building a range for the first time: start with the middle column at 500 pieces. It carries the protection story you can put in a product video (drop the cover, open it, clubs are fine), it does not require a clamshell mould, and its carton still loads 503 pieces into a 40HQ. Then add the full hard case as a premium SKU once you have a channel that sells above USD 120 retail, because a hard case only earns its tooling at four-figure volumes.
The 3,090 g Weight Budget, Assembly by Assembly
Weight is the one specification every buyer asks for and almost no factory can explain. Here is ours, for the standard build (1680D ballistic shell, moulded EVA hood, 75 mm wheels, two-stage trolley). Eleven assemblies, 3,090 g, and a tolerance of ±5% = 154 g on the finished piece. We weigh five pieces per pallet on a 1 g scale and log the number on the inspection sheet, because a cover that drifts 200 g heavy is a cover whose foam has been downgraded.
| Assembly | Weight (g) | Share | What moves it |
|---|---|---|---|
| Outer shell 1680D ballistic + 210D lining | 760 | 24.6% | 600D saves ~110 g; 900D PU adds ~90 g |
| Moulded EVA hard-top hood (5 mm wall + rim) | 420 | 13.6% | 4 mm wall saves 60 g and loses ~15% impact margin |
| 10 mm EPE foam body wrap + egg-crate lid foam | 300 | 9.7% | 8 mm saves 60 g; do not go below 8 mm at the head end |
| HDPE spine board + base skid rails | 280 | 9.1% | 1.5 mm spine is the minimum for a 15.5 kg load |
| Pockets (3) + shoe bag + linings | 210 | 6.8% | Each extra exterior pocket is ~35 g |
| Zippers: No.10 main + two No.8 | 190 | 6.1% | No.8 main saves 45 g and halves the cycle life |
| Wheel housings, 2 × 75 mm PU wheels, axle | 330 | 10.7% | 60 mm saves 80 g; 90 mm adds 70 g |
| Two-stage aluminium trolley + pull handle | 260 | 8.4% | Single-stage saves 90 g, loses 180 mm of extension |
| Webbing, buckles, D-rings, ID window | 120 | 3.9% | Steel D-rings add 40 g and outlast plastic 3:1 |
| Piping, binding, thread, bar-tacks | 140 | 4.5% | Double-fold binding adds 25 g at every seam |
| Embroidery / print / metal plate | 80 | 2.6% | Metal plate adds 25 g and is worth it on premium SKUs |
| Total | 3,090 | 100.0% | ±5% = ±154 g |
Two things to notice. First, the hood, wheels and trolley together are 1,010 g — 32.7% of the product weight, and they are exactly the three assemblies that a cheap cover removes. A 2,300 g cover is not a lighter version of this one; it is a different product with a soft top, 60 mm wheels and a single-stage handle, and it will fail in a hold. Second, fabric is only a quarter of the weight. Buyers spend most of a specification meeting on fabric choice, which is the one decision that moves weight least.
The Hard Top: Hood Geometry and Club-Head Protection
The hood is the reason this product exists in the form it does. A 14-club set has its mass concentrated in 14 steel or titanium heads inside a 36 cm circle, and in a hold that mass arrives as a point load. The hood has to do three things at once: hold the shape when something heavy lands on it, spread that load across the full top face, and stay light enough that the cover still sells.
Hood specification
| Parameter | Specification | Why it is set there |
|---|---|---|
| Hood height | 300–350 mm from the top seam | Clears a 46–48 in driver plus a headcover; shorter and the driver shaft loads the hood rim |
| Wall | 5 mm moulded EVA, 60–70 shore A | 4 mm saves 60 g but loses ~15% of impact margin at the rim |
| Rim reinforcement | 2.0 mm HDPE hoop, 20 mm deep, bonded | Stops the rim folding inward when the cover lands on its end |
| Lid foam | 15 mm egg-crate, 25 kg/m³ | Conforms to head shapes; flat foam transmits the impact straight to the crown |
| Inner tie-down | Two 25 mm webbing straps + side-release buckles | Keeps the club bundle from sliding 40 mm into the hood on impact |
| Top opening | Full-length No.10 zip, two sliders, 340–380 mm gap | A single slider means the customer opens it from one end only; two sliders halve the opening time at the boot |
| Badge area | Flat 120 × 45 mm panel on the hood face | Moulded-in flat, not stitched, so a print or metal badge sits flush |
How the club head is actually protected
Protection is a stack, and each layer has a job. From the outside in: the EVA hood takes the impact and spreads it over roughly 300 cm²; the 15 mm egg-crate foam deforms locally so the load does not concentrate on one crown; the two tie-down straps stop the bundle from travelling and re-impacting; the 210D lining stops abrasion between heads; and the HDPE spine stops the whole assembly from folding at the shaft line. Remove any one layer and the failure moves to the next, which is why a soft-top cover with excellent foam still dents drivers: the foam has nothing behind it.
We test the stack with a 4.5 kg drop mass from 300 mm onto the hood face, three positions (centre, rim, corner), with a 14-club dummy load inside. Pass criteria are no perforation of the hood, no permanent set above 4 mm, and no contact between the drop mass and any club-head surrogate. That is our internal protocol; it is not an airline or third-party certification, and we do not present it as one.
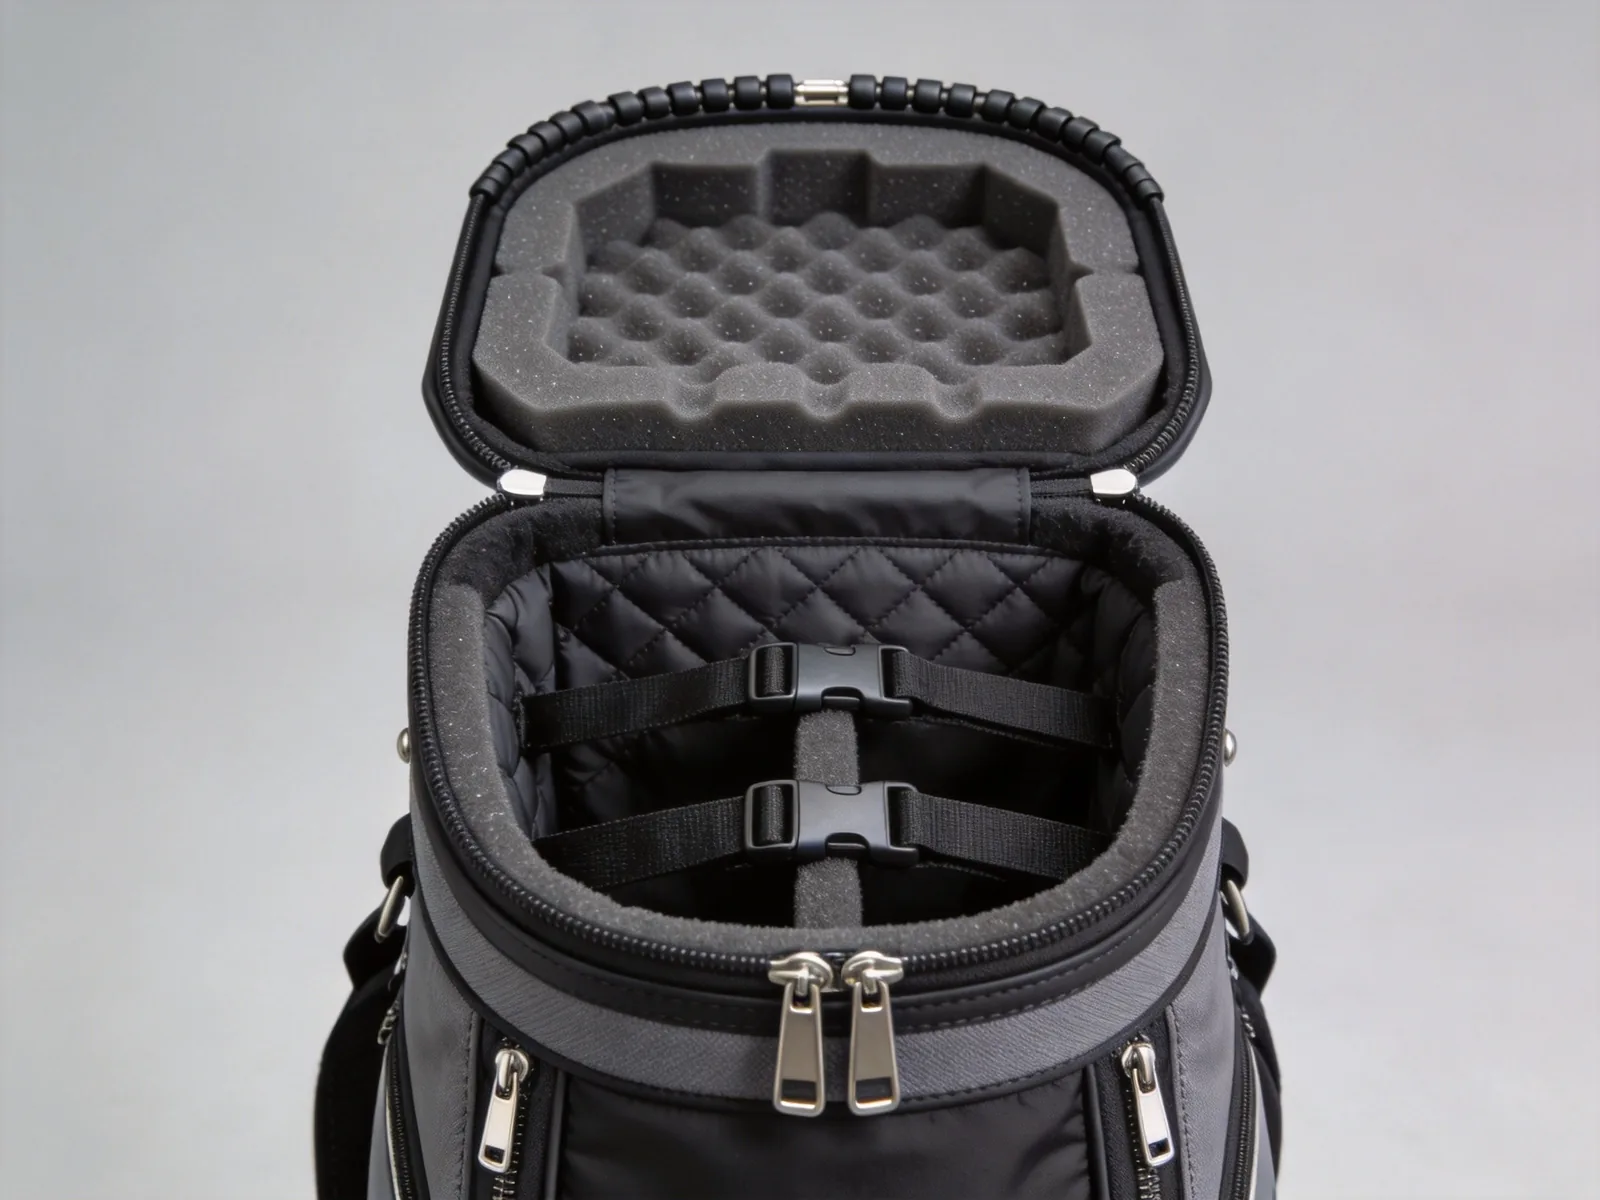
Inside the hood: 15 mm egg-crate lid foam, quilted 210D lining, two 25 mm tie-down straps and the reinforced rim hoop. This is the assembly that takes the club-head impact.
Shell Materials and Coatings
Six materials cover everything we build in this category. The cost index is relative to 600D PU polyester at 1.00, and the weight column is per cover in the standard 130 × 36 × 36 cm build.
| Material | Weight | Coating / backing | Cost index | Best used for |
|---|---|---|---|---|
| 600D polyester, 220 g/m² | ~650 g | PU 1,500 mm | 1.00 | Entry retail, rental fleets, promotional |
| 900D polyester, 300 g/m² | ~790 g | PVC or PU 2,000 mm | 1.18 | Value retail where hand-feel matters more than weight |
| 1680D ballistic nylon, 420 g/m² | ~760 g | PU 3,000 mm | 1.62 | Our default: abrasion resistance at the wheel end and the top rim |
| 1680D + TPU laminate, 460 g/m² | ~820 g | TPU 5,000 mm, seam-taped | 1.94 | Wet-climate markets, tour operators, rental in Asia-Pacific |
| 1.2 mm PU leatherette panel | +110 g (panel only) | Knitted backing | +USD 1.10–1.90 | Premium SKUs, logo panel, contrast piping |
| 5 mm moulded EVA (hood) / 2.5 mm ABS (hard case) | 420 g / 2,100 g | N/A | hood 11% of BOM / case +USD 14–22 | Hood on the workhorse build; ABS on the premium case |
Three material decisions worth arguing about, because they are the ones buyers get wrong:
- Do not downgrade the fabric at the wheel end. Abrasion on a travel cover is not uniform. The base 25 cm and the top rim take almost all of it, because that is where the cover is dragged and where it lands. We use the same 1680D everywhere for simplicity, but a legitimate cost-down is 600D on the body with a 1680D base panel and rim — about USD 1.40 saved with no change in the failure rate.
- PVC is cheaper and it is a compliance liability. A PVC-coated shell costs roughly 12% less than a PU-coated one and is being pushed out of EU retail by packaging and substance rules. If your market is the EU or the UK, specify PU or TPU and put it on the spec sheet, because the difference is invisible until a customer tests it.
- Seam tape is the difference between water-resistant and waterproof. A 5,000 mm TPU laminate with untaped seams leaks at the needle holes in a 20-minute apron downpour. Taping adds USD 0.60 and 35 g, and it is the only way to claim water resistance honestly on a sewn product.
Wheels, Trolley and Base: the 76 N Load Path
The wheel assembly is where a travel cover earns its reputation. Loaded at 15.5 kg, each of the two wheels carries 76 N at rest and considerably more in motion: every kerb, taxi rank lip and baggage carousel edge multiplies that by three to five. A 60 mm wheel with a 6 mm axle survives a terminal floor and fails on a kerb; a 75 mm wheel with an 8 mm axle survives both.
| Component | Specification | Test | Failure it prevents |
|---|---|---|---|
| Wheel | 75 mm PU tyre, 8 mm steel axle, sealed bush | 5 km roll on a 3 mm steel ridge at 12 km/h, loaded | Flat-spotting and axle bend at kerbs |
| Wheel housing | Moulded nylon 66, 4 rivets + 2 bar-tacks into 1.5 mm HDPE | 300 N lateral push, 10 cycles | Housing tear-out, the number one claim on cheap covers |
| Base skid rails | Two 25 mm webbing rails + 3 mm HDPE board | 20 drags of 2 m on concrete, loaded | Base abrasion through the shell at the trailing corner |
| Trolley | Two-stage aluminium, 180 mm + 180 mm extension, push-button lock | 500 N static pull 10 s; 3,000 extend/retract cycles | Handle pull-out and lock collapse under handler lift |
| Pull handle | 40 mm webbing, box-X stitched, 900 N rated | 500 N static, 60 s | Stitch failure when the cover is dragged off a belt |
| Standing stability | Base footprint 34 × 22 cm, wheels inset 30 mm | Static tilt test at 12° | Cover falling over in a hotel lobby and cracking the hood rim |
The 500 N pull test deserves a sentence of its own. It is 51 kg of force, more than three times the loaded weight, applied for a full minute to the pull handle and to the trolley in its extended position. It is not a realistic handling load; it is a safety factor, and it is the test that separates a cover with riveted anchor plates from one with a stitched-on handle. If a supplier cannot tell you what their handle is tested to, they have not tested it.
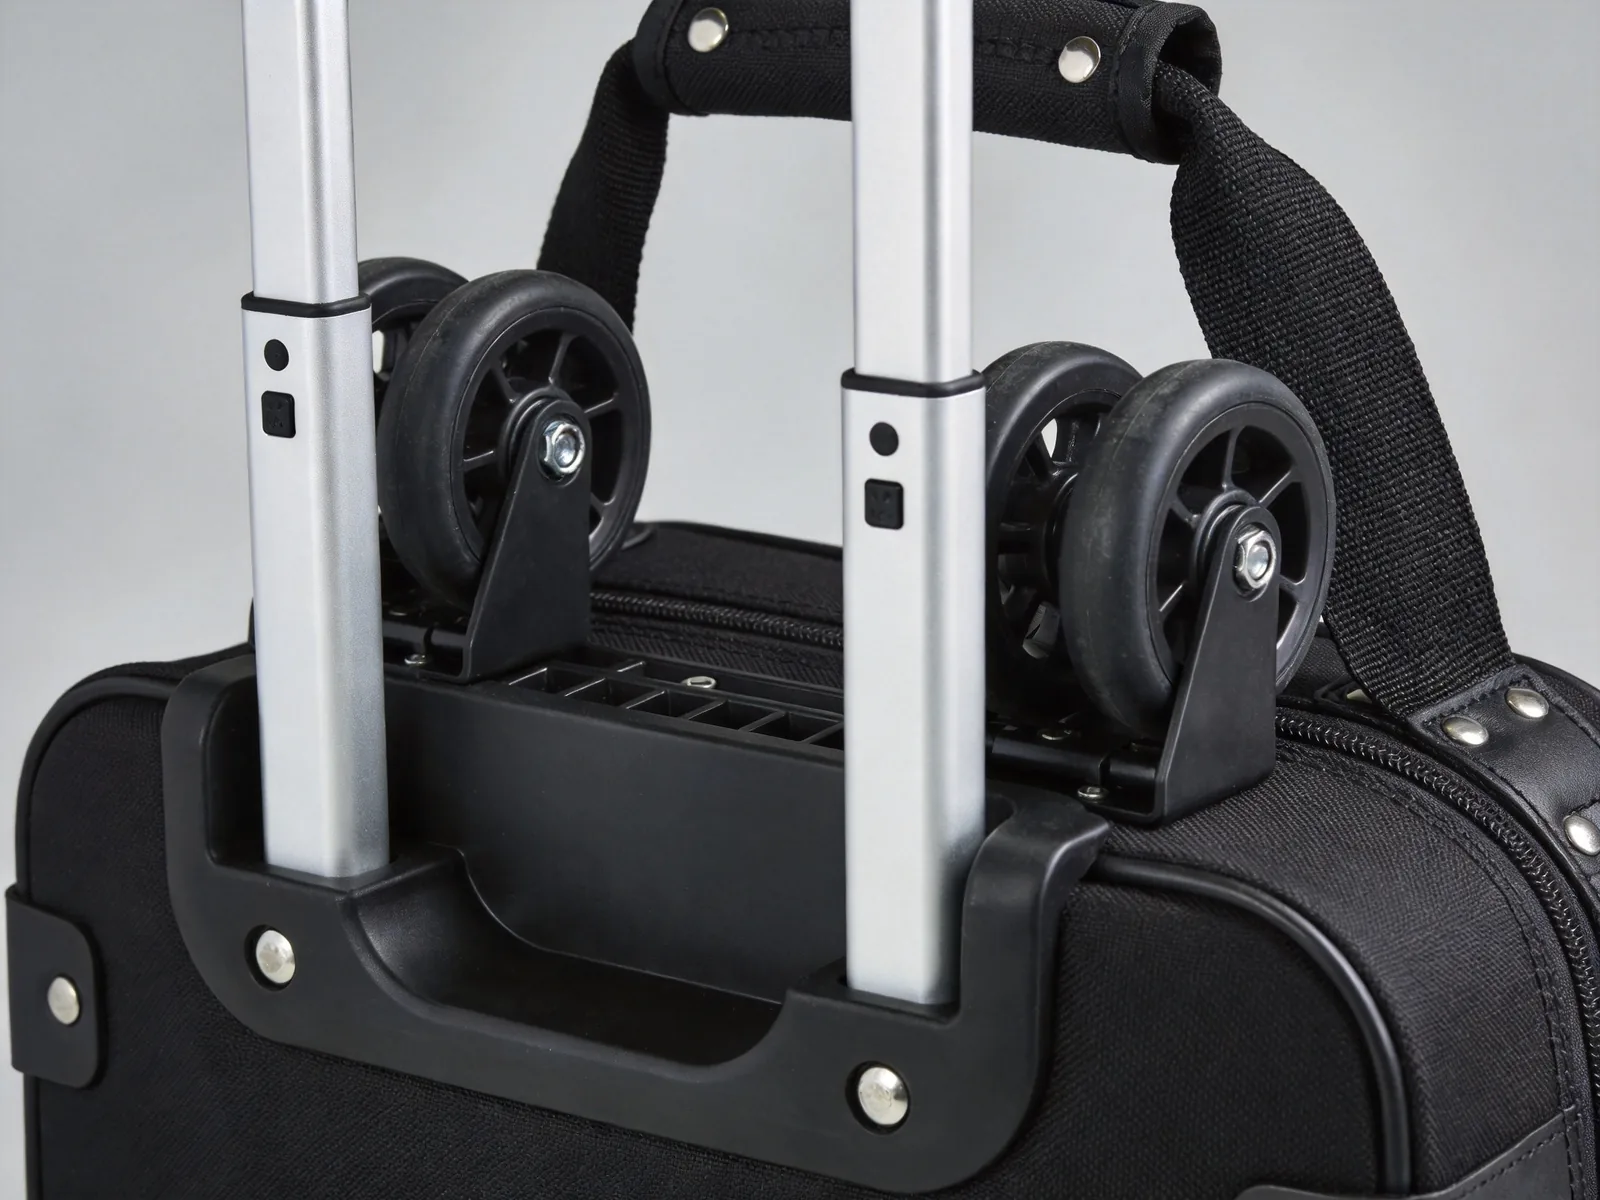
The load path: 75 mm PU wheels in moulded nylon housings, four rivets and two bar-tacks per side, 3 mm HDPE base board, two-stage aluminium trolley with a push-button lock.
Interior Layout and Packing Volume
A cover is bought for capacity and returned for capacity, in the sense that a cover which does not take a full set plus shoes plus a rain suit gets returned once. The internal layout we build to:
- Club capacity: 14 clubs plus a 460 cc driver, with the heads sitting in the hood and the grips at the base. A cart bag goes in whole; a staff bag needs the 38 cm section version.
- Three-point tie-down: two 25 mm straps at the head end and one at the shaft mid-point, so the bundle cannot slide 40 mm into the hood on impact.
- Shoe pocket: 330 × 200 × 130 mm, ventilated with two brass eyelets, positioned at the base opposite the wheel side so it does not add to the pull weight.
- Exterior pockets: one full-length front pocket (400 × 250 mm) for a rain suit, one 200 × 150 mm accessory pocket, one flat document pocket with an ID window.
- Compression: two side straps so the cover can be pulled down to 32 cm section when it carries 12 clubs instead of 14. This is worth about 0.008 CBM per piece in the carton.
- Internal lining: 210D taffeta, quilted at the hood only. Quilting the full body adds 90 g and no protection.
One volume check worth doing before you approve a sample: pack it with 14 clubs, a pair of size-45 golf shoes and a folded rain suit, then measure. If the main zip needs two hands and a knee, the section is 2 cm too small and every customer will notice on the first trip. We build 36 cm section for exactly that reason, and we will tell you when your own product brief asks for 34.
Bill of Materials at USD 38.50 FOB
Ten lines, 100% of the price, on the standard build at 500 pieces. This is a costing structure, not a quotation: your specification, quantity and decoration will move it, and we quote from your spec sheet rather than from this table.
| BOM line | Share | USD @ 38.50 | Notes |
|---|---|---|---|
| Shell, lining and foam | 17.0% | 6.54 | 1680D ballistic, 210D lining, 10 mm EPE, egg-crate lid |
| Moulded EVA hood | 11.0% | 4.24 | 5 mm wall, rim hoop, badge flat |
| Frame, base and skid rails | 7.0% | 2.69 | 1.5 mm HDPE spine, 3 mm base board, webbing rails |
| Wheels, housings and trolley | 14.0% | 5.39 | 2 × 75 mm PU, nylon 66 housings, two-stage aluminium |
| Zippers and hardware | 8.0% | 3.08 | No.10 main, two No.8, sliders, D-rings, buckles |
| Pockets and webbing | 6.0% | 2.31 | Three exterior pockets, shoe bag, compression straps |
| Decoration | 4.0% | 1.54 | Embroidery, heat transfer, woven label |
| Labour | 19.0% | 7.32 | ~1.9× the seam metres of a cart bag |
| Overheads and packing | 10.0% | 3.85 | Polybag, carton, QC, factory overhead |
| Factory margin | 4.0% | 1.54 | At 500 pieces; improves with volume |
| Total FOB | 100.0% | 38.50 | Ex-works Shenzhen / Xiamen, FOB terms |
Price ladder and what actually moves the number
| Quantity | Unit FOB | vs 500 pcs | What changes |
|---|---|---|---|
| 500 pcs | USD 38.50 | — | Tooling amortised over the run |
| 1,000 pcs | USD 36.19 | −6.0% | Fabric buying tier, cutting efficiency, tooling spread |
| 2,000 pcs | USD 34.61 | −10.1% | Longer cutting runs, hood mould fully absorbed |
| 5,000 pcs | USD 32.88 | −14.6% | Fabric on contract, dedicated line, packaging on pallet |
The ladder is real but it is not the biggest lever. In our experience the four decisions that move a travel cover’s cost most, in order, are: (1) architecture — soft versus hard top is a USD 4–6 swing and a tooling decision; (2) section size — 2 cm of section is 0.008–0.012 CBM, which is freight, which is cash; (3) hood tooling — a new hood mould is USD 2,200–3,800, so reusing an existing hood shape with your own badge insert saves most of it; (4) fabric — 600D instead of 1680D saves USD 2.10 and is the change most likely to come back as a claim. Negotiating the margin line is fifth.
Tooling, Moulds and Amortisation
Travel covers carry less tooling than a moulded hard case and more than a soft bag. Five items cover the standard build; the table gives the range and the per-piece amortisation at three volumes, so you can see where a 500-piece order is actually paying for the mould.
| Tooling item | Cost (USD) | /500 pcs | /2,000 pcs | /5,000 pcs |
|---|---|---|---|---|
| EVA hood mould (one size, one shape) | 2,200–3,800 | 4.40–7.60 | 1.10–1.90 | 0.44–0.76 |
| Hood logo insert (your mark, moulded in) | 320–600 | 0.64–1.20 | 0.16–0.30 | 0.06–0.12 |
| Wheel housing tool (nylon 66) | 900–1,600 | 1.80–3.20 | 0.45–0.80 | 0.18–0.32 |
| Embroidery plate | 60–120 | 0.12–0.24 | 0.03–0.06 | 0.01–0.02 |
| Screen print frame (per colour) | 45–90 | 0.09–0.18 | 0.02–0.04 | 0.01–0.02 |
| Total | 3,525–6,210 | 7.05–12.42 | 1.76–3.10 | 0.70–1.24 |
Read the first column against the second: at 500 pieces, tooling adds USD 7.05–12.42 per cover, which is 18–32% of the FOB price. That is why a 500-piece run at a new hood shape is not the cheapest way to enter the category. Two ways to reduce it, both legitimate: use an existing hood shape and tool only your logo insert (USD 320–600 instead of USD 2,200–3,800), or order the hood mould as a shared investment across two colourways and two sizes in the same run. We will quote both, and we will tell you which hoods already exist before you design a new one.
Sampling in 6–10 Working Days
Sampling starts when the specification is locked, not when the enquiry arrives. The four stages below are what happens inside those 6–10 working days; the clock only starts once we have your material call, your dimensions, your logo artwork and your target price confirmed in writing.
| Stage | Days | What is produced | What you approve |
|---|---|---|---|
| 1. Spec lock and pattern check | 1–2 | Dimensioned drawing, BOM, material swatches, hood choice from existing shapes | Drawing and swatch card — sign before cutting |
| 2. Cut and pre-assembly | 2–3 | Cut panels, foam, spine board, hood, wheel housings | Nothing; this is the risk point for fabric availability |
| 3. Sew and assemble first sample | 2–3 | One finished sample, decoration applied, weighed and measured | Weight, dimensions, decoration position |
| 4. Fit and function review | 1–2 | Loaded with 14 clubs + shoes, wheel and handle check, photo set, revision list | Sample approval or a marked-up revision |
Two rounds of revision are included. A third round is chargeable at USD 60–120 per sample, because by then the change is usually a design change rather than a correction. What we ask you to send with the enquiry, to keep the 6–10 days honest: reference product or photos, target dimensions, target FOB, target retail price, decoration artwork in vector, and the market you sell into (that last one decides the coating and the compliance pack).
Bulk Production in 35–50 Days
Bulk starts after sample approval and deposit. The eight stages below sum to 35–50 days depending on material lead times; the two variables that push a run to the top of the range are custom-dyed fabric (+10–15 days) and the March–May peak (+7–10 days), because that is when every golf brand in the northern hemisphere wants its covers at the same time.
| Stage | Days | Output / checkpoint |
|---|---|---|
| 1. Material in and inspection | 5–8 | Fabric, foam, zippers, wheels, trolley in; AQL 4.0 incoming check |
| 2. Cutting | 4–6 | Panels, foam, spine boards cut to the approved pattern; first-off check |
| 3. Printing / embroidery | 3–5 | Decoration before assembly; colour and position sign-off |
| 4. Sub-assembly | 5–7 | Hoods, pockets, wheel housings, handles built as sub-lots |
| 5. Main assembly | 8–12 | Body sewn, spine and base fitted, hood attached, wheels and trolley mounted |
| 6. In-line inspection | ongoing | Every 50 pieces: dimensions, weight, seam, wheel spin, zip function |
| 7. Final inspection and packing | 4–6 | AQL 2.5 major / 4.0 minor, then polybag and carton |
| 8. Carton marking, palletising, handover | 2–3 | Shipping marks, FBA or retail labels, loading photos, booking |
Two production details that decide whether the run lands on time: hoods are moulded in a separate lot before assembly, so a hood mould that is not ready stops the line on day 20 rather than day 2; and wheels and trolleys are the longest-lead hardware at 12–18 days, which is why we confirm them at the sampling stage rather than after the deposit. If your launch date is fixed, tell us the date and we will work backwards and say whether it is achievable instead of accepting it.
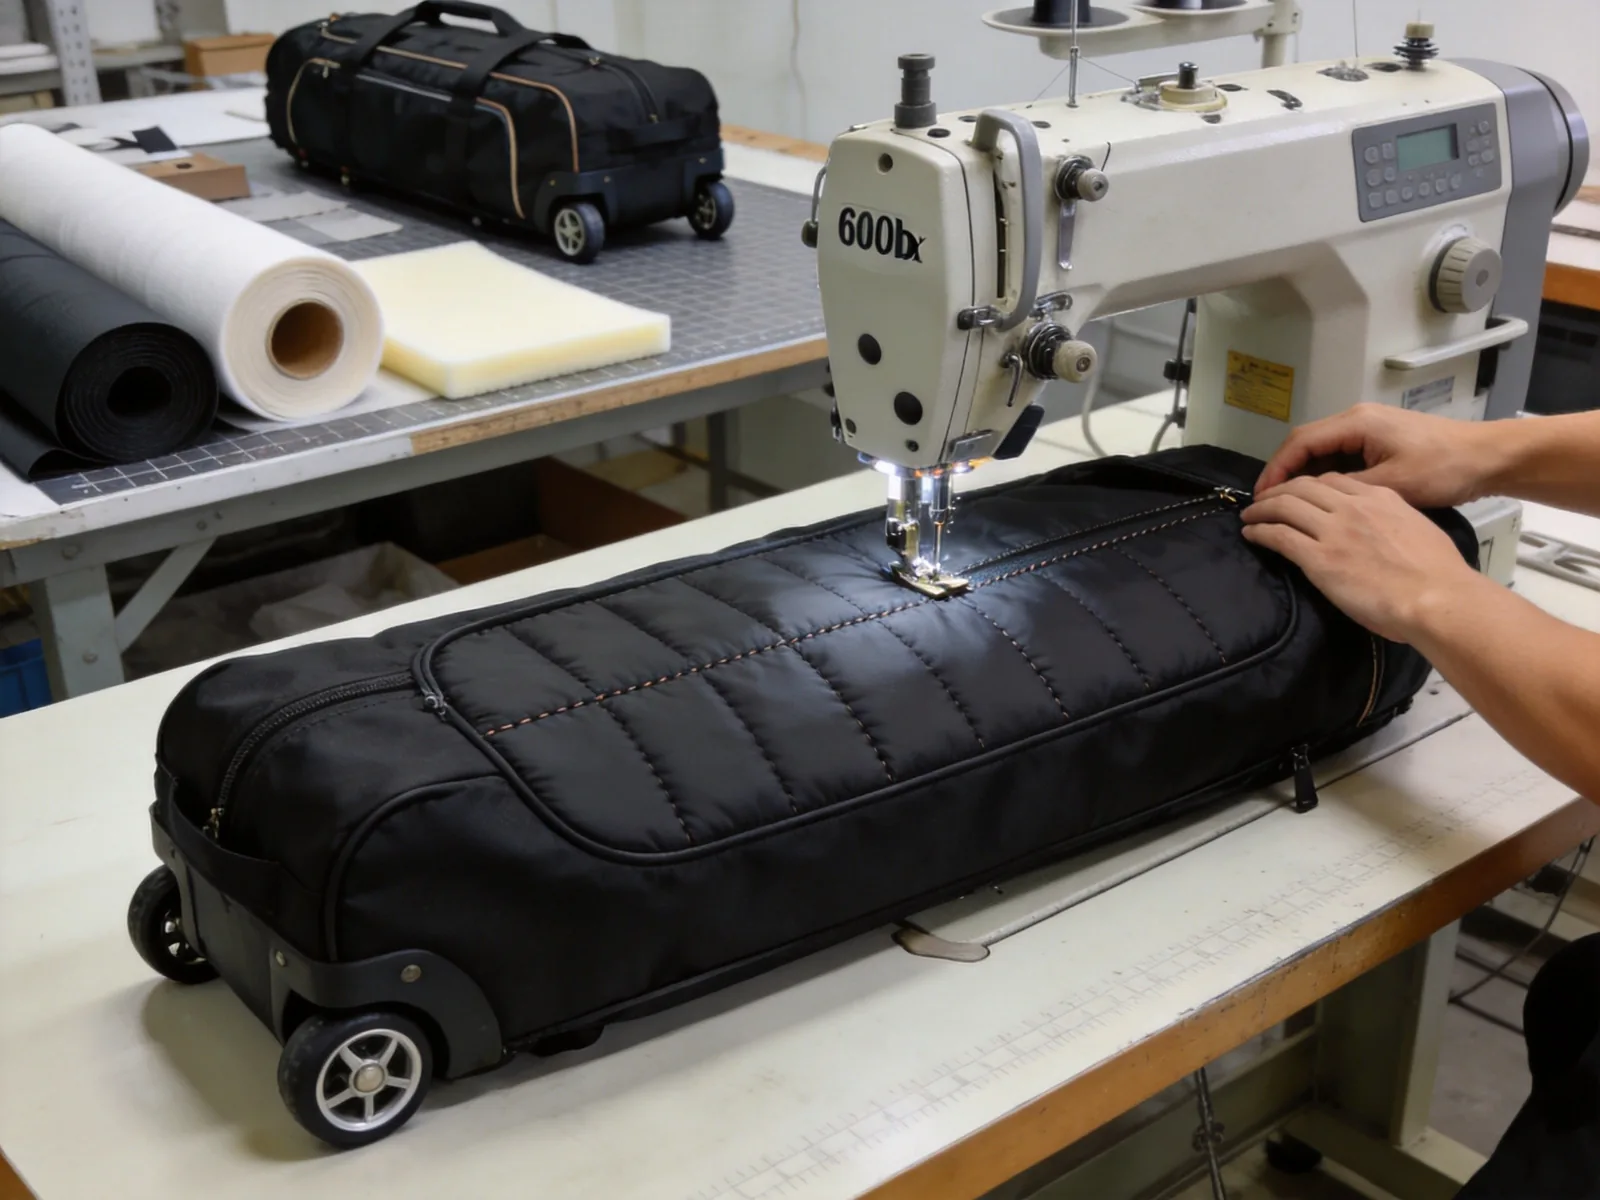
Body panel assembly: the padded shell is sewn as a sub-assembly before the spine board, base and hood go on. Roughly 1.9× the seam metres of a cart bag in the same slot.
Twelve Tests and Five Inspection Gates
Every test below is part of our internal protocol for this product. They are bench tests we run on the sample and on a production sample from each lot; they are not third-party certifications, and we do not describe them as such. If your programme needs a notified-body or lab report, we will prepare the samples and you commission the lab.
| # | Test | Method | Pass criteria |
|---|---|---|---|
| 1 | Drop, loaded | 1.2 m free fall, 6 faces + 3 edges, 15.5 kg dummy load, concrete | No perforation, no permanent set > 4 mm, clubs undamaged |
| 2 | Club-head impact | 4.5 kg mass from 300 mm onto hood centre, rim and corner | No hood perforation, no contact with head surrogate |
| 3 | Static compression | 250 kg for 60 min on the packed cover | No permanent set > 6 mm, zip still operates |
| 4 | Wheel roll | 5 km on a 3 mm steel ridge at 12 km/h, loaded | No flat spot, no axle bend, wheel still round within 1 mm |
| 5 | Wheel housing pull | 300 N lateral, 10 cycles | No tear-out, no rivet elongation |
| 6 | Handle static pull | 500 N for 60 s on pull handle and extended trolley | No stitch failure, no lock collapse |
| 7 | Trolley cycle | 3,000 extend / retract cycles | Lock holds, no play > 3 mm |
| 8 | Zipper cycle | 3,000 open / close cycles under 5 kg load | No skipped teeth, slider still self-locks |
| 9 | Rain spray | 60 L/m²/h for 30 min, cover upright and on its side | No water in the shoe pocket or hood interior |
| 10 | Abrasion | Taber, 1,000 cycles, base panel and top rim | No substrate show-through |
| 11 | Cold flex | −10 °C for 4 h, then 20 flex cycles at the hood rim | No cracking of EVA or coating |
| 12 | Salt spray, hardware | 48 h neutral salt spray on plated parts | No red rust > 2% of surface |
Five gates control the run. Gate 1 incoming material (AQL 4.0, fabric weight and coating checked against the approved swatch). Gate 2 first-off after cutting and after decoration. Gate 3 in-line every 50 pieces (dimensions, weight, wheel spin, zip, seam). Gate 4 pre-final before packing. Gate 5 final inspection to AQL 2.5 major / 4.0 minor, with four defects treated as critical and zero-tolerance: hood perforation, wheel housing separation, main-zipper failure, and any sharp edge on the trolley lock. Critical defects stop the lot, not the sample.
Compliance Boundaries — What We Do and What We Do Not
Compliance is the part of a specification where a supplier’s over-claiming becomes your liability, so we state the boundary plainly.
- What we supply: material declarations for shell fabric, coating, foam, webbing and zippers from our mills; a REACH SVHC statement at the material level; a California Proposition 65 statement on the components we buy; a packing list and HS code proposal; and, where you need it, samples for your own lab testing.
- What we do not do: we are not a certification body, a notified body, an EU authorised representative, or a GPSR responsible person. We do not issue CE, UKCA or CPSIA certificates, and we do not sign declarations on your behalf. If your market requires those, you appoint the responsible entity and we support it with documents.
- What we flag early: PVC-coated shells where the destination is the EU or UK; nickel-release risk on cheap plated D-rings; azo dyes in low-cost webbing; and phthalates in soft PVC trims. All four are cheap to avoid at specification stage and expensive to fix after the container ships.
- Packaging and EPR: retail cartons, polybags and hangtags all fall under packaging EPR schemes in several EU markets. We can print your EPR registration number and the material codes on the carton, but the registration is yours.
Packing, Cubic and Landed Cost
This is the section most quotations leave out, and on a 130 cm product it is the section that decides your margin. Three packing configurations, all real, all quoted on request:
| Packing | Carton (cm) | CBM / carton | CBM / pc | 20GP | 40HQ | Ocean / pc* |
|---|---|---|---|---|---|---|
| Single, 1 pc/ctn | 135 × 40 × 25 | 0.1350 | 0.1350 | 207 pcs | 503 pcs | USD 5.17 |
| Nested, 2 pcs/ctn (hoods off, bodies nested) | 135 × 42 × 38 | 0.2155 | 0.1077 | 259 pcs | 631 pcs | USD 4.12 |
| Retail display, 1 pc/ctn | 138 × 42 × 28 | 0.1623 | 0.1623 | 172 pcs | 419 pcs | USD 6.21 |
*At USD 2,600 per 40HQ, 68 CBM usable, 28 CBM usable in a 20GP. Ocean freight only — excludes origin charges, destination charges, duty and VAT.
Nesting two pieces per carton is the single best freight decision available on this product, and it is a design decision, not a packing decision: it only works if the hood is removable with two buckles rather than bonded to the body. That is why our standard hood attaches with a zip-and-buckle system instead of being sewn in. It costs USD 0.35 in hardware and saves USD 1.05 per piece in ocean freight, plus 128 more pieces per 40HQ. On 5,000 pieces that is USD 5,250 — more than the hood mould.
Landed cost worked example (500 pcs, nested, EU destination)
| Line | Per piece | Basis |
|---|---|---|
| FOB | USD 38.50 | 500 pcs, standard build |
| Ocean freight | USD 4.12 | Nested 2 pcs/ctn, 40HQ at USD 2,600 |
| Insurance | USD 0.43 | 1% of CIF value |
| Duty at 6.5% | USD 2.80 | Indicative HS 4202 rate; confirm with your broker |
| Destination charges | USD 1.20 | THC, docs, delivery order |
| Landed (pre-VAT) | USD 47.05 | Excludes VAT and last-mile |
Landed cost is 22% above FOB before VAT. A brand selling at USD 129 retail with a 45% wholesale margin buys at roughly USD 55, which leaves about USD 8 of headroom over this landed cost — and that headroom is where decoration, retail packaging and your own freight variance live. It is worth doing this arithmetic before the design review, not after.
Six Channels and How the Specification Changes
| Channel | What they buy | Specification shift |
|---|---|---|
| Golf retail / pro shops | 2–3 SKUs, brand-led | 1680D, moulded hood, full-colour print, retail carton |
| DTC / online brand | 1 hero SKU + 1 colour | Strong hood badge, unboxing insert, polybag + mailer carton |
| Tour operators and rental fleets | 200–1,000, replaceable | 600D shell, soft or 4 mm hood, fleet ID panel, no retail packing |
| Corporate and promotional | 500–5,000, logo-led | 600D, single-colour print, cheapest wheel set that passes test 4 |
| Airline / travel retail | Dimensional compliance first | 125–130 cm length, 34–36 cm section, weight under 3.0 kg |
| Premium travel goods | Hard case or leather-trim cover | ABS clamshell or PU leather panels, metal plate, 1,000 pcs minimum |
ECN, Spare Parts and Reorders
A travel cover programme runs for years, and the second order is where most supplier relationships break. Three mechanisms keep it working:
- ECN control. Any change to material, dimension, hood shape, wheel or decoration gets an engineering change note with a revision number, a reason, an effective date and a stock-cutover plan. Your PO revision and our BOM revision must match before cutting starts.
- Spare parts at 1%. Wheels, trolley assemblies, sliders and buckles shipped at 1% of order quantity, packed separately and marked. It costs about USD 0.28 per piece and removes most of the after-sales friction in year one.
- Reorder in 25–30 days. Same specification, same materials, no new sampling: 25–30 days instead of 35–50, because the pattern, hood mould and decoration screens already exist. Reorders are also where the price ladder actually pays out, since tooling is fully amortised.
Eight Failure Modes and the Specification That Prevents Them
| Failure | Where it shows | Root cause | Specification fix |
|---|---|---|---|
| Dented driver crown | Hood interior, first trip | Soft top or 8 mm foam with no rigid layer | 5 mm EVA hood + 15 mm egg-crate + two tie-downs |
| Hood rim cracked | Top edge, after a fall | No rim hoop; EVA too hard | 2.0 mm HDPE hoop bonded in, 60–70 shore A |
| Wheel housing torn out | Base corner | Stitched housing into shell only | Moulded nylon 66 + 4 rivets + 2 bar-tacks into 1.5 mm HDPE |
| Wheel flat-spotted | After one trip | 60 mm hard wheel on kerbs | 75 mm PU, 8 mm axle, sealed bush |
| Trolley lock collapses | Handler lift | Single-stage friction lock | Two-stage push-button lock, 500 N static test |
| Main zip splits | Over-packed cover | No.8 zip on a 36 cm section | No.10 main zip, two sliders, 3,000-cycle test |
| Water in the shoe pocket | Apron, wet weather | Untaped seams, PU 1,500 mm | TPU 5,000 mm, taped seams, eyelet drainage |
| Shell abraded at base | Trailing corner | No skid rail, thin coating | 1680D base panel + two webbing skid rails |
Twelve Questions to Ask Any Supplier — Including Us
- What is the empty weight of the approved sample, and what is the tolerance on the finished piece?
- Is the hood moulded, and what is its wall thickness and shore hardness?
- How is the wheel housing attached — stitching, rivets, or both — and into what substrate?
- What is the pull handle tested to, in newtons, and for how long?
- What zip size is on the main opening, and how many sliders?
- Is the shell PU, PVC or TPU, and what hydrostatic head?
- Are seams taped on the waterproof version, or only coated?
- What is the carton cube per piece, and can the product nest two per carton?
- Which tooling is new for my order, and what does it cost at my quantity?
- What are the four critical defects at final inspection, and what happens when one is found?
- Who issues the compliance documents, and who is the responsible person in my market?
- What is the reorder lead time with no changes, and what spares ratio do you ship?
If a supplier answers all twelve with numbers, you are dealing with a factory. If the answers are adjectives, you are dealing with a trading company that will sub-contract the run — which is not automatically wrong, but it changes who owns the claim when the first wheel housing tears out.
Frequently Asked Questions
Send the Specification, Get the Numbers
Tell us the length, section, target weight, hood type, fabric and quantity. We will come back with a dimensioned drawing, a BOM at your quantity, the tooling list with amortisation, and a sampling slot in 6–10 working days. MOQ 500 pieces, bulk 35–50 days, AQL 2.5 major / 4.0 minor, and a factory that has been building bags since 2014 with a founder in the trade since 2004.
Related Pages on This Site
- Custom Golf Staff Bag Manufacturer — Tour Bags, Weight Budgets, MOQ 500
- Custom Golf Cart Bag Manufacturer — OEM/ODM Cart Bags and Tooling
- Custom Golf Sunday Bag Manufacturer — Ultralight Carry Bags
- Custom Golf Stand Bag Manufacturer — OEM/ODM Stand Bags
- Custom Golf Staff Bags — Product Range
- Golf Staff Bag Private Label Programme
- Can You Take a Golf Bag on a Plane? Airline Rules and Packing
- Custom Luggage and Travel Bags — OEM/ODM
- Custom Travel Bag Manufacturer
- Custom Garment Bag Manufacturer — Suit Covers
- Custom Golf Shoe Bags — OEM/ODM
- Custom Leather Golf Bags