A bag manufacturer established in 2014, with our founder working in the bag trade since 2004. We produce private-label drawstring bags and cinch sacks — flat promotional sacks, drawstring backpacks with padded straps, barrel bags, mesh gym bags, cotton canvas sacks, RPET and recycled shells — for promotional distributors, gym and fitness brands, schools and sports clubs, retail and DTC labels, outdoor brands and hospitality groups, in 190T–600D polyester, 210D–600D RPET, 8 oz and 12 oz cotton canvas, poly mesh and non-woven PP.
Short answer for buyers: a drawstring bag is a single-panel bag closed by a cord running through a sewn channel at the top, and the four specifications that decide whether a program is profitable are the shell weight, the cord-channel construction, the cord and cord-lock grade, and the strap attachment. Shell weight sets the unit cost more than anything else — 190T–210D polyester at 60–75 gsm is the giveaway grade, 420D at around 110 gsm is the retail mid-grade, and 600D at around 200 gsm is the durable gym grade, with roughly a 1.0 : 1.25 : 1.45 cost index between them. The channel is where cheap bags fail: a 20 mm finished casing with a single row of lockstitch at 8–10 stitches per inch, double-stitched and bar-tacked at both eyelet ends, survives a season of gym use, while a 15 mm casing with an overlocked edge splits at the eyelet within weeks. We build drawstring bags at 500 pieces per style, sample them in 6–10 working days, run mass production 35–50 days after sample approval, and inspect to AQL 2.5 major / 4.0 minor.
What a Drawstring Bag Actually Is — Five Structures That Share a Name
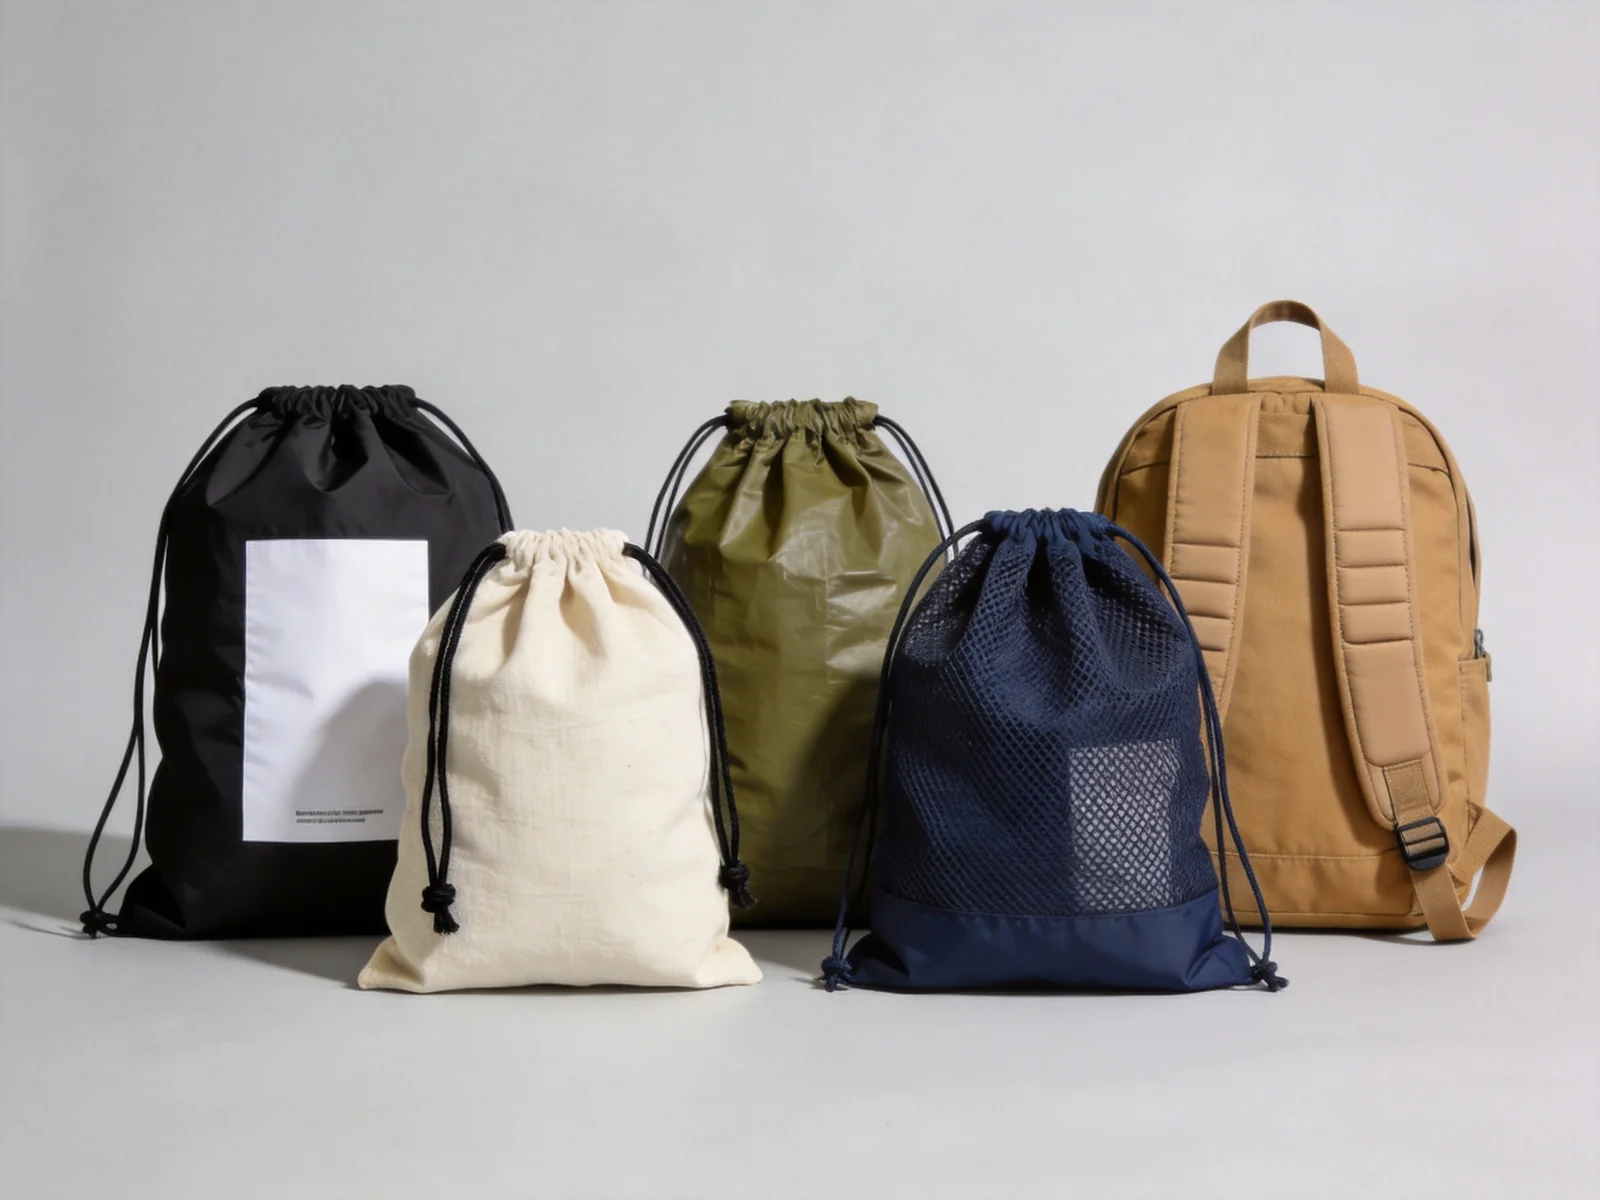
“Drawstring bag” is used for five different products that share one closure mechanism and almost nothing else. A promotional cinch sack, a drawstring backpack, a barrel bag, a mesh swim bag and a cotton canvas gift sack are bought by different departments, priced on different cost structures and inspected against different criteria. Before a quotation means anything, the buyer has to fix which of the five the range needs, because the pattern, the cord consumption and the labour content differ by a factor of two to three between them.
| Code | Structure | Body | Closure | Typical buyer | Design note |
|---|---|---|---|---|---|
| DS-01 | Flat cinch sack | Single panel folded and side-seamed, no base gusset | One channel, one cord loop through both sides | Promotional distributors, events, retail giveaway | Cheapest structure per unit; the bag lies flat when empty, which is what keeps freight cost down |
| DS-02 | Drawstring backpack | Two panels, boxed or flat base, reinforced corners | One continuous cord forming both shoulder loops | Gym brands, schools, sports clubs, DTC labels | The cord is also the strap, so eyelet and bartack strength become a safety spec, not a cosmetic one |
| DS-03 | Barrel / cylindrical sack | Tube with circular or oval base, base gusset | Single channel with cord lock | Laundry, storage, outdoor, hospitality | Round base consumes more fabric and more sewing time than a flat sack; stands open when loaded |
| DS-04 | Mesh gym or swim sack | Poly mesh body with solid base panel | Channel in solid top band | Fitness, swim, dive, team kit | Mesh has to be bound at every seam or it ravels; the top band carries the entire load |
| DS-05 | Premium canvas sack | 8–12 oz cotton canvas, flat or boxed base | Wide channel, cotton or webbing drawcord | Retail, gifting, hospitality, beauty brands | Heavier shell needs a wider channel and a stronger needle; screen print sits differently on canvas than on polyester |
Two of these five account for most volume. DS-01 is the promotional workhorse, and DS-02 is the retail product that a brand can actually build a line around, because it carries weight on the shoulders and can hold a laptop sleeve, a shoe compartment or an internal zip pocket. A brand launching a drawstring range usually starts with DS-01 for the entry price point and DS-02 for the margin product, then adds DS-03 or DS-04 when the range needs a laundry, swim or kit story.
The Buying Landscape: Six Channels and What Each One Actually Needs
Drawstring bags reach us from six kinds of buyer, and the brief changes completely between them. A promotional distributor quoting a 20,000-piece event order and a fitness brand building a four-colour retail line are not buying the same product, even when both call it a drawstring bag.
| Channel | Typical order | Structure that wins | Non-negotiable requirement |
|---|---|---|---|
| Promotional distributors and agencies | 5,000–50,000 pcs, single drop, hard deadline | DS-01 flat cinch sack in 190T or 210D, one or two spot colours | Unit cost at volume; print position accuracy across the run; delivery that lands before the event date, not near it |
| Gym, fitness and studio brands | 1,000–8,000 pcs per colourway, 2–3 drops a year | DS-02 drawstring backpack in 600D or 600D RPET, padded straps | Load rating at the eyelets; a cord that does not cut into the shoulder; colour consistency across the range |
| Schools, universities and sports clubs | 500–10,000 pcs, seasonal cycles | DS-02 or DS-04 mesh, team colourways, large print area | Durability under daily adolescent use; name-tag panel; washability without print loss |
| Retail and DTC labels | 500–5,000 pcs per SKU, frequent reorders | DS-05 cotton canvas or 420D with a woven label and hangtag | Retail-ready finish; hangtag and barcode; a shell that photographs well and feels heavier than its price point |
| Outdoor and travel brands | 1,000–6,000 pcs, bundled with a main product | DS-03 barrel in ripstop nylon, or DS-01 in 210D ripstop | Packability, low packed volume, and a cord that holds a wet load without stretching |
| Hospitality, spa and gifting | 500–10,000 pcs, contract cycles | DS-05 canvas or 210D with a wide channel and cotton cord | Print quality on a premium hand-feel shell; a cord long enough to hang; packaging that survives a guest taking it home |
Those ranges are what we see in practice rather than a policy. The commercial threshold is 500 pieces per style, and inside that 500 a buyer can mix up to three colourways and two branding layouts. That is usually enough to test a colour direction or a second channel without committing a full run to one variant — which matters in this category more than in most, because drawstring bags are frequently bought as a colour story rather than as a single SKU.
The Drawstring Channel: The One Component That Decides Quality
Almost every complaint about a drawstring bag traces back to the channel — the sewn tube the cord runs through. It is a small component, roughly 2.5 metres of stitching on a standard sack, and it is where factories take cost out. The three ways to cheapen it are: narrow the casing so less fabric is consumed, skip the second row of stitching at the eyelet ends, and finish the channel edge with an overlock instead of a folded and stitched edge. Each saves a few cents; each turns a bag that lasts a season into a bag that fails in a month.
| Parameter | Specification we run | Cheap alternative and what it costs you |
|---|---|---|
| Finished casing width | 20 mm for a 4 mm cord; 25 mm for a 6 mm cord or a webbing drawcord | 15 mm casing binds the cord, so it will not close smoothly once the bag is loaded and the cord wears through the stitching |
| Channel edge finish | Fold-and-stitch with the raw edge enclosed, or binding tape on mesh | Overlock-only edge ravels after the first wash and leaves loose thread inside the channel |
| Stitch type and density | Single-needle lockstitch, 8–10 stitches per inch, bonded nylon or polyester thread | Chain stitch at 5–6 SPI: faster to sew, and it unravels from one broken stitch |
| Eyelet and end reinforcement | 12–16 mm bartack, 24–32 stitches, at both channel ends, plus a double row of stitching 30 mm either side | No bartack: the channel end opens under a pull load and the eyelet tears out of the fabric |
| Eyelet | 8 mm inner diameter brass eyelet, nickel-free plating, clinched with a die | Punched hole with no eyelet, or a thin painted eyelet: cuts the cord and rusts at the first wash |
| Cord length | Twice the channel opening circumference plus 20 cm per side, so the bag opens fully when worn as a backpack | Short cord: the bag cannot be worn on both shoulders, which is the single most common spec error we correct |
| Cord lock | Two-hole spring toggle, nylon body, or a metal toggle on premium lines | No lock, or a single-hole lock: the bag will not stay closed when carried by one cord |
There is a simple way to audit this on a sample. Load the bag to its rated weight, hold both cords, and pull the bag open and closed twenty times. A correctly built channel closes with two fingers and shows no white crease along the casing edge. Then pull one cord hard against the eyelet — 150 N is roughly a hard two-handed pull — and watch the bartack. If the fabric around the eyelet distorts before the stitch gives, the channel is right; if the stitch gives first, the sample is not ready for production.
Materials: Nine Shells and What Each One Is For
Shell choice drives 30–40% of the FOB price and 100% of how the product is perceived. The table below is the range we run as standard, with cost indexed against 210D polyester at 1.0.
| Shell | Weight | Hand feel | Print performance | Cost index | Best for |
|---|---|---|---|---|---|
| 190T polyester | 55–60 gsm | Slick, papery, light | Screen print good; sublimation needs a coated grade | 0.9 | High-volume giveaway, event bags, hotel laundry |
| 210D polyester | 65–75 gsm | Slightly textured, dry | Screen print and heat transfer both clean | 1.0 | The default promotional cinch sack |
| 210D RPET | 70–80 gsm | As 210D, marginally softer | As 210D; sublimation works on the white grade | 1.08 | Promotional programs with a documented recycled claim |
| 420D polyester | 105–120 gsm | Denser, more body | Excellent; holds fine detail | 1.25 | Retail mid-grade, school bags, brand merch |
| 600D polyester | 190–210 gsm | Rugged, structured | Excellent; embroidery also viable | 1.45 | Gym and kit bags, drawstring backpacks |
| 600D RPET | 195–215 gsm | As 600D | Excellent | 1.55 | Durable lines that need a recycled story |
| 8 oz cotton canvas | 260–280 gsm | Soft, matte, natural | Water-based screen print sits beautifully; plastisol is too heavy | 1.6 | Retail, gifting, hospitality, beauty brands |
| 12 oz cotton canvas | 390–410 gsm | Heavy, structured | Excellent, but needs a heavier mesh count | 2.0 | Premium totes and gift sacks sold as objects, not giveaways |
| Poly mesh | 180–220 gsm mesh | Open, technical | Print only on the solid band or base | 1.15 | Swim, dive, gym and team kit sacks |
| Non-woven PP | 70–90 gsm | Stiff, paper-like | Screen print only; creases show | 0.75 | Cheapest compliant giveaway where fabric is not required |
Two material decisions are worth making early. The first is whether the range needs a recycled claim, because RPET adds 8–10% to the shell cost and requires the mill’s transaction certificate to be documented against the specific order rather than implied on the box. The second is whether the shell will be printed or left plain, because a 190T shell prints cleanly with one spot colour and poorly with four, while a 600D shell holds four colours and an embroidered logo equally well. Choosing the shell before the artwork is confirmed is the most common cause of a second sample round.
Cord, Eyelet and Hardware: The Load Path
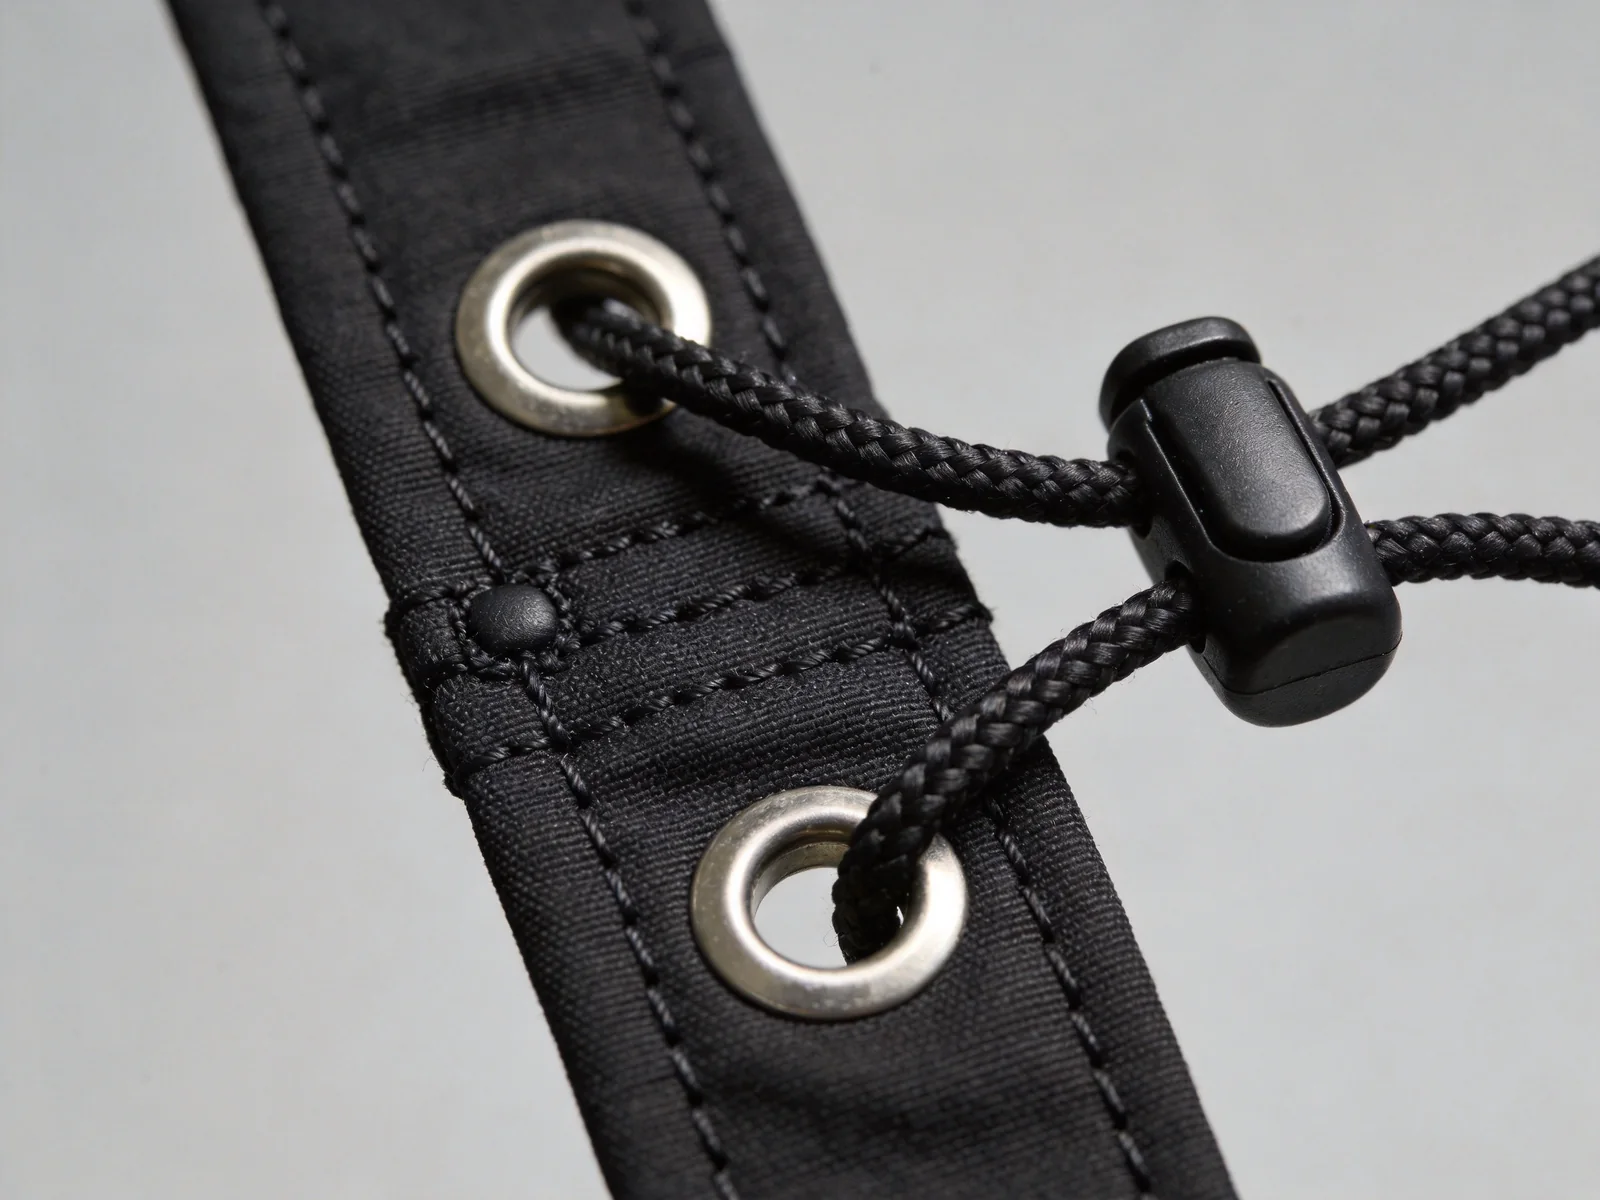
On a flat cinch sack the cord is a closure. On a drawstring backpack the cord is the entire carry system, which means the cord, the eyelet and the bartack together form a load path that has to be specified rather than inherited from a catalogue. We quote the cord by construction and breaking load, not by colour card.
| Cord | Diameter | Breaking load | Feel and behaviour | Where we use it |
|---|---|---|---|---|
| PP hollow braid | 3 mm | 60–80 kg | Stiff, light, cheapest; softens with use | Promotional cinch sacks, laundry bags |
| Braided polyester | 4 mm | 120–150 kg | Smooth, low stretch, holds a knot | Standard for drawstring backpacks |
| Cotton drawcord | 4 mm | 80–100 kg | Matte, natural, softens when washed | Canvas sacks, hospitality, gifting |
| Reflective polyester | 4 mm | 110–130 kg | Retro-reflective, slightly stiffer | School, cycling and night-safety programs |
| Elastic bungee | 3 mm | n/a (stretch) | Springs back, grips a load | Gym sacks that must hold kit tight |
| Flat webbing drawcord | 10 mm | 180–220 kg | Wide, comfortable on the shoulder, premium look | Premium backpacks and heavier loads |
The hardware set is short: eyelets, cord locks, cord ends and — on backpacks — a shoulder-strap pad or a webbing loop. We standardise on nickel-free plated brass eyelets clinched with a die rather than punched grommets, because a punched grommet in a 210D shell works loose after ten or fifteen washes. Cord ends are either heat-sealed and dipped, or finished with a metal or plastic aglet; the dipped finish costs a little more and stops the most common end-of-life complaint, which is a frayed cord end that will not pass back through the lock.
Sizing and Capacity: A Matrix, Not a Single SKU
Drawstring bags are sold by perceived size rather than by litre capacity, but capacity is what determines whether the product works for the end user. We specify every size by body dimension, flat capacity, filled capacity and rated load, and we quote the load rating because it is the number that separates a bag that survives a school year from one that does not.
| Size | Body (W × H) | Flat capacity | Rated load | Typical use |
|---|---|---|---|---|
| XS | 25 × 32 cm | 4 L | 4 kg | Kids’ event bags, shoe bags, small giveaway |
| S | 30 × 40 cm | 6 L | 5 kg | Promotional giveaway, retail gift-with-purchase |
| M | 35 × 45 cm | 9 L | 8 kg | Gym kit, school PE, general retail |
| L | 40 × 50 cm | 13 L | 12 kg | Beach, laundry, family swim |
| XL | 45 × 55 cm | 18 L | 15 kg | Team kit, equipment, bulk laundry |
| Backpack | 34 × 42 cm, boxed base | 11 L | 10 kg | Drawstring backpack with padded straps |
| Barrel | 25 cm diameter × 50 cm | 14 L | 12 kg | Laundry, storage, outdoor kit |
Rated load is not a marketing number. It is set by the weakest element in the load path: on a flat sack it is the bartack at the channel end; on a backpack it is the eyelet clinch and the cord’s own breaking load divided by a safety factor of about four. A 4 mm braided polyester cord breaks around 130 kg, which supports a 30 kg working load in theory, but the eyelet in a 210D shell will tear out long before that. That is why a 15 kg rating on an XL sack is a shell and reinforcement statement, not a cord statement.
Strap and Carry Systems
The single most under-specified element of a drawstring backpack is the strap, because the cord that closes the bag is also the strap that carries it. There are five ways to resolve that, and they differ in comfort, cost and tooling.
| Carry system | Construction | Comfort | Added cost | Recommendation |
|---|---|---|---|---|
| Cord only | One continuous cord through four eyelets, forming two shoulder loops | Low; the cord cuts in above 4–5 kg | Baseline | Promotional sacks and light retail |
| Cord with webbing loops | Cord runs through 20 mm webbing loops at the shoulder points | Medium | +3–5% | The best value upgrade for a school or gym program |
| Padded strap sections | Cord or webbing with 5–8 mm foam-filled shoulder pads | Good up to 10 kg | +12–18% | Fitness brands and daily-carry backpacks |
| Full webbing straps | 25 mm webbing straps with a cord closure in the channel, separate systems | Good; behaves like a backpack | +20–25% | Premium lines where the bag carries a laptop or shoes |
| Single-shoulder sling | One cord loop, one shoulder point, cross-body wear | Medium; suits small loads | +2% | Festival, city and kids’ lines |
When the strap is separate from the closure, the bag stops being a drawstring bag in the technical sense and becomes a backpack with a drawstring top. That is a legitimate and often better product, but it changes the pattern, the cost and the tooling, so it should be decided at the reference-sample stage rather than after the first sample.
Branding: Seven Methods and Where Each One Belongs
Branding is where a drawstring bag program is won or lost commercially, because the print method determines the minimum quantity, the colour count, the durability and the artwork deadline. We quote the method against the shell, not against a general price list.
| Method | Colours | Best shell | Durability | Cost index | Note |
|---|---|---|---|---|---|
| Screen print | 1–4 spot colours | 210D–600D polyester, cotton canvas | 30+ washes at 40 °C | 1.0 | The default for promotional volume; each extra colour adds a screen and a pass |
| Heat transfer | Full colour | 210D and up, smooth surfaces | 20–25 washes | 1.15 | Best route for photographic or gradient artwork at 500 pcs |
| Sublimation | Full colour, no limit | White or light 210D polyester with a coating | Permanent in the fibre | 1.2 | Will not work on dark shells or on cotton; the print becomes part of the fabric |
| DTF transfer | Full colour | Cotton canvas, dark polyester | 25–30 washes | 1.1 | Good small-area detail; less stretch than heat transfer |
| Embroidery | Up to 8 threads | 420D and up, canvas | Excellent, outlasts the bag | 1.6 | Not viable on 190T–210D: the fabric puckers under stitch density |
| Woven label | Any, up to 6 colours | All shells | Excellent | 1.3 | The premium alternative to printing a small logo; also carries care and origin information |
| Silicone transfer | 1–3 colours | All shells | Very good, raised feel | 1.4 | Popular on gym and outdoor lines for a tactile logo |
Print placement matters as much as method. The flat cinch sack has one large clean panel on each face, and that is the most valuable print area in the category. On a drawstring backpack the front panel is split by the channel and the cord, so the artwork has to be positioned below the channel and inside the eyelet line — a detail that is routinely missed when artwork is supplied as a flat rectangle without a placement template. We supply a placement template with the sample so that the artwork is built to the bag rather than corrected afterwards.
Colour, Pantone Matching and the Tolerances That Matter
Colour is the specification most likely to generate a dispute on a drawstring bag order, because the product is often bought as a colour story and the shell is often a stock fabric dyed in a different lot. We manage it with three controls: a lab-dip approved against the Pantone reference before bulk fabric is ordered, a master standard retained in our sample room for the life of the program, and a light-box check under D65 and TL84 at final inspection.
What can be held: dyed fabric within about 1.5 ΔE of the approved lab dip, screen-print ink within about 2 ΔE, and repeat orders within the same mill lot family. What cannot be held is an exact match across two different materials — a 600D polyester shell and a cotton canvas shell in the “same” colour will never read as identical under both daylight and shop lighting, because the fibre and the surface reflectance differ. Where a brand needs shell and print to match, we specify a tone-on-tone print and accept a slight tonal difference, or we move the logo to a woven label where the colour is controlled separately.
| Element | Tolerance we work to | How it is checked |
|---|---|---|
| Dyed shell colour | ≈1.5 ΔE against approved lab dip | Spectrophotometer plus D65 / TL84 light box against the retained master |
| Screen-print colour | ≈2 ΔE against approved ink drawdown | Drawdown comparison on the same shell, not on paper |
| Print position | ±3 mm from the placement template | Template overlay on 5 pieces per carton at final inspection |
| Panel dimension | ±3 mm on body width and height | Measured flat, relaxed, 24 hours after sewing |
| Finished bag weight | ±5% against the approved sample | Batch weighing, 10 pieces per lot |
Load, Wear and the Washing Question
A drawstring bag is a low-cost product that is used hard, and the failure pattern is predictable. Three loads dominate: a wet gym kit at 5–8 kg, a school bag at 4–6 kg carried daily for a year, and a laundry load at 8–12 kg lifted by one cord. Each stresses a different part of the bag.
Wet kit stresses the shell coating and the seam. A 210D shell with a light PU back-coating will hold a damp towel for a few hours without wicking; an uncoated 190T shell will pass moisture through the seam within an hour. If the product is sold for swim or gym use, specify a coated shell or a mesh body with a solid base, and seal the base seam with binding rather than a plain overlock.
Daily school use stresses the eyelets and the cord. The cord abrades against the eyelet every time the bag is opened, and a painted eyelet will wear through its plating in a term, leaving a rust ring on the fabric. Brass with nickel-free plating, clinched rather than punched, is the fix, and it adds a few cents per bag.
Laundry loads stress the channel and the bartack. A 10 kg load lifted by one cord puts the full weight through one channel end, which is why every laundry-grade sack we build carries a double bartack and a 30 mm double stitch run at both ends. If the load will routinely exceed 12 kg, the right answer is a barrel bag with a webbing handle, not a drawstring sack — and we will say so rather than quote a sack that will fail.
Washing: a 210D–600D polyester sack survives 30 machine washes at 40 °C with a screen print intact if the print is properly cured; a cotton canvas sack shrinks 3–5% on the first wash, which has to be allowed for in the cut dimension if the finished size is a contractual number. We state the shrinkage allowance on the spec sheet so the buyer is not surprised by a 45 cm bag arriving at 43 cm.
Quality Control: The Inspection Plan and the Tests Behind It
Every order runs to a written inspection plan agreed before production, and the plan is built around the components that actually fail rather than around a generic checklist. The ten checks below are what we run on a standard drawstring bag program; heavier or printed programs add checks rather than replace them.
| # | Check | Method / instrument | Accept criteria |
|---|---|---|---|
| 1 | Incoming shell fabric | GSM cutter, width measure, shade against master, AZO screening declaration | GSM ±5%, width ±2 cm, shade within tolerance, declaration on file |
| 2 | Cutting accuracy | Panel measurement against the pattern, grain direction check | ±3 mm, no cross-grain panels |
| 3 | Channel construction | Casing width gauge, stitch density count, skipped-stitch inspection | 20 mm ±1 mm, 8–10 SPI, zero skipped stitches |
| 4 | Eyelet clinch | Tensile pull to 150 N on a sample of 5 per lot | No tear-out, no fabric distortion beyond 2 mm |
| 5 | Bartack strength | Tensile pull to 200 N at both channel ends | Stitch intact, no channel opening |
| 6 | Drawstring function | 500 open-close cycles, loaded at rated weight | Smooth operation, no cord fray, no channel wear |
| 7 | Cord lock | 5,000 toggle cycles | Holds under 10 kg static load after cycling |
| 8 | Print durability | AATCC 8 crock dry and wet, 3 home washes at 40 °C, tape adhesion | Crock grade 4 or better, no lift or cracking after washes |
| 9 | Dimension and capacity | Measured flat and filled, volume by displacement | Dimension ±3%, capacity ±5% against the approved sample |
| 10 | Metal detection, count, packing | Needle and metal detector pass, piece count per carton, carton drop test | Zero metal fragments, exact count, carton intact after drop |
Final random inspection runs to AQL 2.5 for major defects and 4.0 for minor defects, on a general inspection level II sample size. Major defects in this category are: a torn or split channel, a missing or torn eyelet, a cord that will not pass through the channel, print that is more than 3 mm off placement or visibly wrong in colour, and a wrong size or wrong colourway in the carton. Minor defects are loose threads, minor print specking, uneven topstitch and slight shade variation within a carton. We photograph the inspection and send the report with the pre-shipment sample photographs, so the buyer sees the same pieces we see.
MOQ, Sampling and the Production Calendar
Drawstring bags are a fast product to develop and a slow product to ship, and buyers are usually surprised by which of the two dominates the calendar. Sampling is quick because the pattern is simple; production is not, because the shell fabric, the cord and the print screens are all outside processes.
| Stage | Duration | What has to be locked before it starts |
|---|---|---|
| Specification and artwork lock | 1–3 days | Structure, shell, size, cord, print method, colour references |
| Sampling | 6–10 working days | Confirmed spec plus print-ready vector artwork |
| Sample approval and deposit | 3–5 days | Written approval on the physical sample, not a photo |
| Bulk fabric, cord and screen booking | 7–15 days, runs in parallel | Approved lab dip, cord colour, screen count |
| Mass production | 35–50 days | Materials in house, print screens ready |
| Final inspection and reporting | 1–2 days | Production complete, packing list confirmed |
| Documentation and shipping booking | 3–5 days | Invoice, packing list, certificate of origin, booking confirmation |
The commercial threshold is 500 pieces per style, with up to three colourways and two branding layouts inside that 500. Below 500 the unit cost stops reflecting material and starts reflecting setup, cutting and sampling time, which is why we quote 500 as the floor rather than as a negotiation position. Programs that book two quarters ahead are routine; the component that moves a drawstring bag delivery is almost never sewing capacity, it is the fabric dye lot and the print screens.
Cost Drivers: Where the Money Actually Goes
Buyers comparing quotes for what looks like the same bag are usually comparing two different specifications. The table below is the cost structure of a standard 210D printed cinch sack at 5,000 pieces, as a share of FOB, and it shows why a 20% price difference between two quotes almost always traces to shell weight or print method rather than to factory efficiency.
| Cost driver | Share of FOB | What moves it |
|---|---|---|
| Shell fabric | 30–40% | Weight and fibre: 190T to 600D is a 60% swing on this line alone |
| Cutting and sewing labour | 20–25% | Structure: a boxed-base backpack takes roughly twice the sewing time of a flat sack |
| Cord, eyelets and cord lock | 8–12% | Cord construction and eyelet grade; a metal toggle adds 3–4% |
| Printing | 10–18% | Colour count and method: one spot colour versus full-colour transfer is roughly a 1.0 : 1.8 ratio |
| Packaging | 5–8% | Poly bag versus retail box; a printed box can add 8–10% at low volume |
| Overheads, QC and margin | 15–20% | Inspection level, documentation, payment terms |
There are three honest ways to hit a target price: reduce the shell weight, reduce the number of print colours, or simplify the structure. There is one dishonest way, which is to keep the specification on paper and substitute the shell in production. We do not do that, and we put the shell weight and the mill reference on the spec sheet so that a buyer can verify it at inspection.
Compliance and Claims: What Can Be Documented
Drawstring bags sit in the promotional and textile-article space, which is now audited more closely than it was five years ago. What we can supply with an order is documentation, not assurances.
What we can document: fabric composition and weight; coating type and whether the DWR is PFAS-free; AZO-free and formaldehyde-free declarations for dyed shell fabric from the mill; phthalate-free declarations for PVC-containing components and print inks; heavy-metal screening on printed and coated parts; nickel-free plating declaration for eyelets and toggles; GRS transaction certificates for recycled polyester where the order is placed against a certified mill lot; and the test reports behind the inspection table above, including crock and wash results for the print.
What we cannot issue: a “biodegradable” or “compostable” claim on a polyester or RPET shell, because neither is; an “eco-friendly” statement as a blanket property, because it is not a measurable specification and we will not print it on a bag; an OEKO-TEX certificate in our own name, because the certificate belongs to the mill and the specific fabric lot; and any REACH, Prop 65 or CPSIA compliance statement for a market we have not tested the specific materials against. Where a brand needs a claim for a retail compliance review, tell us the market at quotation stage and we will quote the test rather than imply the result.
Six Failure Points We Design Out
Across the drawstring programs we run, the same six defects recur across the industry, and each one has a design answer that costs less than the returns it prevents.
- Channel end splitting. The cord pulls through the end of the casing. Fixed with a 12–16 mm bartack plus a double stitch run at both ends, and by leaving 8 mm of channel beyond the eyelet rather than terminating the seam at the eyelet.
- Eyelet tear-out. The eyelet pulls through a thin shell. Fixed with a reinforcement patch or a double layer of shell behind the eyelet on anything below 420D, and by clinching rather than punching.
- Cord fraying at the lock. The cord end unravels and jams the toggle. Fixed with a heat-sealed and dipped end, or an aglet, and by specifying a braided rather than a twisted cord.
- Print cracking at the fold. Artwork crosses the fold line and the ink cracks in the wash. Fixed by keeping artwork 10 mm clear of the fold and the channel, and by using a stretch-capable ink on thin shells.
- Shoulder cut on backpacks. A 4 mm cord carrying 8 kg cuts into the shoulder. Fixed with webbing loops at the shoulder points as a minimum, or foam-filled pads above 6 kg.
- Shrinkage surprise on canvas. A 45 cm canvas sack arrives at 43 cm after the first wash. Fixed by cutting to a shrinkage allowance and stating the allowance on the spec sheet.
Customization: What We Actually Change on a 500-Piece Order
The list below is what a 500-piece order can change without new tooling. Anything outside it is possible but usually implies a die, a mould or a minimum fabric buy, and we will say which before quoting.
| Element | Options at 500 pcs | Notes |
|---|---|---|
| Structure | DS-01 to DS-05, or a modification of an existing pattern | A new pattern from scratch is possible but adds a sample round |
| Shell | Any of the nine shells in the material table | Stock colours are faster; a custom dye lot adds 7–15 days |
| Size | Any size within the matrix, or a custom dimension | Custom size needs a new cutting pattern but no tooling |
| Cord | PP, braided polyester, cotton, reflective, elastic, webbing | Colour matched to the shell or contrasted |
| Hardware | Eyelet finish, cord lock type, cord ends, webbing loops, strap pads | Metal toggle and metal aglets are the two premium upgrades buyers ask for most |
| Pockets | Internal zip pocket, slip pocket, shoe compartment, name-tag panel | Adds 3–6% at 500; the zip pocket is the most requested addition |
| Branding | Any of the seven methods, plus woven main label, care label, hangtag | Care label content is checked against the shell and the print method |
| Packaging | Poly bag, printed retail box, hangtag, barcode, carton marks | Carton marks printed to your specification, not our template |
Packaging, Cartons and the Freight Number Buyers Forget
Drawstring bags are cheap to make and expensive to move relative to their value, so packed volume is a commercial specification. A flat cinch sack packs down to almost nothing, which is precisely why it is the promotional favourite: 500 flat sacks at 210D typically fit into two or three master cartons, while the same 500 in printed retail boxes need eight to twelve. On a product with a low FOB, that difference can be a larger share of landed cost than the fabric choice.
We quote the carton count, the carton dimensions and the gross weight with every order, and we will re-quote the packing if a buyer’s target landed cost depends on it. Retail-ready packing, DC-ready packing with GS1 carton labels, and pallet configurations to a specific height are all available; the constraint is usually the box tool, not the packing labour.
Why Brands Build Drawstring Programs With Us
Most of our drawstring programs sit inside a larger bag range, and the reason is operational rather than commercial. A drawstring sack uses the same cutting room, the same lockstitch and walking-foot machines, the same bonded thread, the same cord and eyelet vendors and the same print department as a backpack, a tote or a duffel, so a brand already running a bag program adds a drawstring line without adding a second supply chain, a second colour approval cycle or a second carton specification.
The technical capability that matters here is dimension-critical small-panel work: a drawstring sack is essentially two or three panels and a channel, and a 3 mm error at the channel width becomes a cord that will not run freely. That is the same discipline we apply to packing cubes and tactical bags, where a panel that is 2 mm out is a functional defect rather than a cosmetic one.
Brands that extend from drawstring sacks into canvas shopping bags, laundry bags, shoe bags, beach bags or yoga mat bags build those on the same cells and the same print screens. Buyers adding wet-weather or swim products usually pair the sack with our dry bags and waterproof bags, and buyers building a full carry range add backpacks and duffel bags on the same program. For the wider OEM/ODM picture, see our custom bag manufacturer hub.
Frequently Asked Questions
Start a Drawstring Bag Program
Send the structure you need (or a reference product), the size and shell you have in mind, the load the bag has to carry, the print method and artwork, the packaging format, the quantity and the date you need the goods in hand. We will come back within two working days with a construction recommendation, a size and shell specification, a print method recommendation with a placement template, a carton and packed-volume estimate, and a quotation.
What we need to quote accurately: structure, size, shell and weight, cord and cord-lock grade, carry system, print method and colour count, artwork placement, packaging, quantity and delivery window. What we will tell you honestly: where a requested shell will not hold the load, where a print method will not survive the wash cycle the product is sold for, where a canvas size will shrink out of tolerance, and where a cheaper structure will cost more in returns over the life of the program.
Request a Drawstring Bag Quote
500 pcs MOQ · 6–10 day sampling · 35–50 day production · AQL 2.5 major / 4.0 minor · OEM/ODM since 2014
Related Manufacturing Pages
- Custom Bag Manufacturer — OEM/ODM Hub
- Custom Canvas Shopping Bag Manufacturer
- Custom Laundry Bag Manufacturer
- Custom Shoe Bag Manufacturer
- Custom Beach Bag Manufacturer
- Custom Yoga Mat Bag Manufacturer
- Custom Packing Cubes Manufacturer
- Custom Backpack Manufacturer
- Custom Duffel Bag Manufacturer
- Custom Dry Bag Manufacturer
- Custom Waterproof Bag Manufacturer
- Custom Tactical Bag Manufacturer
- Custom Tote Bag Manufacturing Guide
- Custom Branding for Promotional Bags — Guide