A bag manufacturer established in 2014, with our founder working in the bag trade since 2004. We build private-label everyday-carry pouches, MOLLE utility pouches, admin pouches, belt pouches, tool rolls, magazine-style organizers and hook-and-loop EDC inserts for tactical and outdoor brands, knife and tool brands, first-responder suppliers, promotional distributors and marketplace sellers — in 1000D and 500D nylon, X-Pac laminate, waxed canvas, 600D recycled polyester and Hypalon.
Short answer for buyers: an EDC pouch is an attachment product before it is a storage product. The specification that decides whether it sells is the mounting interface — a 38 mm or 50 mm belt loop, a PALS/MOLLE webbing panel with 25 mm rows on 25 mm vertical spacing, a laser-cut laminate grid, a Tek-Lok style clip or a hook-and-loop panel — because a pouch that does not lock onto the platform the customer already owns is returned regardless of how well it is sewn. We build EDC pouches at 500 pieces per style, sample them in 6–10 working days, run mass production 35–50 days after sample approval, and inspect to AQL 2.5 major / 4.0 minor. Mounting, retention and access are confirmed on a physical carrier before a pattern is released, not on a drawing.
What an EDC Pouch Has to Solve That a Pencil Case Does Not
An everyday-carry pouch looks like a small zippered bag on a spec sheet. In the field it is a piece of equipment that is worn, clipped, dragged and opened under stress, and almost every return in this category traces back to one of four constraints being treated as a detail rather than as the design brief.
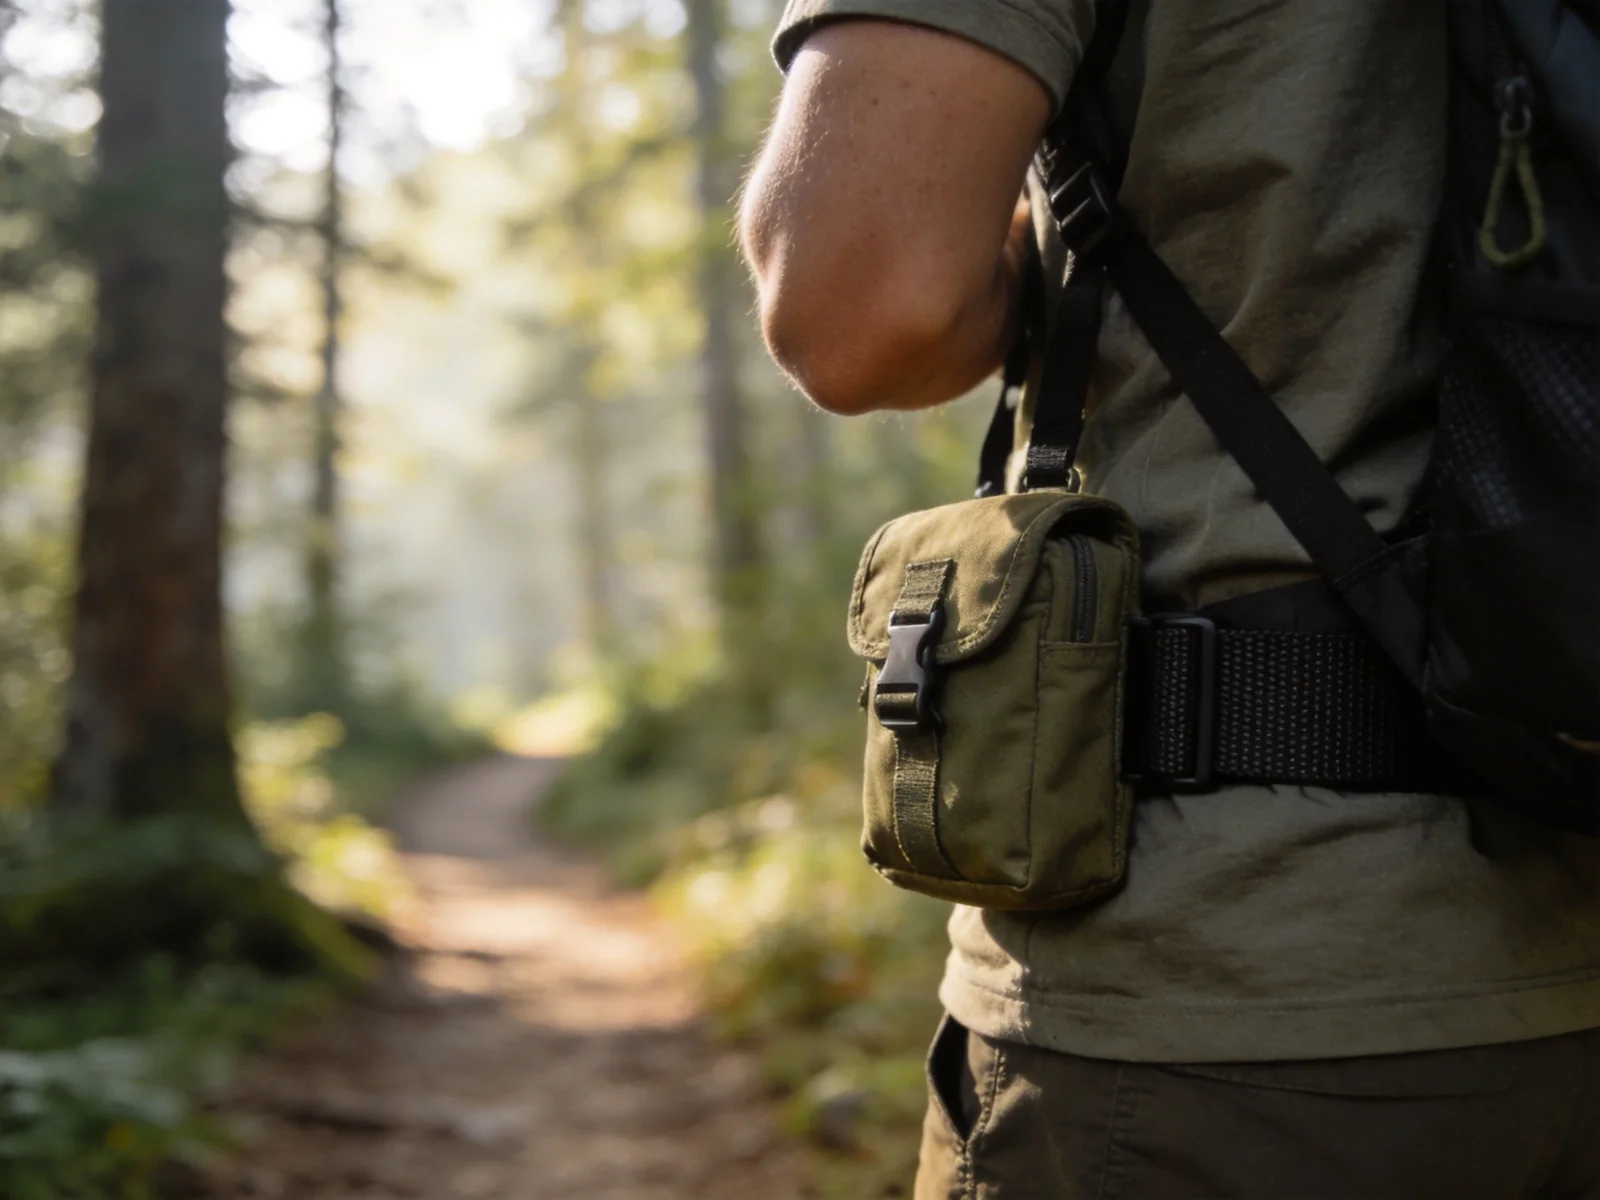
Constraint one: it must lock onto a platform that already exists. The customer already owns a belt, a backpack with PALS webbing, a plate carrier, a range bag or a camera harness. A pouch is an accessory to that system, and the interface is the first thing a reviewer tests. A belt loop cut 2 mm tight will not pass a duty belt; a MOLLE strap spaced 30 mm instead of 25 mm will thread two rows and skip the third; a laser-cut grid with the wrong slot pitch will accept the customer’s MALICE clip but not the next one. Interface dimensions are not negotiable design choices — they are inherited standards, and we cut them from the standard rather than from the rendering.
Constraint two: it is opened one-handed, often in the dark, often with gloves on. An EDC pouch holds keys, a folding knife, a light, a multi-tool, a tourniquet, a phone or a passport — items the user reaches for while the other hand is holding something else. That rules out small pullers, tight zips, deep lids that need two hands to hold open, and closures that need a nail to start. Zipper pulls get paracord extensions, the lid gets a limiter strap or a full clamshell hinge, and the opening is sized so a gloved finger can hook it. This single constraint changes more patterns than any aesthetic decision in the category.
Constraint three: it lives against abrasion and grit. A pouch rides on a belt at hip height, on a pack strap, or in the bottom of a range bag where it meets brass, tools and gravel. The wear points are predictable: the bottom corners, the belt-loop bar-tacks, the zip tape at the curve, and the webbing edges. We reinforce exactly those four places, and we specify a heavier shell on the models that are sold into range and field use than on the models sold as office or travel organizers.
Constraint four: it must not rattle, and it must not lose contents. A pouch that clicks and shifts when the wearer walks is a pouch that gets left at home. Internal retention — elastic loops, loop-pile panels, slip pockets, a divider — is what converts a bag into an organizer, and it is also what reviewers photograph. On the other side of the same coin, retention has to be strong enough that a knife does not slide out when the pouch is inverted, which is why elastic tension and loop coverage are specified in millimetres rather than described as “firm”.
The Buying Landscape: Who Orders EDC Pouches and What Each Channel Needs
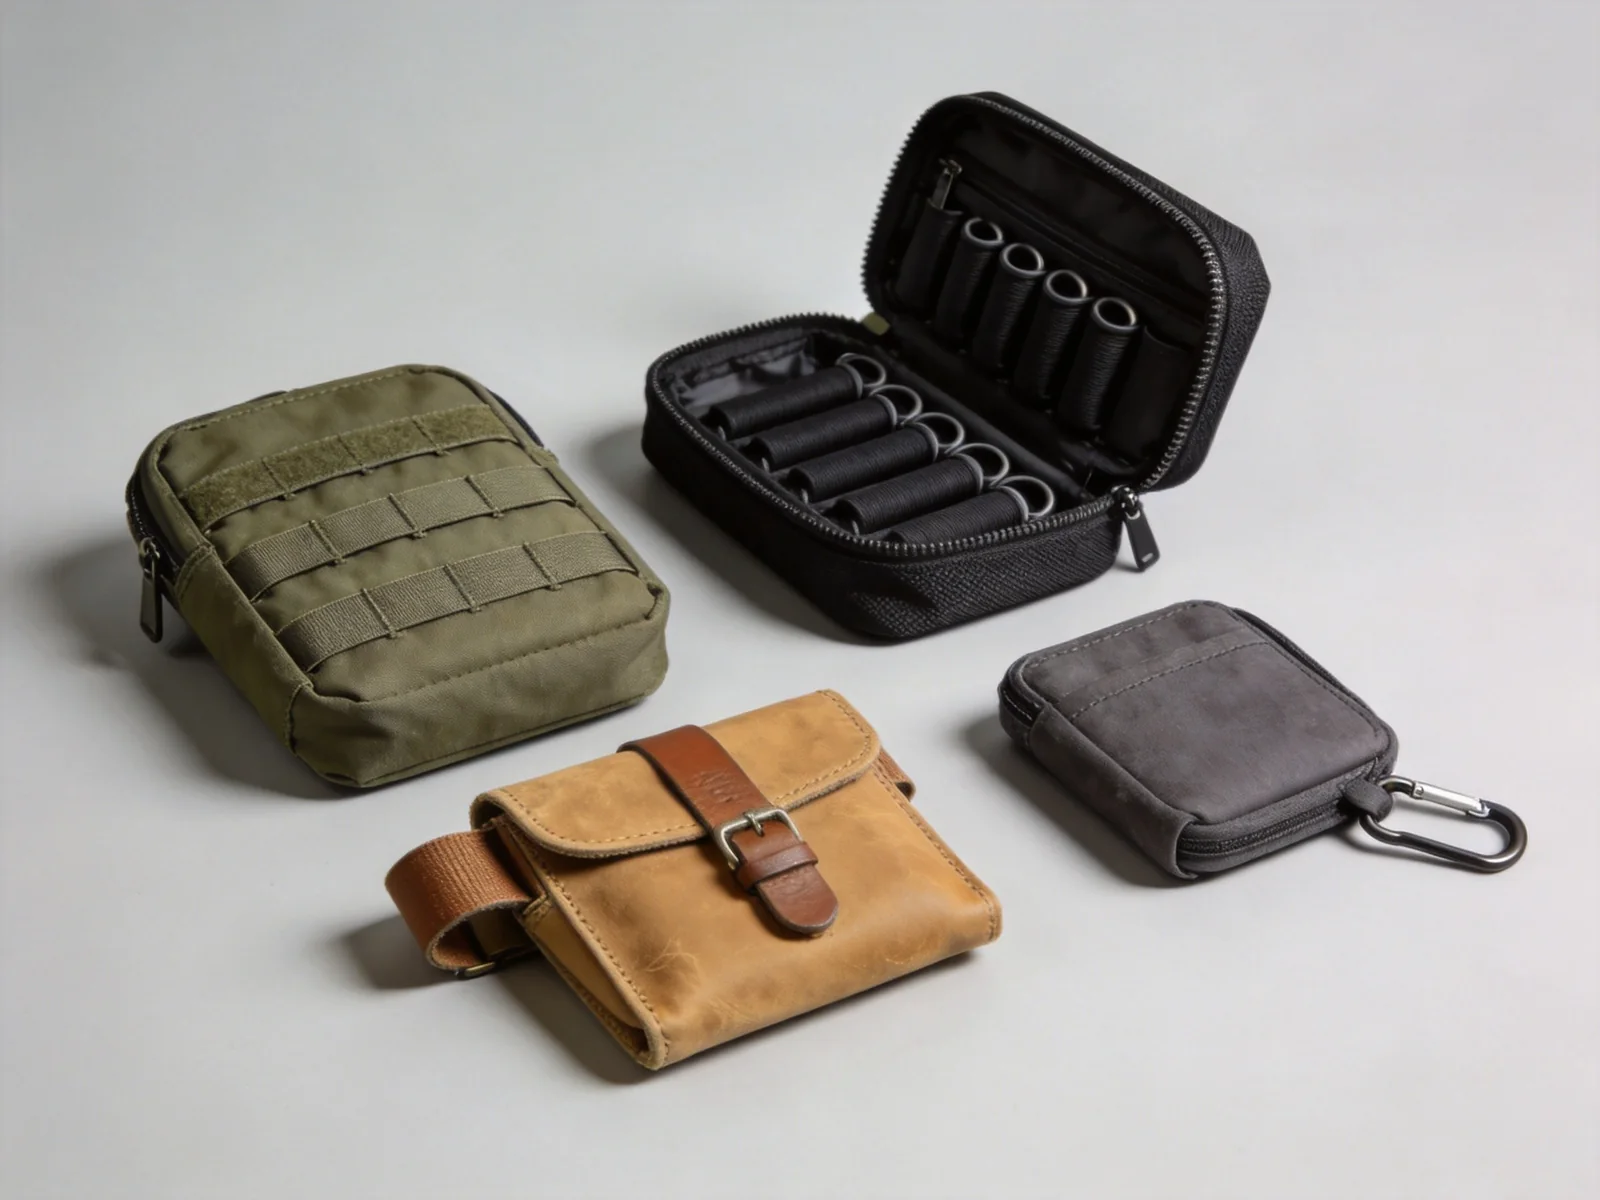
Pouches arrive from six kinds of buyer, and the brief changes completely between them. A tactical brand developing a 12-SKU modular family and a promotional distributor ordering 20,000 printed pouches for a trade-show giveaway are not buying the same product, even when both call it a utility pouch.
| Channel | Typical order | Construction that wins | Non-negotiable requirement |
|---|---|---|---|
| Tactical and outdoor brands | 1,000–10,000 pcs per colourway, 2–3 drops a year | 500D or 1000D nylon MOLLE pouch with PALS rows, bar-tacked stress points, YKK zip | Interface dimensions to standard; colour consistency across a modular family; abrasion test data |
| Knife, tool and flashlight brands | 500–5,000 pcs, bundle SKUs | Belt pouch or fold-over flap pouch with elastic loops sized to the tool | Retention tuned to the exact product dimensions; no rattle; packaging that fits a retail peg or box |
| First-responder and uniform suppliers | 2,000–20,000 pcs, contract cycles | Duty-belt pouch with 50 mm loop, glove-friendly closure, high-visibility options | Colour and hardware specified to a uniform standard; repeatable sizes across reorders; documentation pack |
| EDC and travel accessory brands | 500–5,000 pcs, seasonal | X-Pac or waxed canvas organizer with hook-and-loop panel and carabiner | Premium hand feel; clean stitching visible at retail; photography-ready interior |
| Promotional and gifting distributors | 5,000–50,000 pcs | 210D–420D polyester zip pouch, single-colour print | Unit cost at volume; print area; survives compression packing and bulk freight |
| Marketplace and DTC sellers | 500–3,000 pcs per SKU, frequent reorders | Compact belt or carabiner pouch in 600D RPET, four to six colours | Consistent size and colour between batches; barcode and carton marks; short replenishment cycle |
The order ranges above are what we see in practice rather than a policy. The commercial threshold is 500 pieces per style, and inside that 500 a buyer can mix up to three colourways and two branding layouts, which is usually enough to test a new colour direction or a new channel without committing to a full run of one variant.
Mounting Systems: The Interface That Decides the Pattern
This is the section most suppliers skip and most returns come from. Every pouch we quote is defined first by its interface, then by its volume, then by its closure. The table below is the working list of interfaces we tool for, with the dimensions we hold in production.
| Interface | Standard dimensions | Best for | What goes wrong when it is approximate |
|---|---|---|---|
| Fixed belt loop, single | 38 mm or 50 mm clear opening; loop height 55–70 mm | Duty belts, work belts, casual EDC | Loop cut tight will not pass a 50 mm duty belt with a buckle; loop cut loose lets the pouch rotate forward |
| Double / wrap-around belt loop | Two loops at 38 mm, 70 mm apart | Heavier pouches, tool pouches | Spacing too narrow makes the pouch ride up when the wearer sits |
| PALS / MOLLE webbing panel | 25 mm webbing, rows on 25 mm vertical pitch, stitch channels every 38 mm | Backpacks, plate carriers, range bags | Pitch off by 3–5 mm means the strap threads two rows and skips the third, so the pouch swings |
| Laser-cut laminate grid | Slot pitch matched to the buyer’s clip system; slot 3–4 mm wide | Lightweight tactical, minimalist brands | Slot width too narrow rejects a metal clip; too wide tears the laminate at the slot end |
| Tek-Lok style clip / paddle | Clip body 50 mm, belt range 40–57 mm | Holsters, magazine pouches, quick on-off | Clip moulding tolerance and screw torque decide whether it stays on during a draw |
| Hook-and-loop panel | Loop pile field 50 × 75 mm or 75 × 100 mm, hook on the carrier | Bag inserts, admin panels, vehicle organizers | Field too small lets the insert peel off when the bag is opened one-handed |
| Strap mount (One-Wrap style) | 25 mm or 38 mm webbing with hook-and-loop closure | Backpack straps, bike frames, camera harnesses | Closure overlap under 40 mm releases under load |
| Carabiner / D-ring hang | 25 mm webbing tab with a metal D-ring or a gate carabiner | Key and card organizers, travel pouches | Tab not bar-tacked through the shell tears out at the first snag |
| Drop-leg platform | Two thigh straps 50 mm, adjustable 480–700 mm | Field and range use | Non-slip backing omitted, so the platform slides down the leg when walking |
Two rules come out of that table. First, an interface is a standard, not a styling cue: we keep a dimensioned drawing for each one and cut from it, and when a buyer’s reference sample measures differently from the standard we ask which one the customer’s existing gear follows. Second, the interface decides the pattern layout. A 50 mm belt loop needs a reinforced back panel and moves the zip to the top or the front; a PALS panel needs the webbing sewn through to a stiffener so the rows do not sag between stitches; a hook-and-loop back needs a flat, non-stretch panel behind the loop pile or the field ripples and stops holding.
Sizing: Volume, Contents and the Numbers That Decide Fit
Pouch sizing fails quietly — the product photographs well and then a customer cannot close it over a loaded magazine, or the phone does not fit the front pocket. We size from the contents list, then check the packed volume, then confirm the external dimensions against the interface.
| Format | External size (W × H × D) | Packed volume | Typical contents | Interface we usually pair it with |
|---|---|---|---|---|
| Compact key and card pouch | 110 × 75 × 30 mm | ≈ 0.25 L | Keys, two cards, a folded note, a small light | Carabiner / D-ring tab |
| Small belt utility pouch | 120 × 90 × 45 mm | ≈ 0.5 L | Folding knife, pen, lighter, small multi-tool | 38 mm belt loop |
| Standard EDC utility pouch | 150 × 110 × 55 mm | ≈ 0.9 L | Multi-tool, light, notebook, cable, keys | 38 mm loop or 2-row PALS |
| Admin pouch | 200 × 150 × 60 mm | ≈ 1.8 L | Documents, pens, cables, power bank, gloves | 3–4 row PALS or hook-and-loop panel |
| Large utility / tool pouch | 250 × 170 × 90 mm | ≈ 3.8 L | Tools, tape, ties, first-line repair kit | Double 50 mm loops or 4-row PALS |
| Magazine-style pouch | 90 × 150 × 40 mm | ≈ 0.5 L | One magazine or a comparable cylindrical tool | Tek-Lok clip or 2-row PALS |
| Tool roll, open flat | 480 × 280 mm open, 120 mm rolled | ≈ 1.2 L rolled | Six to twelve hand tools in elastic loops | Wrapped strap or carabiner |
| Hook-and-loop bag insert | 180 × 120 × 40 mm | ≈ 0.8 L | Admin items inside a backpack or sling | Loop field on the back panel |
Three practical rules come out of that table. First, the depth figure is the one buyers underestimate: a pouch listed at 55 mm depth loses 8–10 mm to the zip tape, binding and back stiffener, so the usable internal depth is closer to 45 mm, and a hard item that measures 50 mm will not close. Second, a MOLLE pouch needs 15–20 mm of clear space behind the back panel for the straps to thread, which is why the external depth is not the same as the depth it occupies on a pack. Third, decide early whether the pouch is a single-layer or a two-compartment build: adding a front pocket to a 0.9 L pouch changes the panel count by two and the labour by roughly a third, and it usually pushes the format into the next size bracket.
Construction Types: Ten Ways to Build an EDC Pouch
These are the ten constructions in current production. Most buyers start from one of them and change two or three details — the interface, the internal retention, the closure — rather than developing a new pattern, which keeps sampling to one round and tooling to zero.
| Code | Construction | Best for | Typical FOB positioning |
|---|---|---|---|
| EP-01 | Flat zip pouch, single compartment, bound seams | Promotional, travel organizers, giveaways | Lowest cost; lightest; no structure |
| EP-02 | Boxed utility pouch, YKK zip across the top, belt loop on the back | Knife and tool brands, everyday carry | Entry to mid; the volume workhorse |
| EP-03 | MOLLE utility pouch with PALS rows on the back, bar-tacked | Tactical and outdoor brands, range use | Mid; webbing rows add labour |
| EP-04 | Clamshell admin pouch, full zip, internal elastic loops and slip pockets | EDC organizers, first-responder admin | Mid to high; interior work is hand time |
| EP-05 | Fold-over flap pouch with buckle or hook-and-loop closure | Duty belts, tool pouches, glove-friendly use | Mid; no zip component, more panel shaping |
| EP-06 | Horizontal magazine-style pouch with adjustable elastic retention | Tactical, utility, cylindrical tool carry | Mid; retention tuning per item |
| EP-07 | Laser-cut laminate pouch, welded or bound edges, low profile | Minimalist tactical, cycling, premium EDC | High material cost, lower labour |
| EP-08 | Tool roll, open flat with elastic loops and a wrap strap | Tool brands, bike and field kits | Mid; large panel, many loop operations |
| EP-09 | Hook-and-loop bag insert with loop back panel and pull tab | Backpack and sling brands, camera bags | Mid; flat pattern, simple build |
| EP-10 | Drop-leg or thigh platform pouch with two adjustable straps | Field, range, airsoft, film crews | High; harness and non-slip backing |
The single most consequential choice in that table is zip versus flap. A zip gives a low profile, keeps grit out and reads as a modern product, but it adds a zip, two ends, a puller and a binding operation, and the zip end at the curve is the most likely failure point in the whole pouch. A flap with a buckle or hook-and-loop is faster to open with gloves, cheaper in components and impossible to jam, but it is bulkier and less water-resistant. Buyers selling into duty and field use usually run flaps; buyers selling into EDC and travel usually run zips, and a brand with a full range often runs both on the same body.
Material Selection: Seven Fabrics and What Each One Is Actually For
Fabric choice in this category is decided by three things at once — the abrasion level the product will meet, the hand feel the brand wants at retail, and whether the fabric can carry the branding method already designed. A 1000D nylon that survives a gravel range floor feels like luggage in an office context; a 210D ripstop that photographs beautifully will not survive a belt clip for a season.
| Fabric | Weight | Strengths | Limitations | Use it for |
|---|---|---|---|---|
| 1000D nylon (Cordura-type) | ≈ 350 g/m² | Highest abrasion resistance, holds shape, takes PU backing and DWR | Heavy and stiff; adds 40–60 g per pouch; slower to sew | Range, field and duty pouches, tool pouches |
| 500D nylon | ≈ 240 g/m² | Good abrasion at 30% less weight, softer hand, better drape | Less resistant at the bottom corners; needs reinforcement patches | Modular tactical families, outdoor EDC, the default shell |
| 210D ripstop nylon | ≈ 110 g/m² | Light, packable, good print base, low cost | Low abrasion resistance; needs binding on all edges | Travel organizers, promotional pouches, linings |
| X-Pac style laminate (VX21 class) | ≈ 200 g/m² | Waterproof, dimensionally stable, no fraying, technical look | Higher material cost; cannot be re-sewn without sealing; needle holes leak | Premium EDC, cycling, minimalist tactical |
| 18oz waxed canvas | ≈ 610 g/m² | Heritage hand, ages well, natural water resistance, excellent for leather trim | Heavy; wax transfers in heat; not washable; creases at folds | Heritage and lifestyle EDC, gift and retail programs |
| 600D recycled polyester (RPET) | ≈ 230 g/m² | Durable, colour-fast, prints by screen or heat transfer, recycled-content story | Synthetic hand; needs a backing for structure | Volume retail, marketplace SKUs, corporate programs |
| Hypalon / TPU laminate sheet | ≈ 500 g/m² | Laser-cuttable, no fraying, high abrasion, holds hardware | Not sewable at high density; limited colour range | Laser-cut grids, reinforced mounting points, trim |
Three material notes that come up in almost every development conversation. First, PU coating and DWR are the two finishes that decide whether the pouch beads water, and the industry is moving to C0 (PFAS-free) DWR because of EU and US state restrictions on fluorinated chemistry — we specify C0 DWR as the default on new developments and can quote a fluorinated finish only where a buyer explicitly requires it and takes the compliance position. Second, recycled polyester is now the standard ask for volume programs in Europe and North America, and buyers increasingly want a GRS transaction certificate from the mill rather than a generic “eco” claim; we source GRS-certified 600D RPET and pass on the mill documentation for the specific order. Third, thread matters more than most buyers expect: we sew pouches with bonded nylon in T70 (#69) for shells and T90 (#92) at stress points, at 7–9 stitches per inch, because an unbonded polyester thread at 12 stitches per inch cuts the coating and starts the seam failure it was meant to prevent.
Hardware and Components: Where the Specification Is Won or Lost
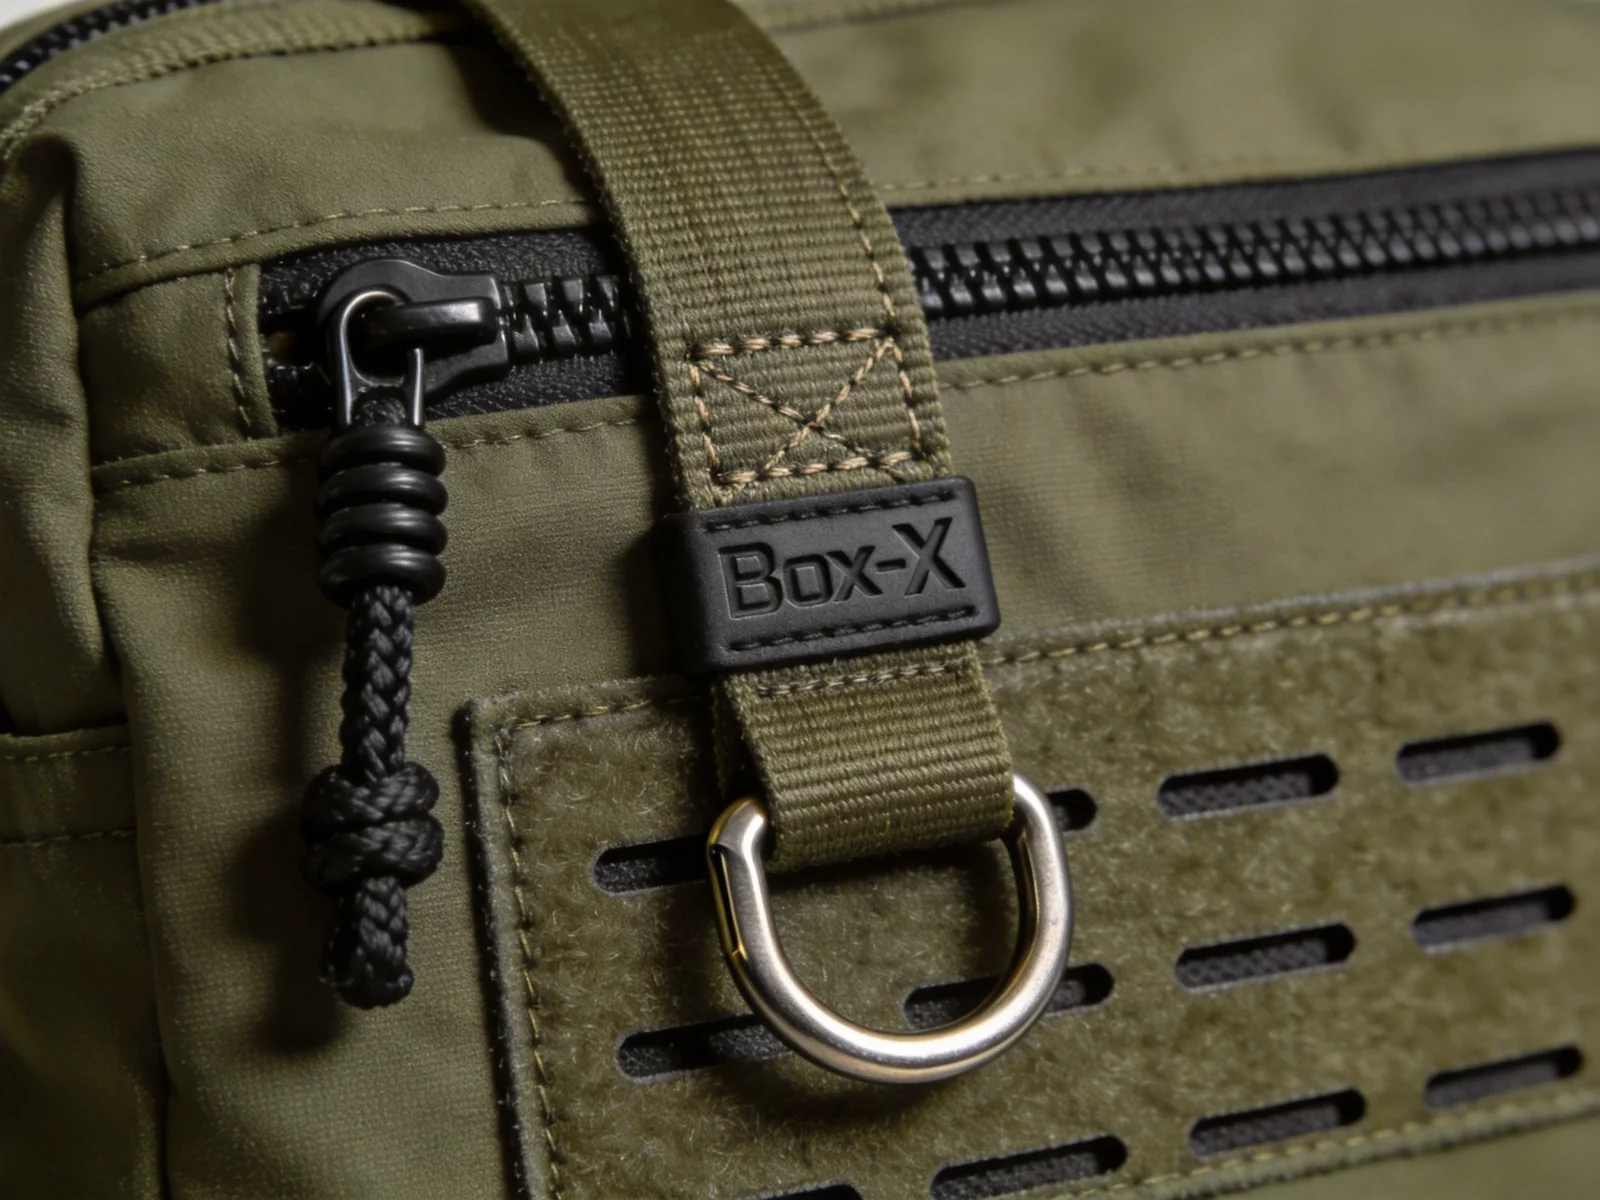
A pouch carries more hardware per litre than any other bag category, and each component is a specification with a tolerance. The list below is what we hold as standard options; anything outside it is a development item with its own lead time.
| Component | Options we run | Why it matters |
|---|---|---|
| Zip | YKK #5 or #8 coil, reverse coil water-resistant, #10 on large tool pouches; nylon or metal slider | The zip end at the curve is the number one failure point; a #5 coil is enough for 1 L, a #8 is needed once the pouch is loaded to 3 L |
| Zip pull | Paracord 550 extension with a heat-sealed end, or a moulded pull tab | Glove and one-hand access; also the part photographers show at retail |
| Buckle | 25 mm and 38 mm side-release, Duraflex or Woojin class; metal G-hook on heritage builds | Cheap buckles crack at −10 °C; the load case is a snagged pouch, not a static one |
| D-ring / loop | 25 mm metal D-ring, polymer loop, 25 mm webbing tab | Hang points take the whole pouch weight on one stitch line, so they are bar-tacked through a reinforcement patch |
| Elastic | 20 mm, 25 mm and 38 mm knit elastic; folded and bound ends | Retention force is set by elastic width and stitch spacing; a raw-cut end unravels within weeks |
| Hook-and-loop | 25 mm and 50 mm, Velcro-brand or equivalent, hook on the insert and loop on the carrier | Peel strength and cycle life fall fast if the pile is thin; the field size decides one-handed security |
| Webbing | 25 mm and 38 mm nylon or polyester, bar-tacked at every row end | PALS rows are only as good as their stitching; an unbar-tacked row sags and the strap loosens |
| Stiffener | 1.0–1.5 mm HDPE sheet, or a bonded board in the back panel | Keeps a loaded pouch from collapsing onto the belt and makes one-handed opening possible |
Two specification habits save buyers money over a program. First, fix the hardware family at the sampling stage and keep it across the range: mixing two buckle moulds in one modular family is visible at retail and doubles the component inventory. Second, choose the zip by loaded volume rather than by price — the difference between a #5 and a #8 coil is a few cents, while the difference in warranty claims on a 3 L pouch is not.
Branding: Six Methods That Work on a Small Curved Panel
An EDC pouch offers roughly 100 × 60 mm of usable branding surface on the front panel, and the panel is curved, bound and often webbed. Methods that work on a flat tote behave differently here, and the method also decides the minimum order and the lead time.
| Method | Best substrate | Durability | Notes |
|---|---|---|---|
| Embroidery | 500D/1000D nylon, waxed canvas | Excellent | Thread count and backing decide whether the panel puckers; best on a flat front pocket, not across a zip |
| PVC or TPU patch | Any shell | Excellent | The most common tactical branding; sewn or hook-and-loop backed; adds 8–15 g and one operation |
| Laser engraving | Hypalon, laminate, anodised hardware | Excellent | No colour, no ink, no cracking; ideal for minimalist and technical brands |
| Heat transfer / silicone label | Nylon, polyester, laminate | Very good | Fine detail and small type; needs a flat area and a controlled press temperature |
| Screen print | 600D RPET, 210D polyester, canvas | Good | One to three colours; must be printed before sewing on flat panels, not on the assembled pouch |
| Woven label | Any shell | Excellent | Cheapest route to a brand mark; placement matters more than size on a small pouch |
Three practical limits. Sublimation needs a light polyester substrate and will not work on 1000D nylon or waxed canvas. A print that crosses a bar-tack or a binding will crack at that line, so artwork is placed inside the flat field. And a patch sewn through a PALS row will block that row — if the branding is on the back panel, the row count has to be reduced by one and the interface drawing updated accordingly.
Six Failure Points We Design Out
These are the defects we see most often in pouches that come back, and the countermeasure we build into the pattern rather than into the inspection.
1. The belt loop or MOLLE row tears out of the shell
The load is concentrated on two stitch lines and a thin shell. We bar-tack every webbing row end, sew the loop through a reinforcement patch of the same or heavier fabric, and box-X the belt loop where it meets the body. On 210D shells we add a stiffener so the stitch line is not taking load through a single layer.
2. The zip end splits at the curve
A zip set into a curved panel is under tension at the end, and a single row of stitching lets the tape pull out. We bind the zip end, add a second row of stitching 2 mm inside the first at the curve, and stop the slider short of the corner so the puller is not used as a lever.
3. Elastic loops go slack within a season
Knit elastic loses recovery when it is sewn under tension across a raw edge. We fold and bind the ends, set the loop length to the tool dimension minus 8–10%, and specify a heavier elastic on retention-critical builds. Where the retention must last for years, we replace elastic with a webbing and hook-and-loop strap.
4. Hook-and-loop peels off the insert
Loop pile bonded to a coated shell fails at the adhesive, not the pile. We stitch the loop field around its perimeter through a flat non-stretch panel, and we keep the field 10 mm inside the seam so the edge cannot be lifted by a thumbnail.
5. The coating cracks along a fold
PU coating on a tight fold breaks at low temperature, and the crack becomes a water path and then a tear. We radius every fold, avoid folding coated fabric on a sharp edge, and specify a C0 DWR with a coating weight matched to the fold radius rather than the heaviest available.
6. Hardware corrodes or rattles
Salt spray and sweat attack cheap plating, and a loose D-ring announces the wearer. We specify plated or anodised hardware to the buyer’s salt-spray requirement, and we set D-rings on a webbing tab that is stitched tight enough that the ring cannot slide.
Customization: What We Actually Change on a 500-Piece Order
Buyers often assume a 500-piece minimum means a stock product with a logo on it. It does not. Inside 500 pieces we change the shell, the size, the interface, the closure, the interior layout, the hardware family, the branding method and the packaging, and the sampling round is where those changes are proven.
| Element | What can change at 500 pcs | Effect on sampling |
|---|---|---|
| Shell fabric and colour | Any fabric in the table above, Pantone-matched; two-tone panel splits | One lab dip per colour, 5–7 days; no pattern change |
| Size | Any dimension, within the same construction | Pattern re-cut; usually no new sampling round if the interface is unchanged |
| Interface | Belt loop, PALS panel, laser-cut grid, clip, hook-and-loop field, strap mount | New back-panel pattern and a physical fit test on the buyer’s carrier |
| Closure | Zip (coil or reverse coil), flap with buckle, hook-and-loop flap, drawcord | Pattern change at the opening; adds one sampling round if the body shape changes |
| Interior | Elastic loops, slip pockets, divider, key leash, loop field, mesh window | Hand-time increase of 15–40%; layout drawing required |
| Hardware | Buckle family, D-ring material, zip brand and size, puller type | Component lead time only |
| Branding | Embroidery, patch, laser engraving, heat transfer, screen print, woven label | Artwork proof and a placement template per SKU |
| Packaging | Polybag, hangtag, header card, retail box, carton marks, barcode | Artwork only; adds 3–5 days to production |
The changes that most often surprise buyers are the cheap ones. A key leash costs less than a dollar and is the single most photographed interior detail in EDC reviews. A paracord zip pull costs cents and removes the most common one-star complaint about gloves. A stiffener in the back panel costs a few cents and is the difference between a pouch that stands open on the belt and one that folds shut.
Quality Control: The Inspection Plan and the Tests Behind It
Inspection on this category is not a final look-over. Pouches are small, so defects hide in the interior and at the interface, and the tests that matter are the ones that reproduce field use. Our standard plan for an EDC pouch program is below.
| Stage | What is checked | Standard / method | Sample |
|---|---|---|---|
| Incoming fabric | Weight, width, shade against lab dip, coating adhesion, DWR spray rating | In-house; AATCC 22 spray test | One roll per lot |
| Incoming hardware | Buckle function, zip smoothness, plating appearance | In-house functional check | AQL 1.0 |
| Cutting | Panel dimensions against the size sheet, grain direction, symmetry | In-house; ±2 mm on critical dimensions | First article + 5% random |
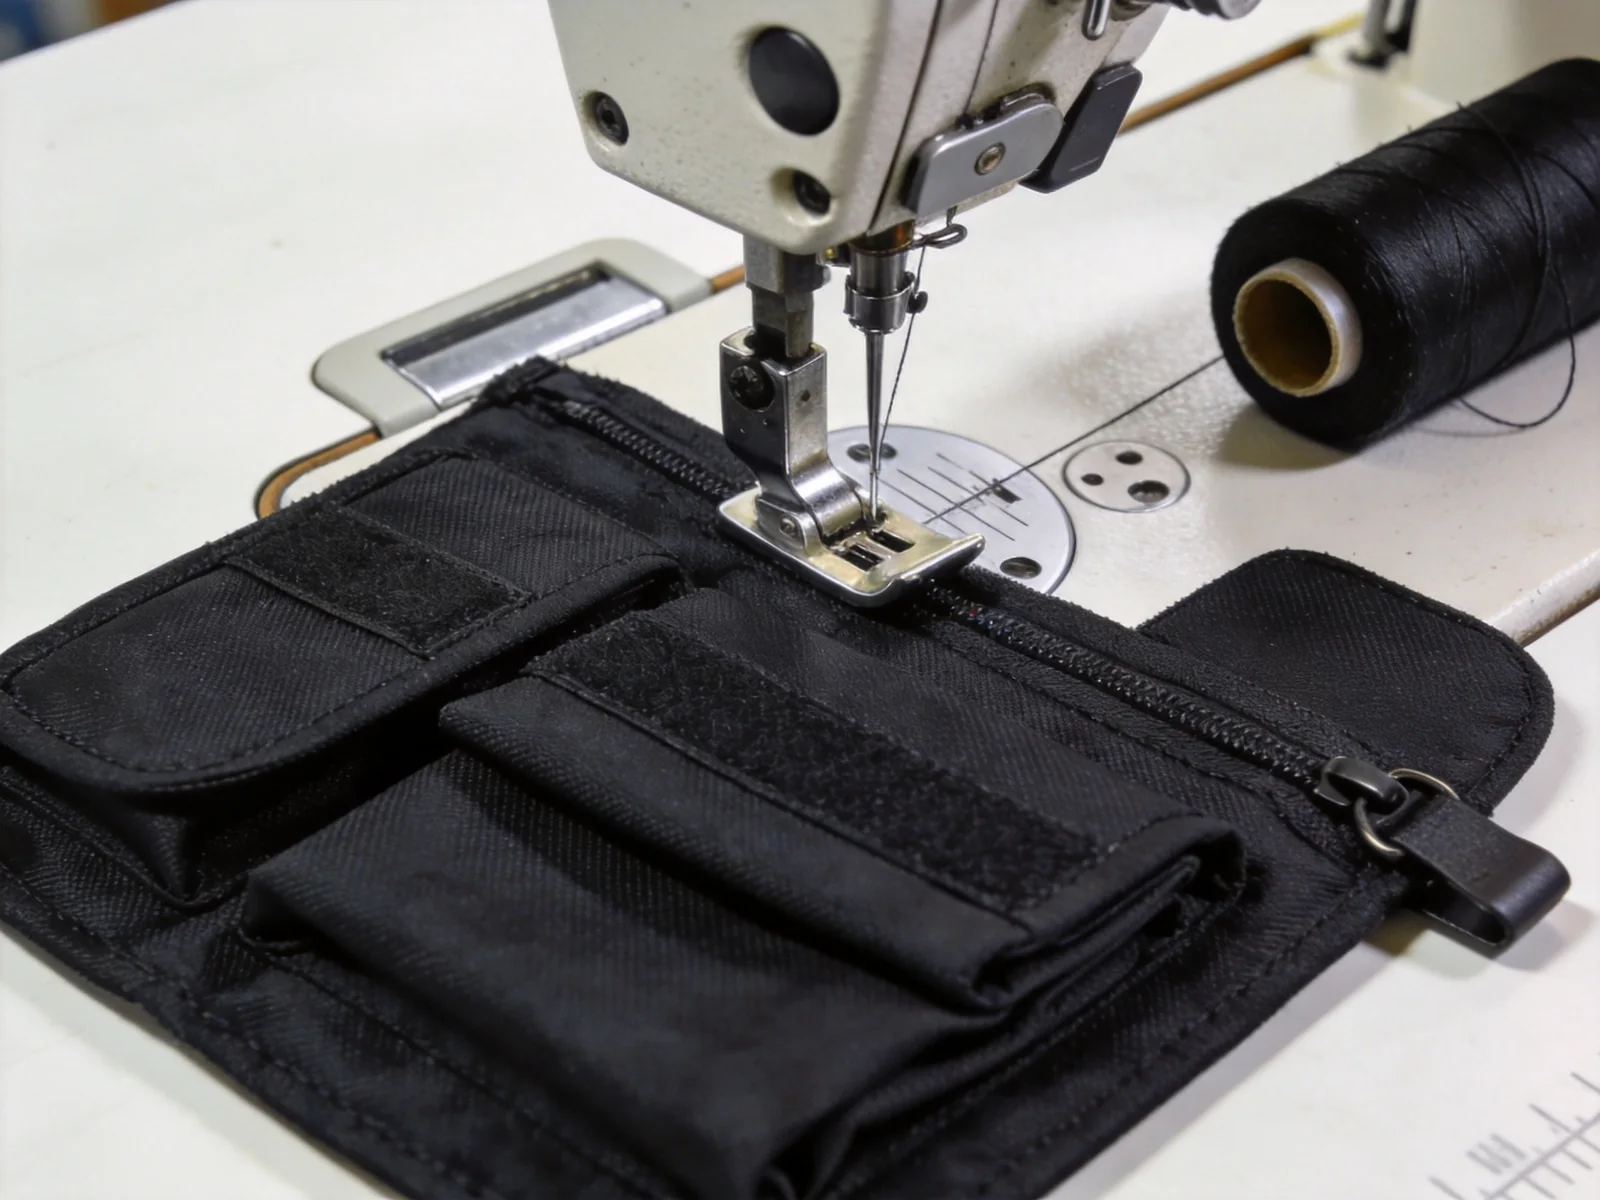
| In-line sewing | Stitch density 7–9 SPI, bar-tacks present, seam allowance, interface pitch | In-house roving check every 50 pcs | Continuous |
| Seam strength | Grab tensile at the belt loop and the zip end | ASTM D5034 equivalent, in-house tensile rig | 3 pcs per lot |
| Zip durability | Open/close cycles without skip or split | Reciprocating cycle test, 5,000 cycles | 3 pcs per lot |
| Abrasion | Bottom corner and belt-loop face | Taber CS-10 or Wyzenbeek, buyer’s cycle target | 2 pcs per lot on request |
| Colourfastness | Crocking and light | AATCC 8 and AATCC 16 | Per colour per lot |
| Hardware corrosion | Salt spray on metal parts | ASTM B117, 24–48 h to buyer’s requirement | Per hardware lot |
| Final random inspection | Workmanship, dimensions, function, packing, carton marks | AQL 2.5 major / 4.0 minor | ISO 2859-1 single sampling |
Two points about that plan. First, the interface is inspected as a functional item, not a visual one: we mount the pouch on a gauge cut to the standard and check that it seats, that the strap threads all rows, and that it does not rotate under a 2 kg pull. Second, defects are classified before inspection, not after. A missed bar-tack is major; a 1 mm stitch wander inside a hidden seam is minor; a zip that skips is critical. Buyers who agree the classification at PO stage get a report they can act on rather than a percentage.
MOQ, Sampling and Production Timeline
The commercial terms are deliberately simple so that planning is possible: 500 pieces per style, 6–10 working days for sampling from a confirmed specification, and 35–50 days for mass production after sample approval and deposit.
| Stage | Duration | What the buyer provides |
|---|---|---|
| Specification review and quotation | 2 working days | Reference sample or drawings, contents list, target market, quantity, branding artwork |
| Interface and size confirmation | 2–3 working days | The carrier the pouch must fit, or its measured interface dimensions |
| Lab dip and artwork proof | 5–7 working days | Pantone references, logo files, placement intent |
| Sampling | 6–10 working days | Approved spec sheet; one consolidated comment round |
| Sample approval | 2–5 working days | Signed sample or written comments |
| Bulk material and component booking | 7–15 working days | Deposit; confirmation of hardware and zip family |
| Mass production | 35–50 days | Approved sample, artwork, packaging specification |
| Final inspection and shipping | 3–5 days | Inspection instruction, shipping marks |
The variable that moves a pouch delivery is almost never sewing capacity — it is component and fabric lead time. A non-stock zip colour, a custom buckle mould or a Pantone fabric that has to be dyed adds two to four weeks on its own, and a launch date that assumes stock components will slip if the hardware is specified late. Where a date is fixed, we book fabric and hardware before sample approval rather than after.
Cost Drivers: Where the Money Actually Goes
Two pouches that look identical on a shelf can differ by 60% in FOB, and the difference is almost never the fabric price per metre. The table below is the cost structure we quote against, in the order the money actually moves.
| Driver | Share of unit cost | How it moves |
|---|---|---|
| Labour (cutting, sewing, bar-tacking, trimming) | 30–45% | Panel count, webbing rows, interior loops and binding operations dominate; a 4-row PALS panel is roughly 3× the sewing time of a plain back |
| Shell fabric | 15–25% | Fabric weight and yield; a 1000D shell costs roughly 1.6× a 500D shell per pouch |
| Zip and closure | 8–15% | Zip size and length, brand, reverse-coil vs standard, number of pulls |
| Hardware | 6–12% | Buckle family, metal vs polymer, D-rings, clips; metal hardware can double this line |
| Interior components | 5–10% | Elastic, hook-and-loop, mesh, key leash, stiffener |
| Branding | 3–8% | Embroidery stitch count, patch size, number of print colours |
| Packaging and freight prep | 3–8% | Polybag vs retail box, hangtag, carton marks, compression packing |
| Inspection and overhead | 5–8% | Test plan depth, AQL level, documentation |
The practical consequence: if a target price is missed, the answer is usually to remove operations rather than to downgrade the shell. Dropping one webbing row, replacing a sewn patch with a woven label, or simplifying the interior from four elastic loops to two usually recovers more margin than moving from 500D to 210D — and it does not turn a field pouch into a product that fails in the field.
Compliance: What Can Be Documented and What Cannot
Pouches sold into the EU, the US and the UK are checked against textile and chemical rules before they are checked against anything else, and the questions that arrive in development are predictable.
- Chemical restrictions: we work to REACH Annex XVII for azo dyes, nickel release and restricted substances, and to California Proposition 65 where the buyer sells into that market. Lead and cadmium limits apply to hardware and to any coated trim.
- PFAS: EU and several US states now restrict fluorinated water repellents in textile articles. Our default on new developments is a C0 (PFAS-free) DWR, and we will state the finish in writing so the buyer can put it in a compliance file.
- Recycled content: where a recycled claim is made, it needs a certificate chain. We source GRS-certified recycled polyester and pass on the mill’s transaction certificate for the specific order; we do not state a recycled percentage that cannot be documented.
- Flammability and children’s use: pouches are not children’s products, but small parts, cords and clips matter if a buyer markets an item to under-14s. We flag that in development rather than at inspection.
- What we do not claim: we do not describe a commercial pouch as mil-spec, Berry-compliant or NSN-listed unless the buyer’s own contract and testing make that true. We build to the buyer’s test protocol and report the results; we do not manufacture a certification.
Why Brands Consolidate EDC Pouches With Us
Most of our pouch programs sit inside a larger bag range, and the reason buyers keep them here is operational rather than romantic. A pouch uses the same cutting room, the same walking-foot machines, the same bonded nylon thread and the same hardware suppliers as a backpack or a tool bag, so a brand that already runs a bag program adds a pouch line without adding a second supply chain, a second colour approval cycle or a second carton specification.
On the technical side, the shared capability that matters is our work on small, dimensionally critical panels with heavy webbing — the same operations we run for tactical bags and tool bags, where a 2 mm error at a mounting point is a functional defect rather than a cosmetic one. A pouch is a compressed version of that engineering, which is why we can usually go from a buyer’s reference sample to a working prototype in one round.
Where a buyer’s range extends into protective and hard-shell carry, the same factory builds EVA cases and camera bags; where it extends into outdoor and wet use, it builds hiking backpacks, waterproof bags and dry bags on the same cells. Brands building a first-line or responder range usually pair the utility pouch with our first aid bag and clear PVC bag patterns, which share the same binding, webbing and print setup.
Frequently Asked Questions
Start an EDC Pouch Program
Send the contents list, the platform the pouch must attach to (or one physical sample of it), the target size and packed volume, the shell material or a reference product, the branding artwork and the market the pouch will be sold in. We will come back inside two working days with a construction recommendation, an interface drawing, a size sheet and a quotation. If the construction is not settled, we can start from one of the ten builds above and adapt it — most pouch programs begin with an existing pattern and one meaningful change, not a new design from zero.
What we need to quote accurately: contents and their dimensions, interface type or the carrier sample, target external size, shell preference, closure type, interior retention requirements, branding method and artwork, packaging format, order quantity and required delivery window. What we will tell you honestly: where a requested interface will not seat on the platform you named, where a compliance claim cannot be documented, and where a cheaper material will cost more in returns over the life of the product.
Request an EDC Pouch Quote
500 pcs MOQ · 6–10 day sampling · 35–50 day production · AQL 2.5 major / 4.0 minor · OEM/ODM since 2014
Related Manufacturing Pages
- Custom Bag Manufacturer — OEM/ODM Hub
- Custom Tactical Bag Manufacturer
- Custom Tool Bag Manufacturer
- Custom EVA Case Manufacturer
- Custom Camera Bag Manufacturer
- Custom First Aid Bag Manufacturer
- Custom Clear PVC Bag Manufacturer
- Custom Crossbody Bag Manufacturer
- Custom Laptop Bag Manufacturer
- Custom Packing Cubes Manufacturer
- Custom Waterproof Bag Manufacturer
- Custom Hiking Backpack Manufacturer