A bag and case manufacturer established in 2014, with our founder in the industry since 2004. We build private-label thermoformed and compression-molded EVA cases — tool cases, drone and electronics cases, first aid cases, cosmetic cases, medical kits and die-cut foam organizers — for brands, industrial distributors, retailers and promotional programs.
Looking for a custom EVA case manufacturer? Junyuan Bags has been producing bags and cases since 2014 — our founder has worked in the industry since 2004 — and today we manufacture private-label molded EVA hard cases, tool cases, and foam organizer cases for tool and industrial brands, electronics and drone accessory brands, medical and first-aid suppliers, cosmetic brands, and promotional distributors in North America, Europe, and Australia. Every bulk order is inspected to AQL 2.5 major / 4.0 minor, with MOQ 500 pieces per style, sampling in 6–10 business days, and mass production in 35–50 days. Combined capacity across our affiliated and partner factories covers programs from 500 to 50,000 pieces per style, quoted within 24–48 hours of a complete specification.
- ✓ Shell engineering, not catalogue picking — EVA grade, sheet thickness, mold shape and foam layout specified against the product the case must protect
- ✓ Both molding routes available — thermoformed (vacuum-formed) shells for short runs and compression-molded matched-mold shells for rigid, structural cases
- ✓ Foam is drawn, not cut by eye — die-cut PE, EVA and PU inserts built from your product’s CAD or a physical sample
- ✓ AQL 2.5 major / 4.0 minor inspection — shell wall thickness, mold release marks, hinge cycling, zipper cycling, latch retention and drop testing on every batch
- ✓ Direct manufacturer pricing — you work with the production team, not a trading layer
- ✓ Low entry point — 500 pieces per style, up to three colorways mixed in one order
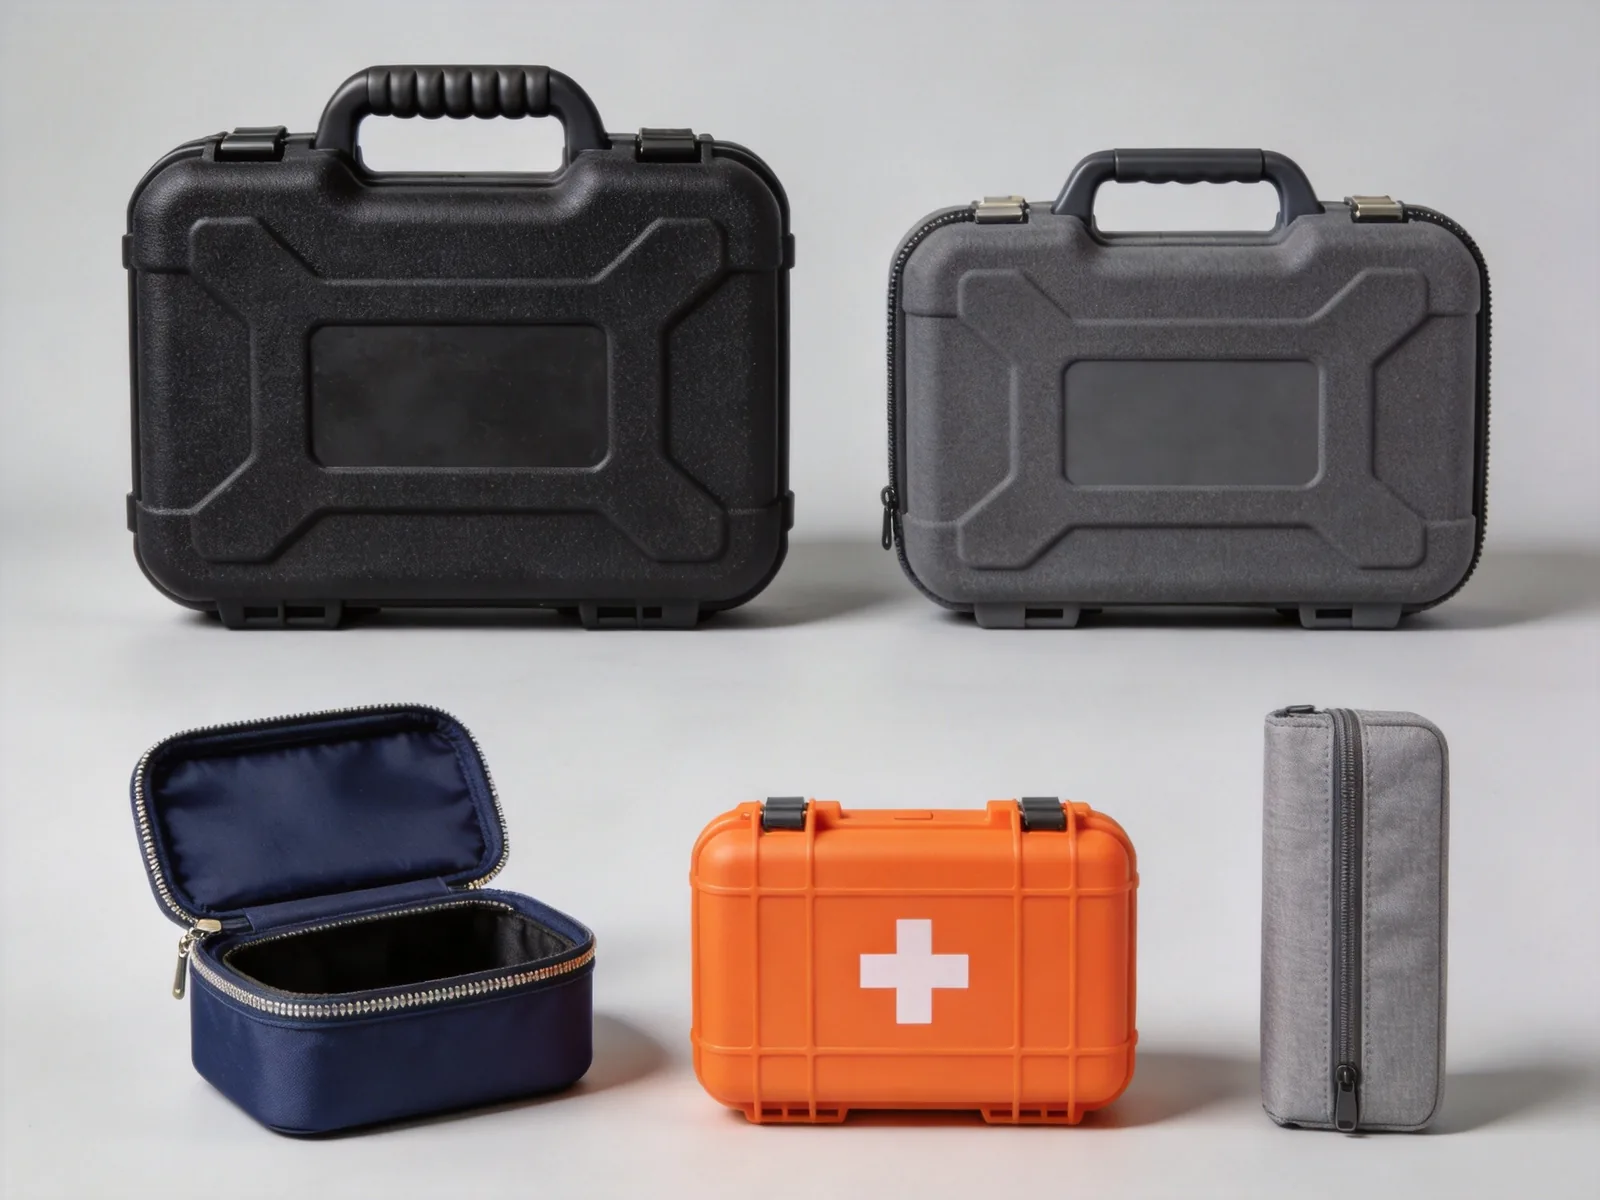
Custom EVA cases — molded tool case, drone case, zip-around cosmetic case, first aid case, and slim organizer, built to your specification
What Is a Custom EVA Case and Who Buys Them?
A custom EVA case is a semi-rigid or rigid protective case whose shell is formed from ethylene-vinyl acetate foam sheet, laminated to a fabric face and usually lined inside, with a cavity shaped to hold a specific product. It is not a bag with padding added: the shell itself carries the impact load, the foam insert locates the product so it cannot move, and the opening, hinge, and closure are designed around how the product is used. “Custom” means the mold cavity, sheet thickness, foam layout, fabric, color, hardware, and branding are all set per order rather than picked from a stock catalogue.
The category is bought by five main groups. Tool and industrial brands order molded tool cases and blow-molded or EVA socket sets where the foam layout is part of the product’s selling proposition. Electronics, drone, and audio brands order zip-around EVA hard cases for headsets, controllers, gimbals, and accessories, usually as a retail-ready SKU or a bundle item. Medical and safety suppliers order first aid cases, diagnostic kit cases, and defibrillator or training kit cases where a cleanable interior and a fixed layout matter. Cosmetic brands order zip-around cosmetic and makeup cases, often with an internal mirror and brush slots. Promotional and corporate distributors order EVA cases for tool kits, gift sets, and staff equipment because the format photographs well and survives shipping.
Because the buyer is protecting something specific, the specification conversation is technical from the first email: what the case must hold, how much drop it must survive, whether the shell must be rigid enough to stack, whether the interior must be wipe-clean, and how the case is presented at retail. Those five answers decide the mold, the sheet, and the foam — which is why we quote the shell and the insert together.
EVA Case Types We Manufacture
The table below shows the formats we produce most often, with the construction each one normally carries. Every column is adjustable: cavity shape, shell thickness, foam layout, and closure type are set by your product and your channel.
| Style | Best for | Typical construction | Closure | MOQ |
|---|---|---|---|---|
| Molded tool case | Hand tools, socket sets, service kits | 3–4 mm compression-molded EVA + 1680D face, die-cut PE foam | Zip-around or twin latch | 500 pcs |
| Zip-around EVA hard case | Headphones, gimbals, controllers, small electronics | 2–3 mm thermoformed EVA + 600D jacquard, mesh lid pocket | #8 reverse-coil zip | 500 pcs |
| Drone / camera gear case | Drones, action cameras, lens kits | 3–5 mm molded EVA shell, convoluted lid foam, die-cut base | Zip-around + carry handle | 500 pcs |
| First aid / medical kit case | Workplace kits, EMT bags, diagnostic sets | 3 mm EVA shell, wipe-clean PVC or TPU lining, elastic loops | Zip-around or latch | 500 pcs |
| Cosmetic / makeup case | Retail beauty sets, brush kits, travel organizers | 2–3 mm EVA + PU or velvet laminate, mirror panel, brush slots | #5 or #8 zip-around | 500 pcs |
| Slim organizer case | Cables, pens, EDC, stationery, small parts | 2 mm EVA shell, elastic webbing grid, mesh pocket | Zip or elastic band | 500 pcs |
| Presentation / gift case | Premium retail sets, corporate gifts, sample kits | 3–4 mm molded EVA, velvet or satin lining, ribbon pull | Latch or magnetic flap | 500 pcs |
| Insert-only foam tray | Adding protection inside a case you already sell | Die-cut PE 25–35 kg/m³ or EVA 40–60 kg/m³ tray | None (drop-in) | 500 pcs |
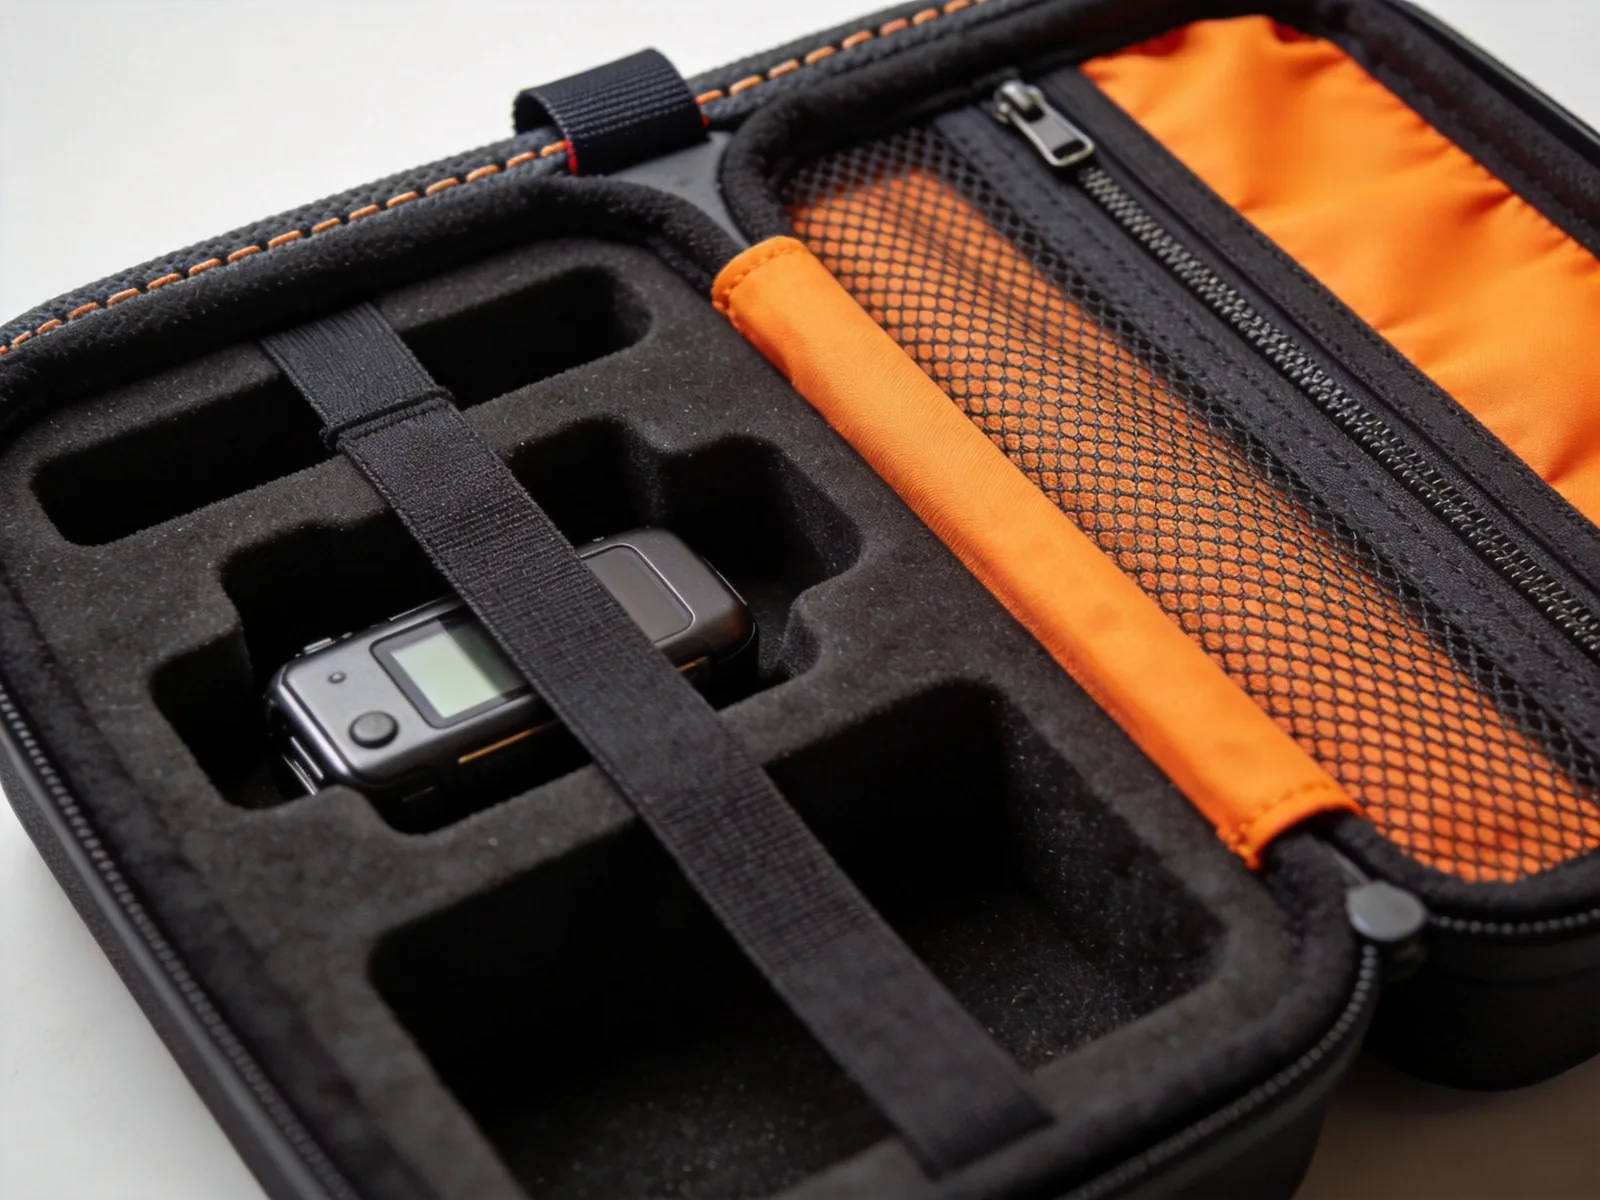
Die-cut foam cavity, elastic retention strap, and a zippered mesh lid pocket — the insert system that defines an EVA case
EVA Molding: Shell Construction, Foam & Lining
Most quality problems in EVA cases trace back to the shell process, not the fabric. We specify the process first, then the material around it.
Thermoforming versus compression molding
- Thermoformed (vacuum-formed) shell — EVA sheet is heated to roughly 120–160 °C, drawn over a male mold under vacuum, cooled, then trimmed and bound. Tooling is cheaper and lead time is shorter, which suits 500–3,000 piece runs and softer zip-around cases. Wall thickness thins at deep draws, so cavity depth is limited.
- Compression-molded shell — EVA sheet or preform is pressed between matched male and female molds. Wall thickness stays uniform at depth, corners are sharper, and the shell is genuinely rigid — the right route for tool cases that must stack or survive a van floor.
- Framed hybrid — a sewn EVA body stiffened by a PP or ABS frame and a PE board in the lid. Used where the case must look soft-sided at retail but hold shape when loaded.
Sheet grade, thickness and hardness
Case shells run EVA sheet at 2.0–5.0 mm, typically with a vinyl acetate content around 18–22%. Thin sheet at 2–2.5 mm gives a flexible zip-around case for headphones and small electronics. Mid-range 3–4 mm is the working thickness for tool and kit cases. At 4–5 mm, with a compression-molded shape, the case behaves as a rigid box. Hardness is specified in the 35–55 Shore C band for foam-core sheet and higher for solid EVA sheet; we quote the grade against the drop requirement rather than by name, because two sheets at the same thickness can behave very differently after molding.
Face lamination and lining
The shell face is laminated before forming, so the fabric must survive the heat cycle without glossing, shrinking, or delaminating at the draw. We run 600D polyester, 1680D ballistic-style nylon, 300D jacquard, PU leather, waxed canvas, and RPET recycled polyester on the outside; inside we use 210D polyester, 190T taffeta, velvet-touch tricot, jersey, and wipe-clean PVC or TPU. Lamination is the point where cheap cases fail in the field — a shell that delaminates at the corner has no repair, so we cycle-test the laminate before bulk.
Material Comparison for EVA Case Shells
| Shell / face material | Gauge | Rigidity & protection | Finish & durability | Typical use |
|---|---|---|---|---|
| EVA + 600D polyester | 2.0–3.0 mm | Semi-rigid, good shape memory | Matte, abrasion resistant, economical | Zip-around electronics and cosmetic cases |
| EVA + 1680D nylon | 3.0–4.0 mm | Rigid, high puncture resistance | Textured, premium hand-feel | Tool cases, drone cases |
| EVA + PU leather | 2.0–3.5 mm | Semi-rigid, smooth surface | Premium look, wipe-clean | Cosmetic, presentation and gift cases |
| EVA + 300D jacquard | 2.0–3.0 mm | Semi-rigid, light | Fine weave, print-friendly | Retail electronics accessories |
| EVA + waxed canvas | 3.0–4.0 mm | Rigid with a soft face | Water-repellent, ages well | Heritage tool and outdoor lines |
| EVA + RPET polyester | 2.5–3.5 mm | Comparable to virgin polyester | Matte, recycled-content story | Brands with sustainability targets |
| Solid EVA sheet (unlaminated) | 3.0–5.0 mm | High rigidity, clean edges | Wipe-clean, color-through | Medical, laboratory and industrial trays |
| PE / EVA foam (insert only) | 10–60 mm | Shock absorption and location | Die-cut, closed or open cell | Foam trays inside any shell |
Hardware follows the same logic. Zippers are #5 or #8 nylon coil, reverse-coil on cases where the teeth must not touch the product, with binding tape over the seam so the slider never contacts the contents. Latches are ABS or zinc alloy with a spring-loaded tongue; hinges are either a living EVA fold, a stitched fabric hinge, or a metal piano hinge on long cases. Handles are rubber over-molded, webbing, or PU-wrapped, bar-tacked into a reinforced panel rather than sewn to the shell face alone. Stitch density runs 8–10 stitches per inch with bonded nylon thread.
Interior Organization: Die-Cut Foam, Dividers & Insert Systems
The insert decides whether the case is used daily or returned. We build it from your product’s CAD file, a physical sample, or a measured drawing, and we specify three variables together: foam type, foam density, and how the product is retained.
Foam types and where they are used
- PE foam, 25–35 kg/m³, die-cut — the default for tool and kit cases; firm, dimensionally stable, and cuts cleanly into tight cavities
- EVA foam, 40–60 kg/m³ — denser and more resilient, used where the product is heavy or the cavity is thin-walled
- PU convoluted (egg-crate) foam — lid-side compression so the product is pressed down rather than rattling
- Cross-linked PE (IXPE/XPE) — fine cell structure for electronics where surface finish matters
- EVA + velvet laminate — presentation trays for premium and gift sets
Retention systems
Products stay put through one of four methods, and most cases use two together: a die-cut cavity that matches the product outline within 1–2 mm, an elastic webbing strap across the cavity, a zippered mesh pocket on the lid for accessories, or elastic loops for cylindrical items such as pens, vials, and drivers. Cavity depth is set so the product sits flush or slightly proud, never recessed so deep that a finger cannot lift it — we cut a finger notch or a ribbon pull in every tight cavity.
Insert-only development
If you already sell a case, a bag, or a tool kit, the fastest route to a protected SKU is a standalone foam tray: we cut the insert to your existing internal dimensions, add a lid layer or a retention strap, and deliver a drop-in unit at 500 pieces. It ships flat, needs no tooling on your side, and turns an existing product into a protected kit without a new mold.
Customization, Branding & Private Label
Every element below is set per order, and none of them changes the MOQ structure: one style, 500 pieces, up to three colorways mixed.
- Cavity and mold shape — drawn to your product; new molds are quoted separately and confirmed before sampling
- Shell colors — face fabric, binding, zipper tape, webbing, and hardware matched to Pantone or approved lab dips
- Logo methods — silkscreen, heat transfer, rubber patch, woven label, metal plate, embossed or debossed PU patch, and interior lining print
- Hardware — matte black, gunmetal, brushed nickel, antique brass, and light gold; D-rings, carabiners, lockable sliders, and padlock loops
- Interior — die-cut foam layout, elastic loops, mesh pockets, document sleeves, mirror panels, and printed foam
- Carry — rubber or PU handle, shoulder strap with swivel hooks, trolley sleeve, belt loop, and MOLLE-compatible webbing
- Packaging — branded poly bag, printed retail box, hangtag, sleeve band, and set boxes for multi-piece kits
For private label, we produce under your brand only: no third-party markings on the product, the packaging, or the carton. Artwork proofs are issued before sampling, and a physical pre-production sample is approved in writing before bulk starts.
EVA Case Size & Capacity Reference
The dimensions below are reference points from our most-ordered formats, not a fixed catalogue. Any of them can be re-drawn for a specific product.
| Reference | Format | External (cm) | Internal (cm) | Holds |
|---|---|---|---|---|
| EV-01 | Slim organizer case | 24 × 16 × 5 | 22 × 14 × 3.5 | Cables, pens, EDC, small parts |
| EV-02 | Zip-around electronics case | 26 × 20 × 9 | 23 × 17 × 7 | Headphones, controller, power bank |
| EV-03 | Cosmetic case | 28 × 18 × 10 | 25 × 15 × 8 | Brush set, palettes, bottles |
| EV-04 | Drone / action camera case | 34 × 26 × 12 | 31 × 23 × 9 | Drone, controller, batteries, props |
| EV-05 | Molded tool case, medium | 40 × 30 × 12 | 37 × 27 × 9 | Socket set, spanners, driver set |
| EV-06 | Molded tool case, large | 48 × 36 × 16 | 44 × 32 × 12 | Full service kit, 60–80 tools |
| EV-07 | First aid case | 30 × 22 × 14 | 27 × 19 × 11 | Workplace kit, elastic loops, pocket |
| EV-08 | Presentation / gift case | 32 × 24 × 8 | 29 × 21 × 5.5 | Premium set, sample kit, corporate gift |
How to Order Custom EVA Cases
The process runs in five steps and typically completes in 41–60 days from a confirmed specification.
- Specification — send the product the case must hold (CAD, photo, or a physical sample), the drop and stacking requirement, the format, quantity, logo method, and target retail price. We return a quotation within 24–48 hours with a proposed shell process and foam layout.
- Mold and artwork — we issue a dimensioned drawing, a mold proposal, and an artwork proof for approval, including logo placement, hardware finish, and label positions. New mold cost is quoted separately and is a one-time charge.
- Sampling — a physical pre-production sample is built in 6–10 business days. Sample cost is charged at material and labor value and is offset against the bulk order once the 500-piece MOQ is confirmed.
- Bulk production — 35–50 days after written sample approval, depending on quantity, molding process, and the number of logo and lining steps.
- Inspection and shipping — AQL 2.5 major / 4.0 minor inspection with a photo and measurement report, then carton marking and shipment by sea, air, or express, or FBA-ready prep.
Compliance & Documentation
EVA cases ship into retail, industrial, and medical channels, so documentation is prepared alongside the goods rather than after the fact. We work with REACH-compliant, AZO-free, and phthalate-free materials, and can supply material declarations, heavy-metal and phthalate screening statements for California Proposition 65 programs, color fastness reports, and hardware salt-spray results. Where a program requires it, we also provide a signed compliance declaration per shipment and lot-level traceability for EVA sheet, face fabric, and foam. For medical and first-aid buyers we can quote wipe-clean linings that withstand routine disinfection and specify materials without added antimicrobial claims, so your product copy stays accurate.
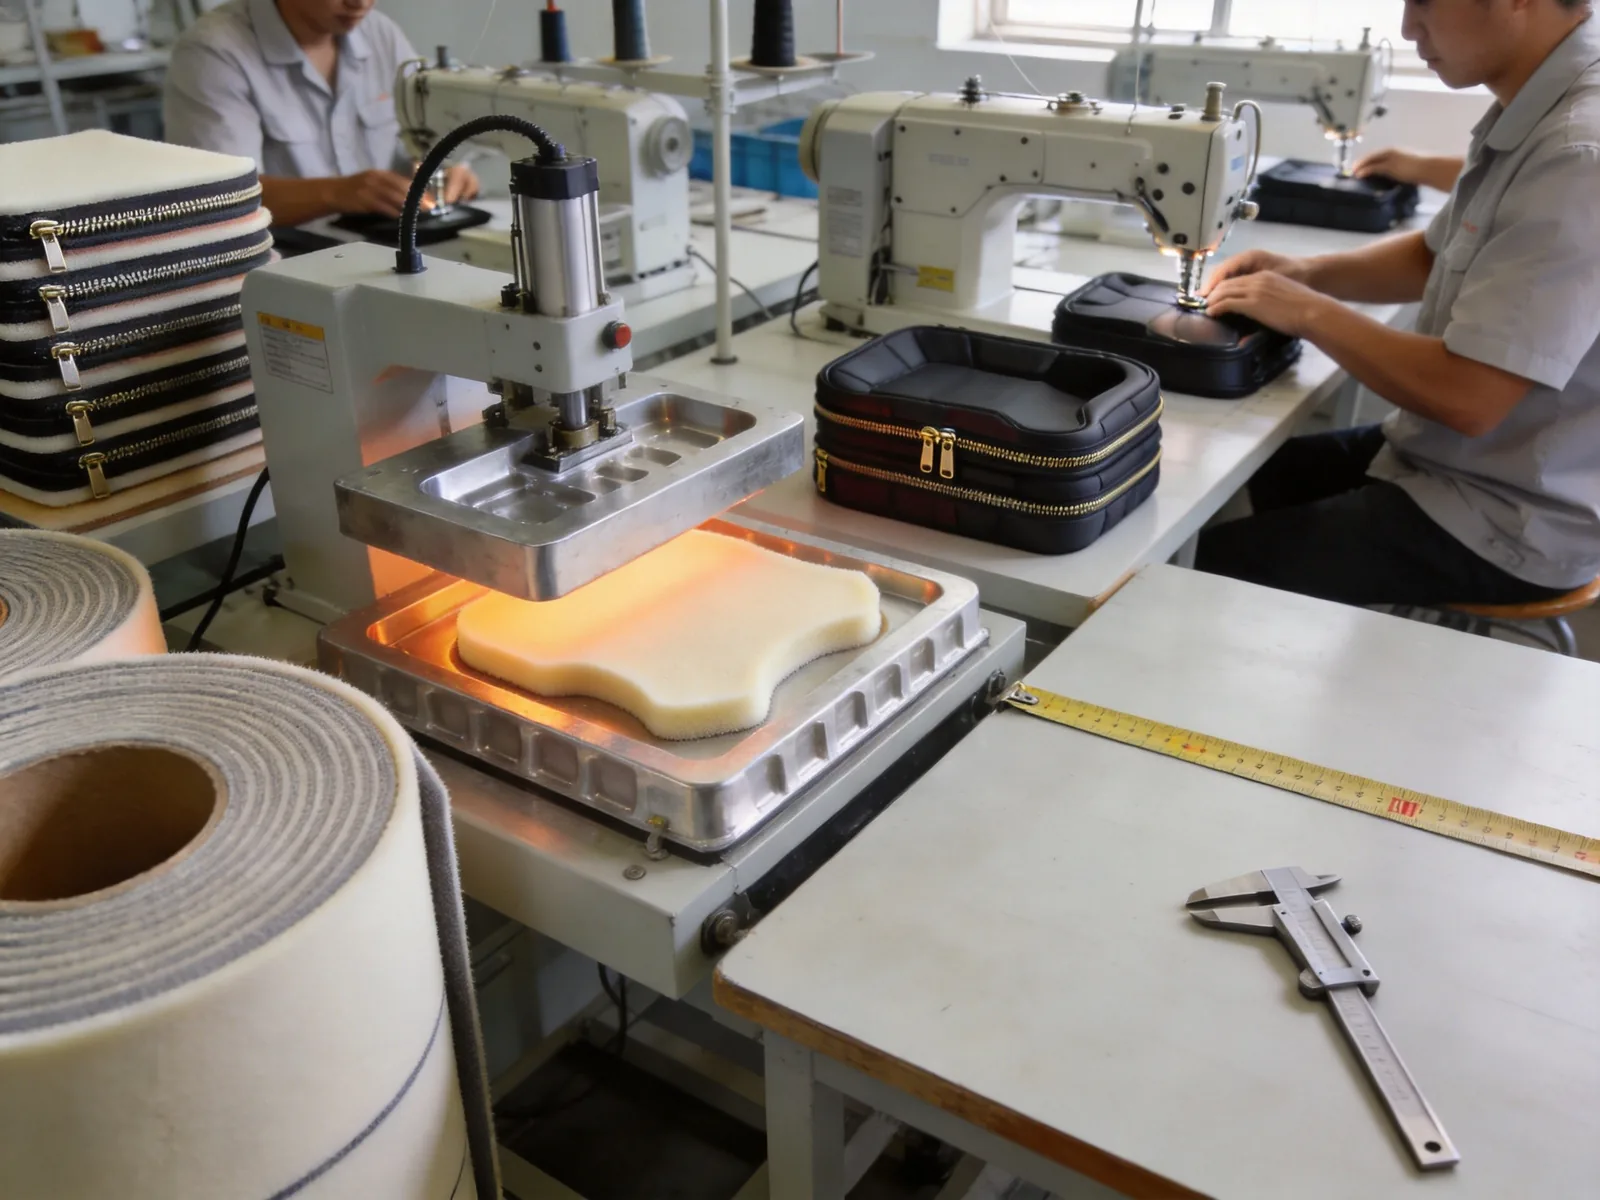
Thermoforming, zipper stitching, and dimensional inspection across our affiliated and partner factories
Quality Control & AQL 2.5 Inspection
Inspection is built into the schedule, not added at the end. Inline checks run at sheet cutting, after molding, and at final packing; the pre-shipment inspection applies AQL 2.5 for major defects and 4.0 for minor defects. The checklist covers:
- External and internal dimensions against the approved drawing, including cavity fit within 1–2 mm
- Shell wall thickness at the base, corners, and deep draws, measured with a caliper
- Laminate adhesion and delamination check after the heat cycle and a 24-hour load test
- Hinge cycling — 500 open-and-close cycles on a sampled case, with no cracking at the fold
- Zipper cycling and slider smoothness, including reverse-coil main compartments
- Latch retention and spring return; handle and strap anchor pull strength
- Foam cavity accuracy, compression recovery, and retention strap tension
- Lining bond, stitching, and thread trimming inside the cavity
- Hardware plating appearance and salt-spray performance
- Logo registration, placement tolerance, and adhesion
- Color match against the approved lab dip under standard light
- Drop test on a sampled carton and case, plus packing accuracy and carton marking
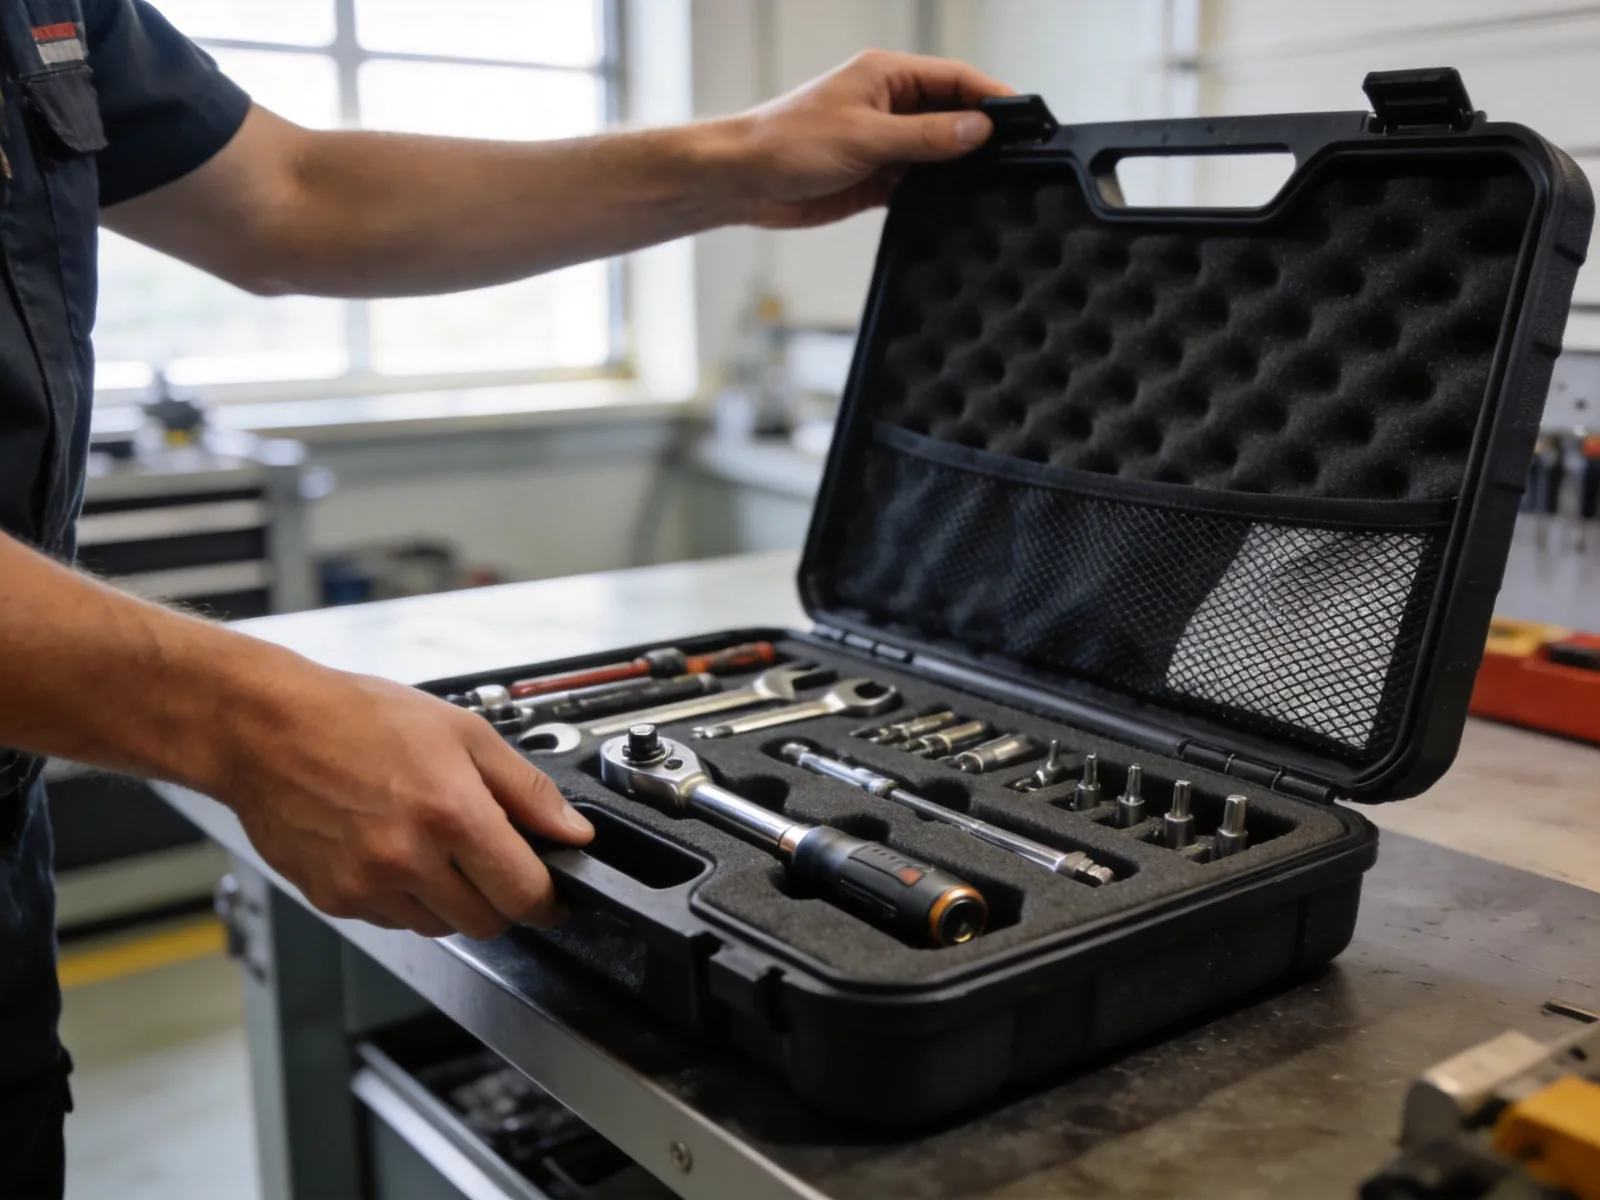
Field use decides the design: cavity layout, lid foam compression, and handle position are specified for real working conditions
EVA Cases for Retail, Industrial, Medical & Promotional Programs
Different channels need different cases, and the specification shifts accordingly. Retail lines need shelf presence, a clean logo, and a printed box, with the shell finished so it photographs well under store lighting. Industrial and tool buyers need rigidity, stackability, a lockable closure, and a foam layout that survives daily removal and replacement of tools — the case is handled by many users and often lives in a van. Medical and first-aid buyers need a wipe-clean interior, fixed elastic loops so items return to the same place, and a closure that a gloved hand can operate. Promotional programs need a low unit cost, a large logo area, and a shorter lead time, and often accept a thinner shell with a simpler foam tray.
For e-commerce sellers, the slim organizer and zip-around electronics formats are usually the better first SKU: lighter shipping weight, lower carton cube, and no mold cost if an existing shape can be adapted. Many of our clients launch an organizer case first, then add a molded tool or drone case once the first container sells through.
Why Work With Junyuan Bags?
We are a bag and case manufacturer established in 2014, with our founder in the industry since 2004, and our production is concentrated in the categories we know best: golf bags, backpacks, travel bags, and technical protective carriers. That focus is why an EVA case brief does not get translated into a fabric pouch with foam glued inside — the shell and the insert are drawn by the same team that builds the case.
- Shell engineering included — molding route, sheet thickness, and foam layout proposed with the quotation, not sold as an upgrade
- One accountable team — sampling, bulk, inspection, and documentation handled by the same production group
- 500-piece entry — a first order that fits a launch plan without heavy inventory risk
- Consistent specification — approved sample, approved lab dip, and approved drawing are the reference for every reorder
- Realistic lead times — 6–10 days sampling and 35–50 days bulk, quoted against the actual material, mold, and logo steps
Ready to Start Your Custom EVA Case Order?
Send Your Product Spec, Get a Quotation in 24–48 Hours
Tell us what the case must hold, the drop and stacking requirement, the format you have in mind, your quantity, and your logo method. We will propose the shell process, foam layout, drawing, and price — MOQ 500 pieces per style, sampling in 6–10 days.
[email protected] | WhatsApp +86 17750020688
Explore Our Other Custom Bag Lines
Related manufacturing pages
- Custom Bag Manufacturer — OEM/ODM Overview
- Custom Tool Bag Manufacturer
- Custom Camera Bag Manufacturer
- Custom Laptop Bag Manufacturer
- Custom Briefcase Manufacturer
- Custom Makeup Bag Manufacturer
- Custom Lunch Bag Manufacturer
- Custom Cooler Bag Manufacturer
- Custom Waterproof Bag Manufacturer
- Custom Packing Cubes Manufacturer
- Custom Shoe Bag Manufacturer
- Custom Backpack Manufacturer