Premium Hiking Packs: Do You Pay for the Name or the Fabrics?
A factory-backed answer to the exact question every hiker asks – how much of a premium hiking pack’s price is the logo, and how much is real fabric, frame and build. With an honest cost ledger and the budget alternatives that match the spec.
For a premium hiking pack you pay for both – but the fabric is the smaller, more honest part, and the name carries far more than most buyers think. A genuinely premium technical or expedition hiking pack typically retails around $180–$350 (approx.), yet the real factory build cost is closer to $55–$110 (typical). Break that gap down and it is roughly: materials ~44–52%, labor & craftsmanship ~22–28%, frame & tooling/suspension ~13–16%, and packaging, QC & margin ~8–12% – then a further design, brand, distribution, warranty and retail load of about 180%–260% (approx.) is added on top. The label is not worthless (fit engineering, R&D and warranty are real), but on a dollar-for-dollar basis the name contributes far more to the ticket than the textiles. The same high-denier coated and ripstop fabrics, frame and suspension grade is buildable under your own brand for a fraction of the price.
TL;DR / Quick Answer
Mostly you pay for the name – but the real value hides in the frame, fit and build, not the logo. A premium ($180–$350 approx.) hiking pack builds for roughly $55–$110 (typical), so the retail ticket is loaded with a ~180%–260% (approx.) brand, distribution, R&D, warranty and retail premium. On the factory ledger, fabrics account for under a third of build cost; the suspension/frame system, its tooling and qualified assembly are what actually make a $55 build into a $250 pack worth carrying. You should spend on the frame, fit and durable fabric you need, not the badge. If you carry real weight for multi-day trails, budget for a structured, torso-adjustable suspension and high-denier shell – and skip the brand premium if a clean-spec OEM or second-tier build delivers the same grade for less.
1. Where the Premium Actually Goes: Name vs Fabrics, Dollar by Dollar
The fastest way to answer “do you pay for the name or the fabrics?” is to split the retail dollar. From the factory bench, a premium technical hiking pack’s build cost is concentrated in the engineered carry system and durable shell – but both of those together still leave a large share of the ticket untouched by real production cost. That residual is what the logo, distribution and warranty model absorb. Here is the honest split at build cost:
| Cost Bucket at Build | Share of Build Cost | What It Pays For |
|---|---|---|
| Materials (shell, lining, frame, straps, hardware) | ~44–52% | High-denier coated and ripstop nylon, breathable mesh, frame stays, webbing, buckles, quality zippers. |
| Labor & craftsmanship | ~22–28% | A technical hiking pack runs through 90–180 operations; frame mount and fit tuning are hand-heavy. |
| Frame & tooling / suspension | ~13–16% | Frame-board, back-panel, hip-belt and foam molds amortized over the production run. |
| Packaging, QC & margin | ~8–12% | Load and fit testing, inspection, premium boxing and the factory’s own margin. |
Then the retail markup lands on top. Across the category, a premium hiking pack carries a design-brand-distribution-warranty-retail load of roughly 180%–260% (approx.). So the fabric is a real but bounded share of the cost; the name is what inflates the final ticket the most. For a step-by-step look at how fabric grade changes the cost ledger, see our backpack material selection guide, which prices nylon, polyester and canvas line by line.
2. A Factory-Level Cost Ledger for a Premium Hiking Pack
Strip out the badge and the “premium” is a set of discrete, priced engineering choices – not a marketing fog. A made-to-spec technical or expedition hiking pack carries a factory build cost of roughly $55–$110 (typical) depending on capacity, fabric grade, suspension complexity and volume:
| Cost Line | Share of Build Cost | Why It Costs What It Does |
|---|---|---|
| Shell & lining fabrics | ~28–32% | High-denier coated and ripstop nylon (210D–420D and up) plus breathable mesh; recycled-spec and waterproofing add cost. |
| Suspension system (frame, stays, hip belt, back panel) | ~18–22% | The most expensive engineering line – the structural reason premium and budget hiking packs are different products. |
| Hardware, zippers & webbing | ~12–15% | Quality zippers, load-lifter and compression buckles, reinforced webbing – repeated-failure points on cheap packs. |
| Labor & assembly | ~16–20% | Higher operation count; frame fitting, hip-belt shelling and bar-tacking drive hand-time. |
| Tooling & amortization | ~8–10% | Frame-board, back-panel and accessory molds spread across the run. |
| QC, packaging & margin | ~6–10% | Load and fit checks, seam sealing review, premium boxing and the factory’s own margin. |
The decisive insight: fabric (shell + lining) is the single biggest material line, but it still sits below the suspension/frame + its labor, and together those engineered lines – not the textiles alone – explain why a premium hiking pack costs what it does.
3. Does the “Premium” Fabric Really Cost That Much More?
Here is where the honest answer surprises most buyers: premium shell fabrics do cost more, but not dramatically more per pack – and they are a small share of the final ticket. The fabric premium is real but bounded. Compare it line by line:
| Component | Premium Grade | Budget Grade | Real Cost Gap at Build |
|---|---|---|---|
| Main shell fabric | High-denier coated / ripstop nylon (210D–420D+), often recycled | Polyester or low-denier nylon | Denier, coating and recycled-spec step-ups add a meaningful but a few-US-dollars line in a $55–$110 build. |
| Back panel & harness | Breathable structured mesh, molded padding, adjustable torso | Generic flat foam | Ventilation and fit engineering is the biggest genuine premium – build, not cloth. |
| Frame & stays | Perimeter aluminum or composite frame with adjustable stays | None or soft wire | The frame is optional on a budget pack and central on a technical pack – pure engineered cost. |
| Hip belt & load transfer | Structured, load-transferring, torso-adjustable padded hip belt | Slim webbing hip strap or none | Real load-to-hip transfer needs structure and sizing; this is where the value lives. |
| Zippers & hardware | Quality zippers, load-lifter and security buckles | Standard generic zips and buckles | Repeated-failure point; the difference is durability, not glamour. |
| Seam & finish treatment | Taped/sealed critical seams, bar-tacked stress points | Basic single-needle seaming | Long-life durability under load is a labor line, not a material coup. |
The takeaway: the fabric gap between a “premium” and a “budget” hiking pack is a genuine but modest share of build cost. The big kind of premium – the suspension, frame, sizing and build method – is what you are really paying for, and it is the same engineered spec a private-label buyer can source through an OEM.
4. Name vs Fabric: A Tooling View of Where the Money Goes
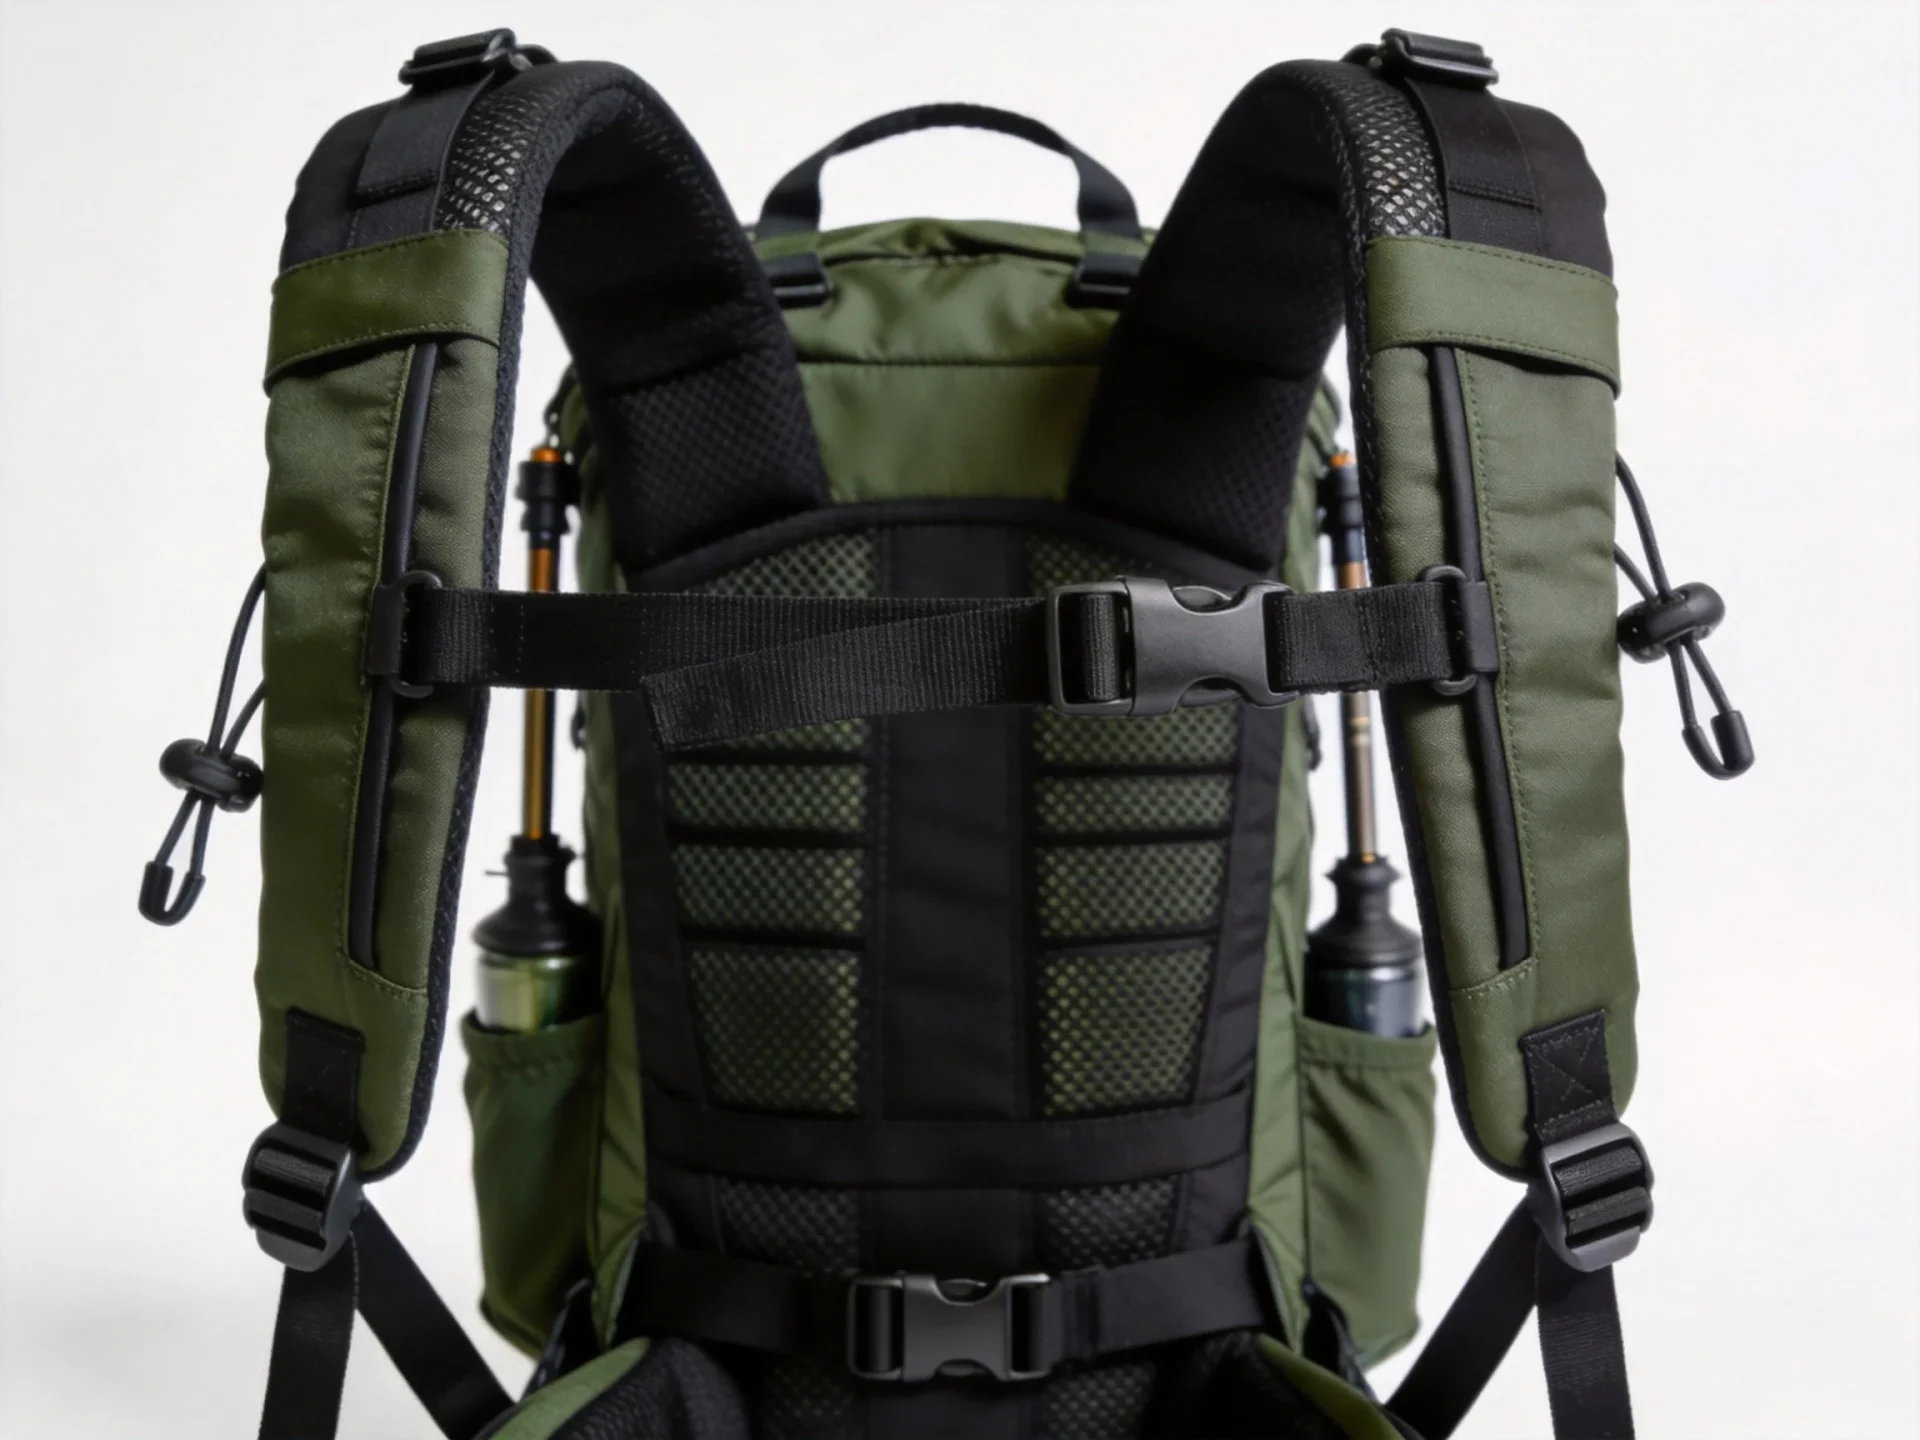
The cleanest way to see that you pay for engineering, not textiles, is to look at what it takes just to tool a premium hiking pack. The molds and dies are the same ones a heritage brand amortizes across thousands of units – and the same ones a private-label buyer can amortize for a single order:
| Tooling / Mold Item | Typical Investment (USD) | Amortized Over | Approx. Cost Per Pack |
|---|---|---|---|
| Molded back-panel / frame-board mold | $9,000–$19,000 | 4,000–8,000 pcs | $2–$4 |
| Hip-belt & shoulder-strap foam molds | $6,000–$12,000 | 4,000–8,000 pcs | $1.5–$3 |
| Ventilated back-system tooling (mesh cage / tension frame) | $6,000–$14,000 | 4,000–8,000 pcs | $1.5–$3.5 |
| Frame stays & load-lifter mounts | $4,000–$8,000 | Full run | $1–$2.5 |
| Brand plate / logo tools | $1,000–$3,000 | Full run | $0.5–$1.5 |
Notice what this list contains: almost no line is “the fabric.” The tools that make a premium hiking pack are tools for fit, structure and load transfer. Fabric is bought off the roll at a modest premium; engineering is what needs tooling and skilled hands. This is also the strongest argument for OEM/ODM: the same molds a heritage brand amortizes are the same molds a private-label buyer gets to amortize. Our travel and technical backpack OEM & feature integration guide walks through exactly which features cost most to tool and assemble.
5. How a Premium Hiking Pack Is Actually Built
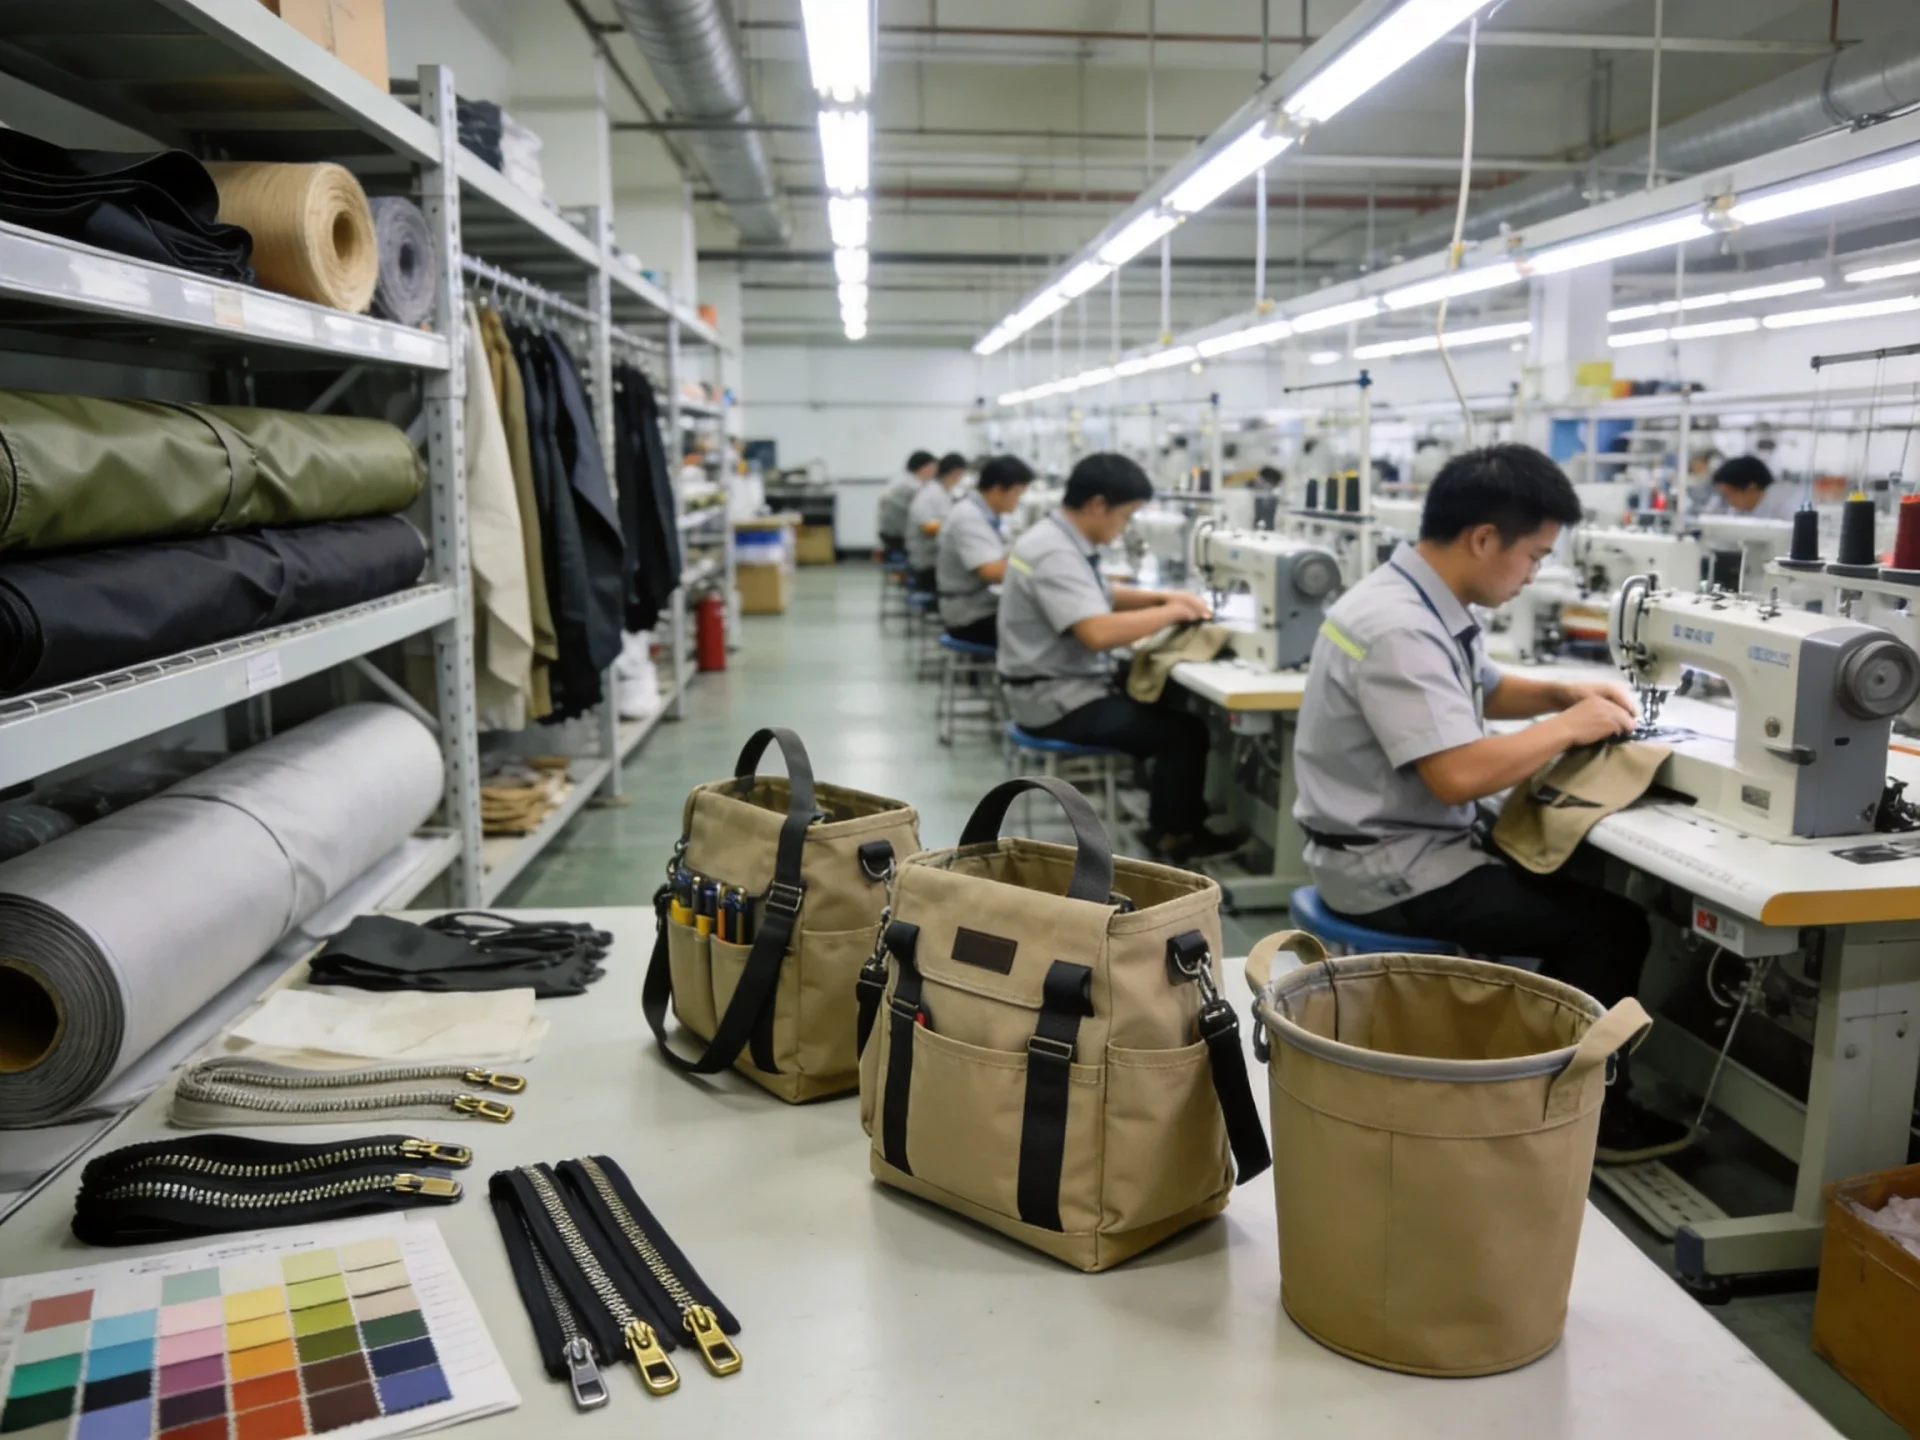
A premium technical or expedition hiking pack travels through roughly 90–180 separate operations depending on capacity and features – far more than a flat commuter pack. In our affiliated factory that runs across 7 production lines with 149 machines (126 sewing) and 137 staff, a trained operator still handles every frame stay, hip-belt panel and critical seam by eye. The steps are the same for a branded pack and a private-label pack:
- Cutting & fusing — panels are cut from roll stock and heat-fused to lining; high-denier recycled-spec outer and breathable mesh back panels are added on premium builds.
- Seam preparation & finishing — critical seams are taped or sealed; premium tiers add fuller coverage and a high stitch-consistency standard.
- Sewing & assembly — body, pockets, back panel and shoulder straps are joined in sequence, with stress points bar-tacked.
- Suspension build & fit — frame stays, molded or ventilated back panel and structured, sized hip belt are assembled, mounted and fit-tested for load transfer.
- Hardware & strap mounting — zippers, load-lifter buckles, compression webbing and harness are fitted and reinforced.
- Final QC & packing — load and fit test, stitch and zipper check, seam-seal review and premium boxing.
The measurable difference between “premium” and “budget” shows up in operations per pack. A fitted suspension with sized hip-belt cups, a ventilated or structured back panel and bar-tacked stress points absorbs more assembly time, pushing labor toward roughly 24–28% of cost – a genuine engineering line, not decoration.
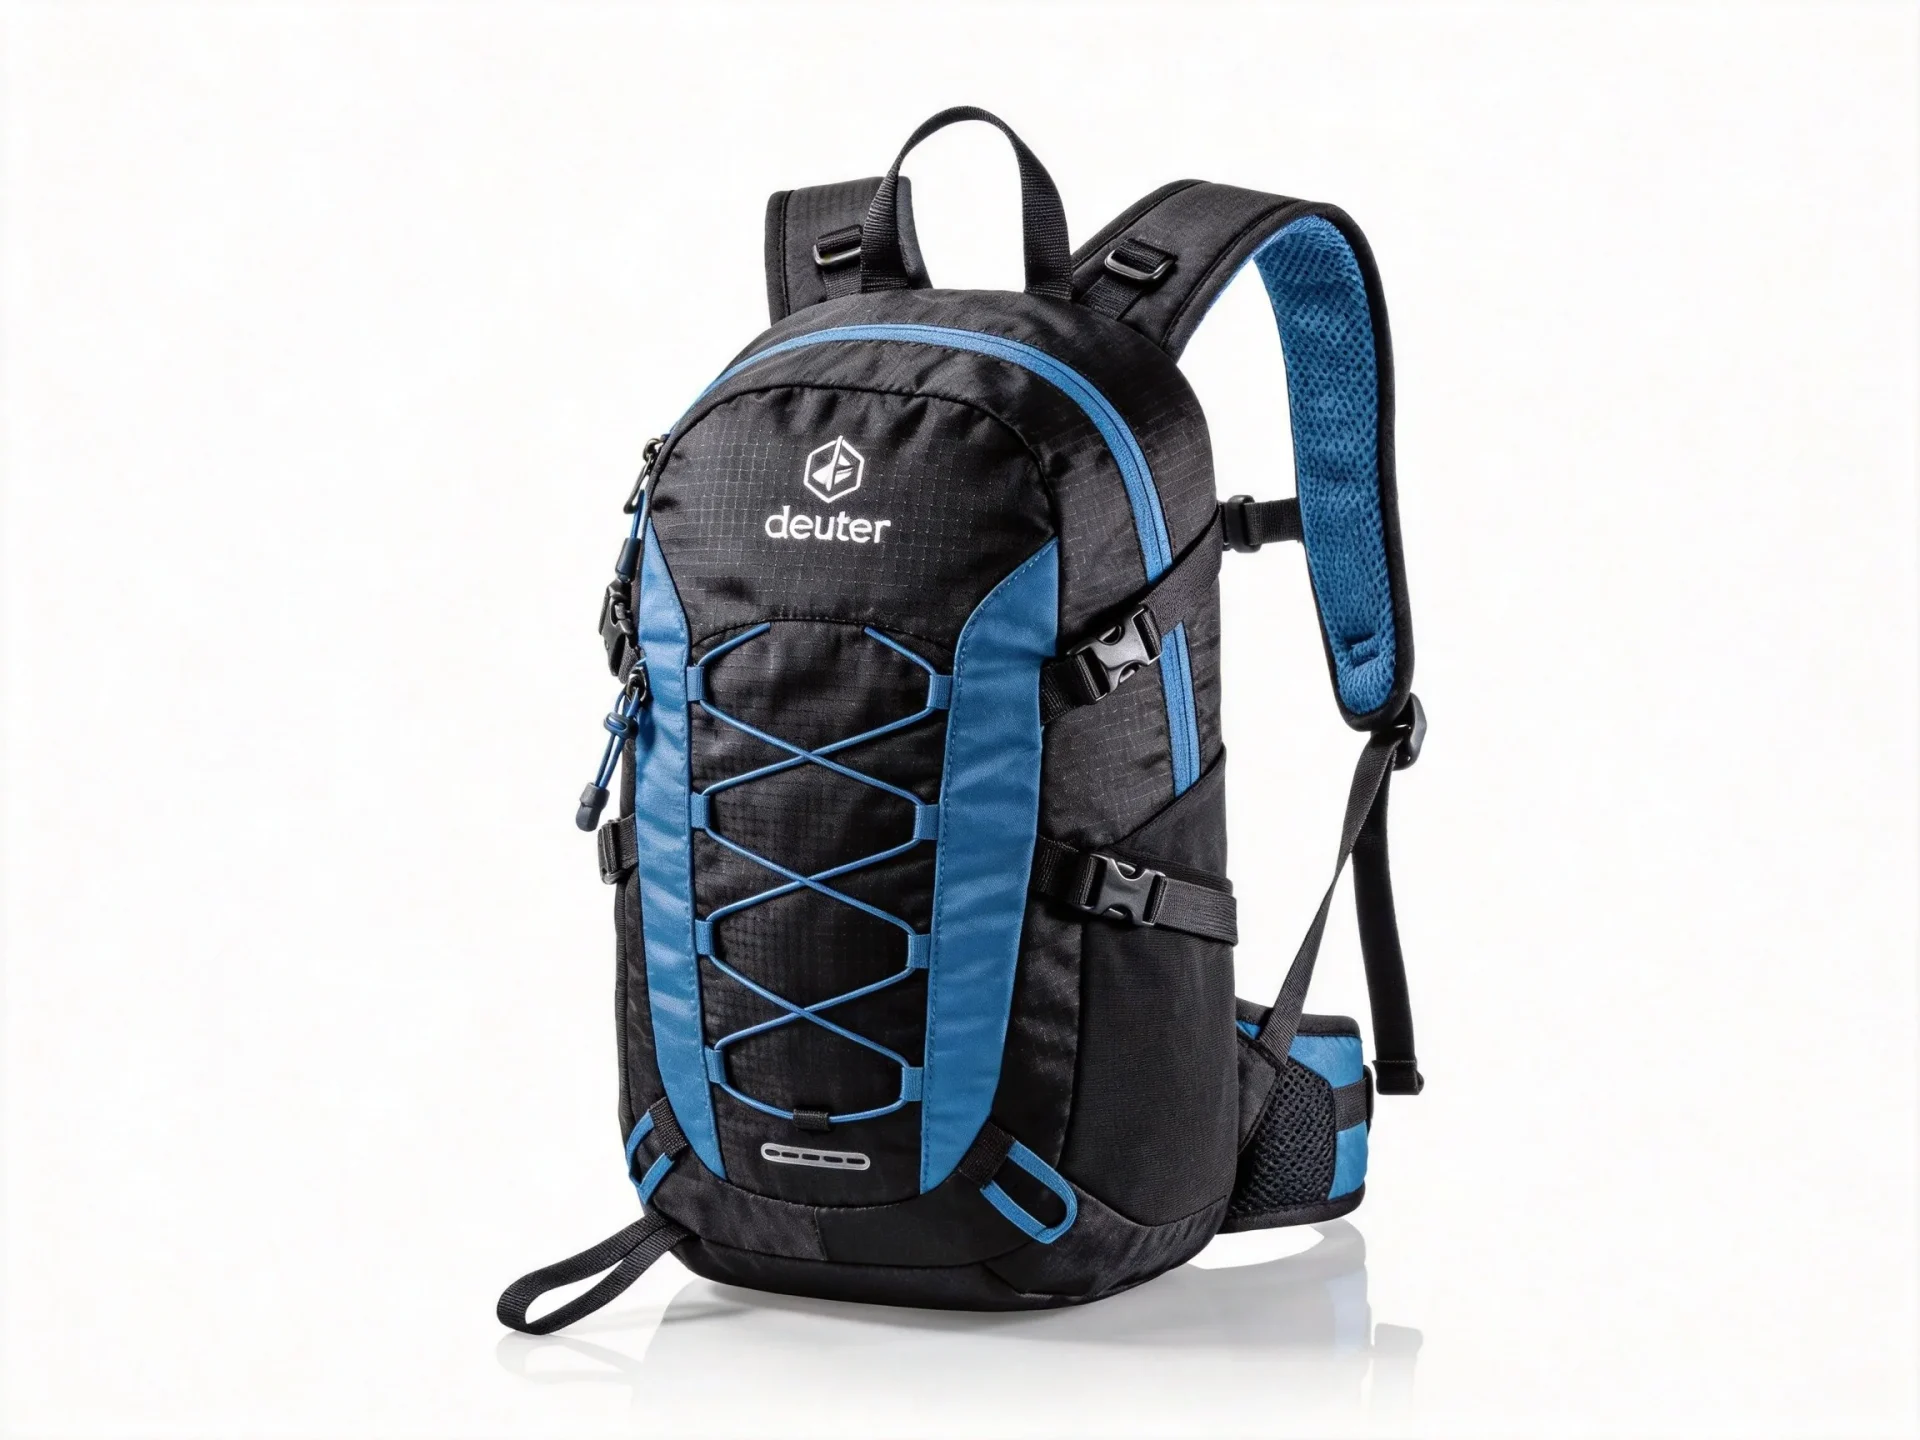
6. So Do You Pay for the Name or the Fabrics?
Here is the straight factory-backed call, and it is more nuanced than “it’s all marketing”:
- You do not mainly pay for the fabric. Shell and lining account for under a third of build cost, and the premium-grade step-up is modest per pack. “Durable fabric” is worth paying for up to a point, but it is not the reason a premium pack costs $300.
- You pay partly for genuine engineering. The frame, torso-adjustable suspension, load-transferring hip belt, breathable back system and fit tuning are real – they are the honest share of the price and the value you can feel on a loaded trail.
- You pay substantially for the name. The 180%–260% (approx.) markup over build absorbs design, R&D, brand, distribution, retail margin and warranty service. That is a real cost of doing business – but it is not a cost of making the bag.
- Skip the premium if you only need the grade, not the badge. The same material, frame, suspension structure and build method is manufactured for private labels worldwide. A clean-spec OEM/ODM hiking pack or a good second-tier brand delivers most of the benefit for a fraction of the ticket.
For the practical side of choosing capacity and fit in this class, see our guide to choosing a hiking backpack and what to expect from hiking backpack manufacturers.
Bottom line: You pay for the name far more than for the fabrics – but the value you should actually spend on is the engineering. The shell fabric is a real but modest share of cost; the frame, fit, suspension and build method are what turn good durable materials into a pack worth carrying for years. Buy the engineering and durability you need, and source the brand premium you actually want – they are separate decisions, and the same grade is buyable under your own label.
Build a Premium-Grade Hiking Pack Under Your Brand
JUNYUAN BAGS is a backpack trading company backed by an affiliated factory in Quanzhou, Fujian – SGS-verified at 4,950 sqm, 7 production lines, 149 machines (126 sewing) and 137 staff, with a monthly line capacity of 200,000 pieces and a vetted partner-factory network. We have supplied 200+ brands across 100+ countries as of 2026. Get the premium engineering – structured suspension, torso fit, high-denier shell – without the heritage-brand markup, made to order and shipped for your brand, shop or wholesale account.
Request a custom hiking pack OEM/ODM quote
See how custom packs are made end-to-end
FAQ: Premium Hiking Packs
Do you pay for the name or the fabrics with a premium hiking pack?
Mostly the name. Shell and lining fabrics account for under a third of build cost, and the premium-grade fabric step-up is modest per pack. The real value share is the frame, suspension, fit and build method, and then a roughly 180%–260% (approx.) brand, distribution, R&D, warranty and retail load is added on top of the ~$55–$110 (typical) factory build cost.
Why are premium hiking packs so expensive?
Because they sell engineered carry, not just a bag. A technical hiking pack adds a torso-length frame, a ventilated or molded back panel, a load-transferring hip belt and higher-denier durable fabrics, plus a warranty service model. The shell fabric is a bounded line; the suspension/frame system and qualified assembly are what carry most of the build cost, and the retail ticket then absorbs a large design-brand-distribution premium.
Is the higher-denier ripstop nylon worth the extra cost?
Generally yes, up to a point. High-denier coated and ripstop nylon (210D–420D and up) resists abrasion, tears and weather far better than cheap polyester or low-denier nylon, and it is the single biggest material cost line. But it is a modest share of a premium pack’s final price – spend on it for durability, not as the reason a pack costs $300.
What actually separates a premium hiking pack from a budget one?
The suspension and fit, not the fabric. A premium pack adds a structured frame, torso-adjustable sizing, a load-transferring hip belt and more assembly operations (90–180 across the build). Those engineered lines and their tooling are the honest cost difference – a $49 flat pack simply has none of them.
Is the brand markup worth paying on a hiking pack?
For the warranty, R&D, fit support and resale value, the brand premium has real value. But dollar-for-dollar on the factory ledger it is a large share of the final ticket. If you carry heavy loads and need proven fit engineering and a solid warranty, the brand can be worth it; if you only need the durable grade, a clean-spec OEM build or a good second-tier brand matches most of the benefit for less.
What cheaper alternatives match a premium hiking pack?
Second-tier technical brands at roughly $100–$180, previous-season clearance, and OEM/ODM builds all deliver the same shell fabric, frame and suspension grade while trimming most of the design and brand margin. The spec you want is buyable under any label.
Can I get a premium-grade hiking pack built under my own brand?
Yes. Premium technical hiking packs are manufactured through global partners in the same specialized factories that build private-label packs worldwide. Our affiliated factory works within a vetted partner-factory network rather than a single captive shop, and can spec a made-to-order suspension pack with torso sizing and high-denier shell for your brand.
How much does a premium hiking pack cost to make?
A made-to-spec technical or expedition hiking pack carries a factory build cost of roughly $55–$110 (typical) depending on capacity, fabric grade, suspension complexity and volume. Against a retail ticket of roughly $180–$350 (approx.), the difference is absorbed by design, brand, distribution, warranty service and retail margin.
Disclaimer: Retail and factory figures in this article are industry-typical approximations used to explain cost structure – not precise quotes or guaranteed prices. Actual pricing depends on your specification, volumes and prevailing conditions. Approx./typical labels apply to every figure above.
OEM perspective note: JUNYUAN BAGS operates as a backpack trading and sourcing organization backed by an affiliated factory and partner factories in Quanzhou, Fujian. We do not claim to manufacture for any named brand, nor do we represent any brand’s proprietary design. Figures describe the open, buyable spec that any brand can source.