Custom Premium Backpack Manufacturer — OEM/ODM for High-End and Luxury Backpack Brands
JUNYUAN BAGS builds premium backpacks on an OEM and ODM basis for brands that sell on construction, not on price. That means ballistic nylon that still holds its shape after two years of daily carry, seams that survive a 30 kg pull test, YKK hardware that does not corrode, and a lining nobody has to apologise for. We are a bag manufacturer based in Quanzhou, Fujian, China, founded in 2014, with a founding team that has been in bag production since 2004.
Our standard programme runs at a minimum order quantity of 500 pieces per style and colour, sampling in 6–10 business days, mass production in 35–50 days, and final inspection to AQL 2.5 / 4.0. Production is delivered through our affiliated and partner factories, which we audit and hold to the same specification we agree with you on the golden sample.
Request a premium backpack quote — email [email protected] or WhatsApp +86 17750020688. Send a tech pack, a reference sample, or even a mood board; we reply with a costed specification and a realistic timeline, usually within 12 hours on business days.

What “Premium” Actually Means in Backpack Manufacturing
“Premium” is one of the most abused words in the bag trade. On an Alibaba listing it usually means a nicer photo. In a factory it means something measurable, and that measurement is almost entirely about what happens at the seams, the hardware, and the lining — the three places a buyer touches first and a returns department hears about last.
When a brand tells us they want to move up from a mid-market backpack to a premium one, the conversation is not about adding features. It is about removing tolerance for things that used to be acceptable. A mid-market bag can have a 6-stitch-per-inch seam, a #5 nylon coil zip, a 210D polyester lining, and a stamped steel slider. A premium bag in the same silhouette will typically run 8–10 stitches per inch, a #8 or #10 YKK VISLON or a metal Excella zip, a 210D or 300D ripstop lining with a PU backer, and a die-cast zinc slider with a matte finish. The bag looks similar in a photo. The cost difference is 35–60%, and the return rate difference is larger than that.
The Four Cost Drivers That Separate Premium from Mid-Market
| Cost driver | Mid-market typical | Premium typical | Effect on FOB |
|---|---|---|---|
| Shell fabric | 600D polyester, PU coated | 1680D ballistic nylon, 500D Cordura, X-Pac VX21, or 1.2–1.4 mm full-grain leather | +18% to +45% |
| Zippers and hardware | Generic #5 coil, painted steel | YKK #8/#10, Duraflex or Woojin die-cast, PVD or anodised finish | +8% to +15% |
| Lining and internals | 210D polyester, unbacked | 300D ripstop with PU backer, brushed tricot device pockets, EVA structure board | +5% to +11% |
| Construction labour | 6–7 SPI, single-needle, bound edges | 8–10 SPI, double-needle or French seams, folded and stitched edges, bartacked stress points | +12% to +25% |
Where Premium Brands Actually Spend Their Margin
A useful exercise for any product manager: take your target retail price, strip out retail margin, distributor margin, freight and duty, and see what FOB number you are actually working with. Premium brands that succeed usually spend that FOB budget in a specific order of priority, and it is rarely the order people assume.
- First: structural integrity. Foam density in the shoulder straps, a PE or HDPE back panel that does not fold under load, bartacks at every strap junction. This is invisible and it is the single biggest driver of “this feels expensive” feedback in reviews.
- Second: hardware. Buyers judge zips by sound and resistance. A cheap slider that rattles destroys a premium impression faster than any other single component, and it is one of the cheapest things to upgrade.
- Third: the lining. A premium exterior with a shiny, thin, unbacked lining reads as counterfeit-adjacent. Ripstop with a visible grid, a contrasting colourway, and a soft-touch finish costs very little and photographs extremely well.
- Fourth: the shell fabric. Counter-intuitively this is often last, because a well-built 900D polyester outperforms a badly built ballistic nylon in the field, and most consumers cannot tell them apart in a showroom.
We build a costed bill of materials with you at the sampling stage so you can see exactly what each upgrade adds per unit at your order quantity. That is the only honest way to decide where the premium budget goes.
Premium Backpack Materials: The Specification Menu
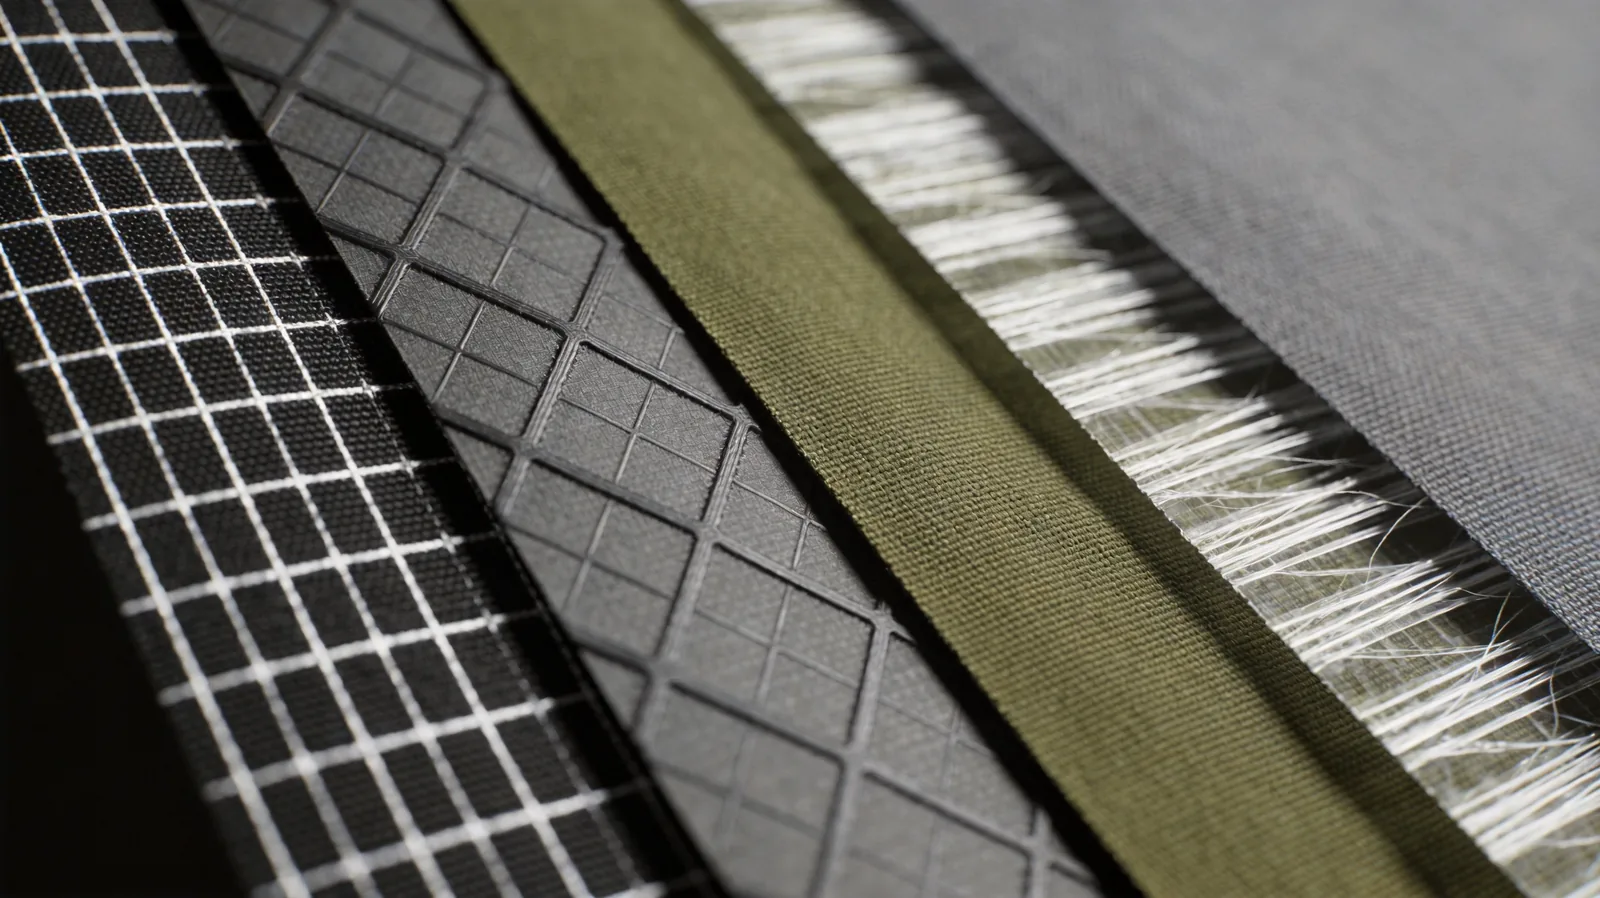
Below is the material menu we work from most often for premium backpack programmes. It is not exhaustive — if you have a nominated mill or a supplier you already buy from, we will quote against your nominated material and confirm its handling behaviour on our machines before sampling.
| Component | Common premium specs | Why it matters | Notes |
|---|---|---|---|
| Shell fabric | 1680D ballistic nylon; 500D/1000D Cordura; X-Pac VX21/VX42; 18 oz waxed canvas; 1.2–1.4 mm full-grain leather | Abrasion resistance, shape retention, hand feel | Ballistic nylon needs a PU backer to stop fraying at cut edges |
| Lining | 210D–300D ripstop polyester with PU backer; 70D taslan; brushed tricot for device pockets | Perceived quality, internal abrasion, device protection | Contrast lining is the cheapest premium signal available |
| Zippers | YKK #8/#10 VISLON; YKK Excella metal; water-resistant matte PU-coated coil | Cycle life, water ingress, sound and feel | Specify slider finish separately from tape colour |
| Hardware | Duraflex, Woojin or YKK die-cast; acetal D-rings; anodised aluminium G-hooks | Load rating, corrosion, premium tactility | Ask for load test data, not just a brand name |
| Webbing | PP webbing 25–38 mm; nylon webbing for load paths; seatbelt webbing for top handles | Strap comfort and long-term stretch | PP is lighter and cheaper; nylon resists UV and abrasion better |
| Foam | PE 8–12 mm shoulder; EVA 3–5 mm structure; memory foam lumbar | Carry comfort, pack shape, recovery after compression | Foam density matters more than thickness |
| Structure | HDPE back panel 0.8–1.2 mm; PE board base; aluminium stay | Prevents pack collapse when loaded | This is what makes an empty bag stand up on a shelf |
| Thread | Bonded nylon 69/92/138; UV-stabilised polyester | Seam strength and colour fastness | Bonded nylon for load seams; polyester acceptable elsewhere |
Shell Fabrics: Ballistic Nylon, Cordura, X-Pac, Waxed Canvas, Full-Grain Leather
Ballistic nylon is the default for premium business and travel backpacks. The 1680D weave gives a tight, slightly lustrous surface that resists abrasion and holds a shape, and it takes a matte PU coating well. Its weakness is cut-edge fraying, so it needs a PU backer and either bound or folded seams. It is also heavier than people expect — a 1680D ballistic backpack shell will typically add 180–260 g over a 600D polyester equivalent.
Cordura in 500D or 1000D is the outdoor and technical default. It is a nylon 6,6 with a rougher, more matte hand and better tear strength per gram than most ballistic weaves. For hiking and commuter crossover programmes we usually recommend 500D Cordura on the body with 1000D on the base.
X-Pac and other laminated sailcloth (VX21, VX42, RX30) are dimensionally stable, fully waterproof as a laminate, and have a distinctive diagonal grid that reads as technical. They are the fastest way to signal “premium technical” but they are stiff, they crease permanently along fold lines, and they cannot be sewn with the same seam allowances as a woven. Budget extra sampling time if you are moving a woven pattern onto a laminate.
Waxed canvas (18 oz and up) is the heritage and lifestyle choice. It develops patina, it is repairable, and it photographs beautifully. It also transfers wax onto light-coloured clothing in warm climates, which is a genuine consumer complaint you should plan a care card for.
Full-grain leather in 1.2–1.4 mm is the top of the ladder. At this level the specification question shifts from “which leather” to “which tannery, which retanning, and what is the finish”. We work with nominated tanneries and can confirm chrome-free and vegetable-tanned options with the relevant documentation.

Linings and Interlinings
The lining is where most mid-market factories save money and where most premium brands lose the sale in a showroom. Three practical rules:
- Use a PU-backed ripstop, not a plain taffeta. The backer stops the weave from shifting and prevents the lining from ballooning inside the bag after a few months of use.
- Specify a contrast colourway. A charcoal exterior with a burnt-orange or sand lining is a two-dollar upgrade at 500 pieces and is one of the most photographed details in unboxing content.
- Where devices go, use brushed tricot or a velvet-faced pocket, and pad it with 3–5 mm EVA. A laptop sleeve that lets a laptop slide straight onto a zip pull is a warranty claim waiting to happen.
Hardware and Zippers
Hardware is the highest-leverage upgrade in the entire bill of materials. Moving from generic painted steel to die-cast zinc from Duraflex, Woojin or YKK typically adds 8–15% to FOB and completely changes how the bag feels in the hand. Two specifics worth insisting on:
- Ask for cycle test data on the zips, not just the brand. YKK publishes cycle life; a #8 VISLON under normal use should comfortably exceed the number of cycles a bag sees in five years, but the tape and the stitching around the zip ends fail first in practice.
- Specify slider finish separately from tape colour. Matte black sliders on a black tape look premium; glossy black sliders on a black tape look like a school bag. This is a one-line instruction in the tech pack that is frequently omitted.
Foams, Frames and Structure
A premium backpack has to hold its shape when empty and recover when crushed. That is a structure question, not a fabric question, and it is where a lot of otherwise good programmes fall down. The three components that matter:
- HDPE back panel, 0.8–1.2 mm. Gives the pack a spine, distributes load, and stops the back from folding into the wearer. Without it, even a good ballistic nylon bag looks like a stuff sack.
- PE board base. Prevents the bottom sagging under weight, which is what makes a loaded bag look cheap in a customer photo.
- Foam density, not thickness. A 10 mm 45-density shoulder strap outperforms a 15 mm 25-density strap on comfort and lasts longer. Ask for the density number.
Construction Details That Premium Buyers Inspect First
If you have ever watched an experienced buyer handle a sample, you have watched this sequence: they open every zip, they turn the bag inside out, they pull the shoulder strap hard, they look at the seam at the base of the strap, and then they squeeze the back panel. Those five moves map exactly onto the five construction decisions that separate a premium programme from a mid-market one.
Stitch Density and Seam Type
Stitch density is the fastest objective test available to anyone with eyes. Mid-market bags run 6–7 stitches per inch; premium bags run 8–10. Below 6 the seam looks coarse and loses strength; above 11 you start perforating the fabric and reducing tear strength, so more is not better. Alongside density, the seam type matters:
- Double-needle seams on all load-bearing joins (strap to body, base to body, handle attachments).
- French seams or bound seams on the lining so there are no raw edges visible when the bag is opened.
- Folded and stitched edges on pockets and flaps rather than cut-and-bind, which is the single clearest tell of a premium build.
Edge Finishing
Raw or bound edges on a lining are the most common place a premium bag reveals itself as mid-market. Folded-and-stitched edges take roughly 1.6× the labour of a bound edge but eliminate the fraying, the loose thread tails, and the scratchy feel that generates one-star reviews. On leather goods the equivalent decision is edge paint versus burnishing, and at the premium end you should specify which.
Related: custom leather bags covers the leather-specific finishing options in more depth.
Bartacks and Stress Points
Every strap junction, every D-ring attachment, every zip end needs a bartack — a short, dense zigzag or box-X stitch that distributes load. A premium specification should name the bartack type and the stitch count per bartack. Skipping bartacks saves a few cents per bag and is the direct cause of the “strap tore off after three months” return.
We test this. A finished sample goes on a pull rig and the strap junction is loaded to 30 kg for a sustained hold. If a bartack or a seam fails, the pattern goes back, not the production run.
Laptop Compartment and Suspension
For business and commuter premium backpacks, the laptop compartment is the feature buyers evaluate hardest. The specification we recommend as a baseline:
- Suspended sleeve: the laptop must not touch the base of the bag. A 20–25 mm clearance above the base line is standard.
- 3–5 mm EVA foam on both faces, with a brushed tricot face on the device side.
- A vertical zip opening with a storm flap, positioned so the bag does not have to be laid flat to extract a 16-inch laptop.
- A separate tablet sleeve in front of the laptop sleeve, sized for a 11-inch tablet, in the same tricot.
For hiking and technical programmes the equivalent is the suspension system — ventilated back panel, load-lifter straps, and a hip belt that actually transfers weight rather than just closing around the waist. See custom hiking backpack manufacturing for that specification set.

OEM vs ODM vs Private Label — Which Model Fits Your Premium Line
Brands arrive at a premium programme from three different starting points, and picking the wrong model is the most expensive mistake available. The distinction is about who owns the design and who carries the development risk.
| Model | Who owns the design | What we provide | Typical MOQ | Best for |
|---|---|---|---|---|
| OEM (full custom) | You — from your tech pack | Pattern making, material sourcing against your spec, sampling, tooling, production, inspection | 500 pcs per style and colour | Brands with an in-house design team and an established silhouette |
| ODM (adapt our design) | Us, adapted to your brand | A base silhouette from our library, modified to your materials, colours, logo and features | 500 pcs per style and colour | Brands entering premium with no design resource, or testing a new category |
| Private label | Us, unmodified | An existing silhouette with your branding, labels, hangtags and packaging | 500 pcs per style and colour | Fast market entry, promotional premium lines, corporate gifting |
A practical warning about the middle path: many brands ask for ODM and then, halfway through sampling, start specifying bespoke hardware and a new pattern. That is OEM work priced as ODM, and it is the usual reason premium programmes slip their launch date. Decide the model before the first sample, not during the third.
For a broader view of the full custom route, see custom backpack manufacturer, which covers the general OEM/ODM workflow across sports, laptop, school and promotional backpacks.
MOQ, Tooling and the Real Cost of a Premium Programme
Price per unit is the number everyone asks for first and the number that matters least on its own. What actually determines whether a premium backpack programme makes money is landed cost per sellable unit, and that includes tooling amortisation, freight, duty and the defect rate you have to absorb.
MOQ Structure
Our standard minimum order quantity is 500 pieces per style and colour. Golf bag programmes run at 200 pieces because the construction is a different product family with different material economics. What “per style and colour” means in practice:
- 500 pieces of one design in one colourway is the cleanest and cheapest unit price.
- 500 pieces split across two colourways is usually acceptable with a modest surcharge, because the cutting and the trims change but the pattern does not.
- Below 500, tooling and set-up costs are spread over too few units and the per-unit price rises sharply. If you need a small run to test a market, the honest answer is usually to test with an existing silhouette rather than a new one.
Volume pricing typically begins to move at 5,000 pieces and again at 20,000, and repeat clients on proven designs can often flex the entry point. Ask; it is a commercial conversation, not a policy wall.
Tooling and Development Charges
| Item | Typical charge | Notes |
|---|---|---|
| Pattern making (new silhouette) | Quoted per design | Waived on repeat orders of the same pattern |
| Sample fee (first round) | Quoted per sample | Refunded against the first bulk order once it reaches the agreed value |
| Custom logo tooling — metal plate, emboss die | Quoted per design | One-off; plate stays with the tooling and is reused on repeats |
| Custom hardware (bespoke mould) | Quoted per design | Highest tooling cost; only justified at volume or across multiple styles |
| Lab testing (per material or per style) | Quoted per test | Charged at cost; reports are yours to keep and reuse |
Landed Cost: FOB, Freight, Duty and HS Code
FOB Xiamen or FOB Shenzhen is our standard Incoterm. From there, a premium backpack typically lands at 1.35–1.6× FOB once ocean freight, insurance, duty and destination charges are included — and the ratio is worse on air freight, which is why premium programmes with a fixed launch date need their production slot booked early.
- HS classification. Most backpacks classify under HS 4202.92. Depending on the destination and the exact construction, duty rates vary substantially between the US, the EU and the UK. We provide the material composition and construction details your customs broker needs, but the classification decision and the duty calculation are yours to confirm.
- Freight mode. Sea freight for volume, air for launch-critical top-ups. A premium programme that misses its season by three weeks usually loses more margin than the air freight would have cost.
- Duty engineering. Material substitution and construction changes can move a product between duty treatments. We will tell you honestly when a change is worth exploring and when it is not.
Sampling: From Tech Pack to Golden Sample
Sampling is where a premium programme is won or lost. A factory that samples quickly but loosely will cost you three rounds and a missed season; a factory that samples precisely in 6–10 business days will get you to approval in one or two rounds. Our sampling window is 6–10 business days from the point we have a complete specification and approved materials.
What We Need From You
- A tech pack — dimensioned drawings or a CAD file, with seam allowances, stitch callouts, hardware placement and tolerance.
- Material specification — or a nominated supplier. If you have no spec, send a physical sample and we will reverse-engineer the specification and confirm it in writing before cutting.
- Branding assets — logo files in vector, label and hangtag artwork, and the placement diagram.
- Target FOB and target retail, honestly stated. A factory that knows the budget can propose substitutions that keep the design intent inside it. A factory guessing at the budget will over-specify and waste a round.
- Compliance requirements — destination market, any retailer-specific testing protocol, and any material certifications you must be able to claim.
The 6–10 Business Day Sampling Window
The clock starts when three things are true: the specification is signed off, the materials are either in hand or confirmed available, and the branding artwork is approved. Before that point, the sample is a sketch and will be redone. We would rather tell you the clock has not started than deliver a sample that misses because a zip colour was still undecided.
Round one is about construction and proportion. Round two is about materials and finish. Round three should not normally be necessary — if it is, something in the specification was ambiguous, and the fix is a clearer spec rather than a faster sample.
PP Sample and Golden Sample Approval
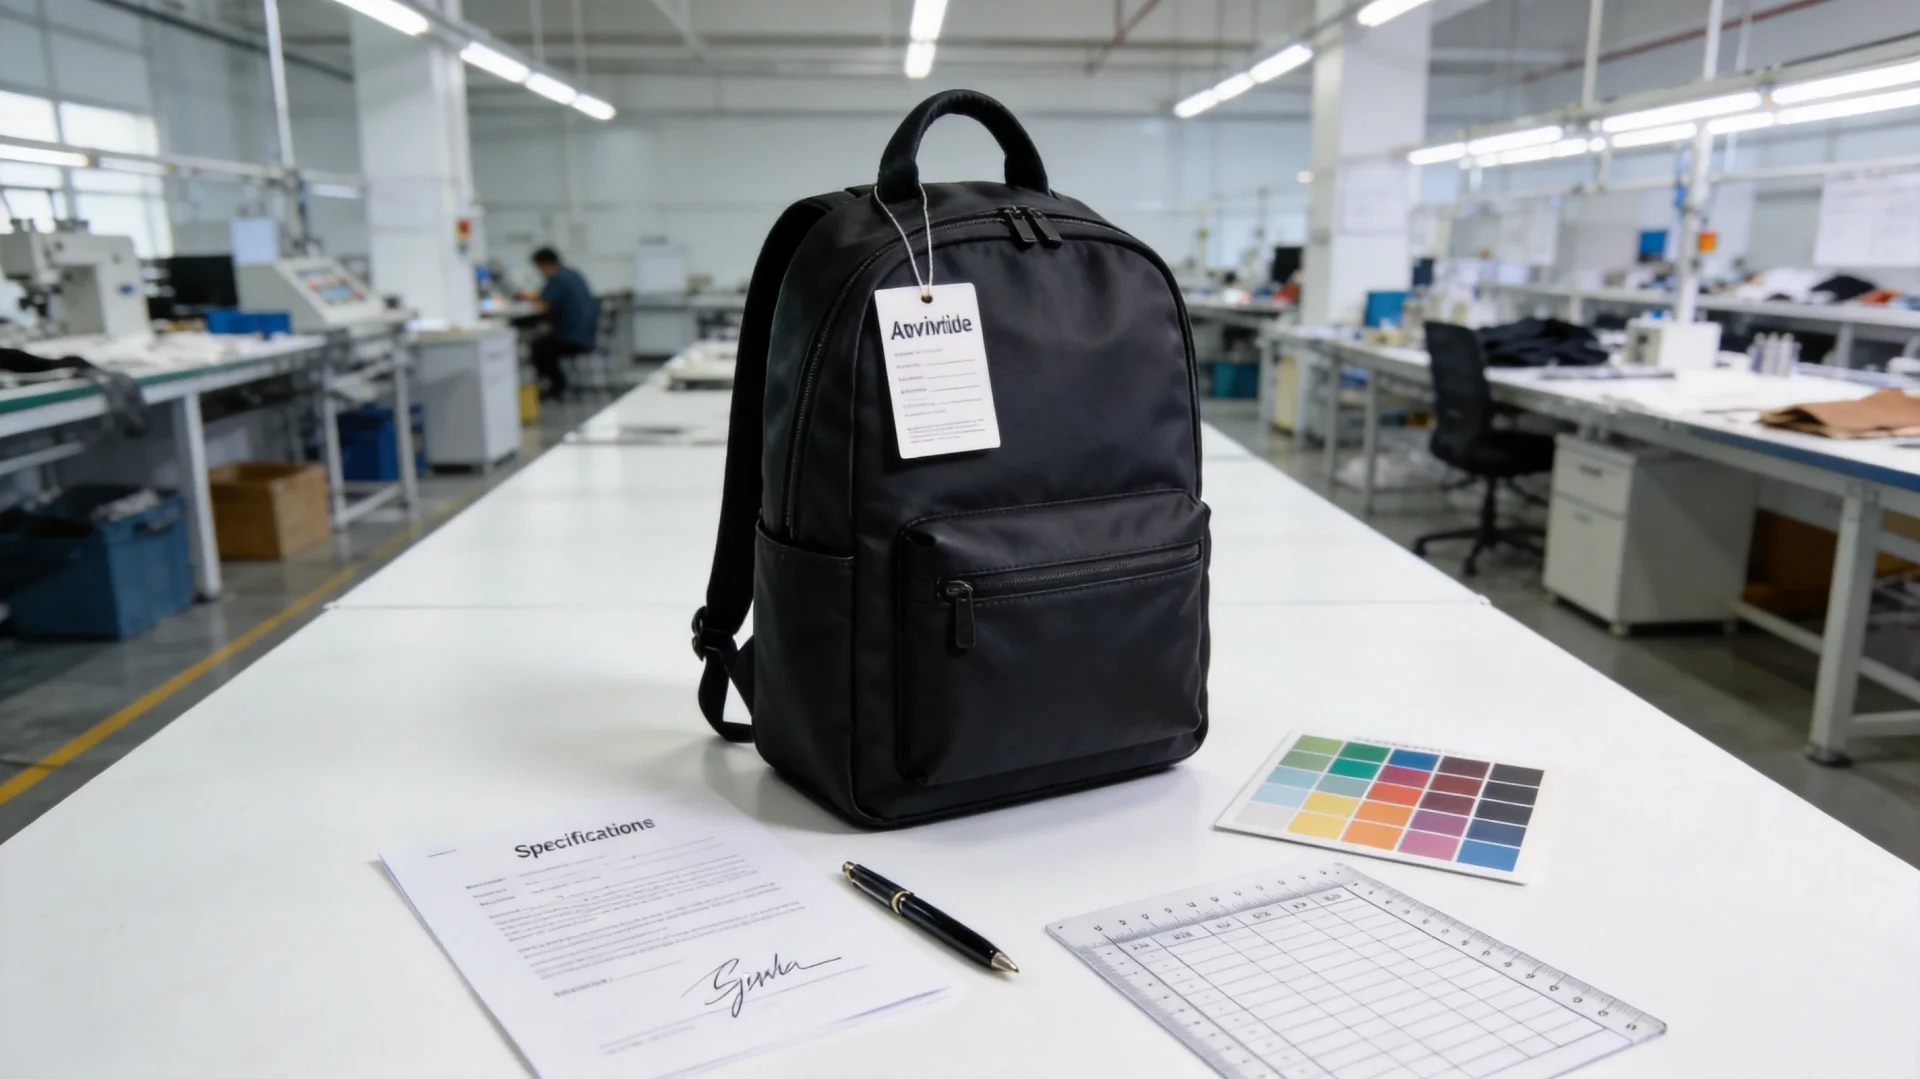
Two approvals matter, and they are not the same thing. The PP (pre-production) sample confirms that production tooling, materials and methods will produce the approved design — it is made on the production line, with production materials, before the run starts. The golden sample is the signed-off reference unit, sealed and held, against which every subsequent inspection is judged.
We do not start a bulk run without a signed golden sample. If you are working to a launch date, this is the milestone to protect, not the ship date.
Quality Control and AQL 2.5 / 4.0
Our inspection standard is AQL 2.5 for major defects and AQL 4.0 for minor defects, applied at final inspection on a statistically valid sample drawn from the finished lot. That is the same standard most premium retailers impose on their own suppliers, which means our inspection report is usually usable as evidence rather than as a starting point for argument.
Inline Inspection vs Final Inspection
Final inspection catches problems; inline inspection prevents them. On premium programmes we run both:
- Inline — a first-article check at the start of the run, then periodic checks through cutting, stitching and assembly. This is where a mis-set seam allowance or a wrong thread colour gets caught at 50 pieces instead of 5,000.
- Final — the AQL 2.5 / 4.0 inspection on the finished lot, with a photo set, a measurement report against the golden sample, and a pass/fail call.
What Gets Checked
| Category | What is measured |
|---|---|
| Dimensions | Key dimensions against the golden sample, within the agreed tolerance |
| Construction | Stitch density (SPI), seam type, bartack presence and density, edge finishing |
| Function | Every zip cycled, every buckle engaged, every strap adjusted through full travel |
| Hardware | Load test on strap junctions and handle attachments; corrosion visual check |
| Materials | Shade matching across panels and against the approved swatch; backing and coating integrity |
| Cleanliness | Thread tails, chalk marks, oil stains, adhesive residue, needle holes |
| Branding | Logo position, orientation, registration, label and hangtag correctness |
| Packing | Polybag, desiccant, carton count, carton drop test, shipping mark accuracy |
Test Reports and Documentation
Every shipment can be accompanied by an inspection report and a photo set. Material test reports — abrasion, tear strength, colour fastness, water resistance, and where relevant REACH, Prop 65, CPSIA and GRS — are provided at cost and are yours to keep and reuse across programmes, which is useful when a retailer asks for evidence on a material you have already tested.

Compliance and Documentation for Premium Retail
Premium retail channels ask harder compliance questions than mid-market ones, and a programme that cannot produce documentation stalls at the buyer meeting rather than at the port. The list below is what we are routinely asked for and can normally support; the specifics of which certificates apply to your programme are confirmed at quotation.
Factory and Social Compliance
Our affiliated and partner factories hold social compliance audit documentation and quality management certification appropriate to the markets they serve. Because production is distributed across a partner network rather than a single owned facility, we confirm which specific facility will run your order and provide that facility’s documentation before you commit. That is a more honest arrangement than presenting a single certificate that may not apply to the line your bags are actually made on.
If your retailer requires a named facility with a specific audit grade, tell us at the RFQ stage and we will confirm availability before quoting. Retrofitting a compliance requirement onto a booked production slot is the most common cause of a delayed premium launch.
Material Certificates
- GRS (Global Recycled Standard) — for recycled polyester and recycled nylon programmes, with transaction certificates through the supply chain.
- REACH — for EU destinations, covering restricted substances in the finished article.
- Prop 65 — for California, with the relevant warnings or the testing to justify not using them.
- CPSIA — for US children’s products, which applies to school backpack programmes.
- OEKO-TEX Standard 100 — for textile components in contact with skin.
Lab Testing
Third-party lab testing is arranged at cost against your destination market and your retailer’s protocol. Typical tests on a premium backpack programme are Martindale abrasion on the shell, tear strength on the base, colour fastness to rubbing and to light, water resistance on coated fabrics, and zip cycle life. Testing can run in parallel with sampling so that it does not add to the critical path.
Lead Times, Capacity and Production Planning
Lead times are the part of a premium programme most often quoted optimistically and delivered late. These are the numbers we hold ourselves to, and the conditions attached to each.
| Stage | Duration | Starts when |
|---|---|---|
| Quotation and specification review | 2–4 business days | Complete RFQ received (tech pack or reference sample, target quantity, target market) |
| Material sourcing and confirmation | 3–10 business days | Specification agreed; nominated materials located and stock confirmed |
| Sampling | 6–10 business days | Specification signed off, materials in hand, artwork approved |
| Sample revision (if required) | 5–8 business days | Written revision notes received |
| PP sample and golden sample approval | 5–8 business days | Sample approved in principle |
| Bulk production | 35–50 days | Deposit received and golden sample signed |
| Final inspection | 1–2 days | Production complete |
| Documentation and shipment booking | 3–5 days | Inspection passed and balance arrangements confirmed |
The realistic total from a standing start to a shippable order is therefore around 10–13 weeks, and 12–16 weeks if the programme needs a second sample round or third-party lab testing on the critical path. Plan backwards from your retail window and protect the golden sample milestone.
Two planning notes that save programmes:
- Chinese New Year. Production in Fujian effectively stops for two to four weeks around the Spring Festival, and the weeks either side are congested. If your launch lands in Q2, book the production slot before December.
- Peak season. August to October is the busiest window for bag export production. A premium programme that needs a November ship date should be in sampling by June.
Payment Terms, Incoterms and Logistics
Payment Terms
Our standard terms are 30% deposit with the order, and the balance against a copy of the bill of lading. That structure protects both sides: the deposit funds materials and secures the production slot, and the balance is released once the goods are demonstrably on board. For long-standing clients with an established trading history we can discuss alternative structures case by case.
We do not ask for full payment upfront on a first order, and we would be cautious about any supplier who does on a premium programme — it usually means they cannot fund the materials.
Incoterms
We quote FOB Xiamen or FOB Shenzhen as standard. Both ports have direct sailings to North America, Northern Europe and the Mediterranean, and both are within a day’s trucking of our production base in Quanzhou. Other Incoterms — CIF, CFR, DAP — can be quoted if your forwarder arrangements require them, but FOB keeps the freight decision and the freight cost with you, which is usually cheaper and always more transparent.
Air, Sea or Rail
- Sea freight — the default for volume. Roughly 25–40 days door to door depending on the lane. Book early; premium programmes in peak season compete for the same space as everyone else.
- Air freight — for launch-critical top-ups and for sample shipments. Economically sensible only for a fraction of an order, but cheaper than missing a retail window.
- Rail to Europe — a middle option on the China–Europe lane, typically 18–25 days, useful when sea is too slow and air is too expensive.
We ship on your forwarder or ours, provide the full export documentation set, and can consolidate with other suppliers if you are managing multiple categories out of Fujian.
Why Brands Build Premium Backpack Programmes With JUNYUAN BAGS
JUNYUAN BAGS was founded in 2014, and our founding team has been in bag manufacturing since 2004. We are a bag manufacturer and exporter based in Quanzhou, Fujian — the same industrial cluster that supplies a large share of the world’s premium bag production. Our legal entity is QUANZHOU JUNYUAN COMMERCIAL AND TRADING CO., LTD., and our registered address is C201-207, Huachuang Park, Tiyu Street, Huada Street, Fengze District, Quanzhou City, Fujian Province, China.
Our premium backpack programmes run through a network of affiliated and partner factories that we audit, specify and hold to the golden sample. We are direct about this because it is the arrangement that lets us match the right facility to the right construction — a leather goods line for a full-grain programme, a technical line for a laminated sailcloth programme, a volume line for a 20,000-piece rollout — rather than forcing every programme through one building.
What we bring to a premium programme specifically:
- Specification literacy. We can read a tech pack and we can also build one from a reference sample. If your team has no technical designer, that gap gets closed at the sampling stage rather than discovered at inspection.
- Material access. Ballistic nylon, Cordura, X-Pac laminates, waxed canvas, full-grain leather, YKK and Duraflex hardware, and GRS-certified recycled fabrics are all sourced and confirmed before sampling rather than promised on a quotation.
- Honest lead times. 6–10 business days sampling and 35–50 days production are numbers we hold. If a programme cannot hit them, we say so at quotation.
- Inspection you can hand to a retailer. AQL 2.5 / 4.0 with a measurement report and photo set, benchmarked against a sealed golden sample.
- Category depth. Beyond premium backpacks we manufacture custom laptop backpacks, hiking backpacks, waterproof bags, travel bags and duffel bags, so a premium line can be built across categories on one supplier relationship.
We also manufacture under our own registered trademark, KEEP PERFECT, which means we have sat on the brand side of the sampling table and know what a launch date actually costs when it slips. Read more about JUNYUAN BAGS.
Frequently Asked Questions
What is the minimum order quantity for a custom premium backpack?
Our standard MOQ is 500 pieces per style and colour. Golf bag programmes run at 200 pieces. For a first order we can sometimes be flexible on a proven silhouette, but a brand-new premium pattern below 500 pieces usually cannot absorb the tooling and set-up cost without a price increase.
How long does sampling and production take?
Sampling takes 6–10 business days once the specification is signed off, the materials are confirmed, and the branding artwork is approved. Mass production takes 35–50 days from deposit and golden sample sign-off. End to end, from a complete RFQ to a shippable order, is realistically 10–13 weeks.
Can you match the quality of a premium benchmark brand?
Yes, and we will show you how. Send us a physical benchmark sample and we will reverse-engineer the specification — fabric, denier, stitch density, hardware, foam density, structure board — and quote against it line by line. What we will not do is claim a brand relationship we do not have. We manufacture to a specification; we do not manufacture for named premium brands unless that is a documented arrangement.
Which premium materials can you source?
1680D ballistic nylon, 500D and 1000D Cordura, X-Pac VX21 and VX42 laminates, 18 oz waxed canvas, full-grain leather from 1.2 to 1.4 mm, GRS-certified recycled polyester and nylon, YKK zips (VISLON, Excella, water-resistant PU-coated), Duraflex and Woojin die-cast hardware, and YKK or Duraflex acetal and aluminium fittings. If you have a nominated mill, we will quote against your material.
Can you work from our tech pack?
Yes, that is our normal OEM route. We work from dimensioned drawings or CAD files and will flag specification gaps before sampling rather than filling them with assumptions. If you have no tech pack, send a physical reference sample and we will build the specification from it and confirm it in writing before cutting.
What is your inspection standard?
AQL 2.5 for major defects and AQL 4.0 for minor defects at final inspection, on a statistically valid sample from the finished lot. We also run inline checks through cutting, stitching and assembly. Every shipment can be accompanied by an inspection report, a measurement report against the golden sample, and a photo set.
What are your payment terms?
30% deposit with the order and the balance against a copy of the bill of lading. We quote FOB Xiamen or FOB Shenzhen as standard. CIF, CFR and DAP can be quoted if your forwarder arrangements require them.
Do you provide material and factory compliance documentation?
Yes. GRS transaction certificates, REACH and Prop 65 documentation, CPSIA where applicable, and OEKO-TEX Standard 100 for skin-contact textiles are all available at cost. Social compliance and quality management documentation is provided for the specific partner facility that will run your order, confirmed at quotation.
What is the difference between OEM and ODM in your programme?
In OEM you own the design and provide the tech pack; we build to it. In ODM you start from a silhouette in our library and we modify it to your materials, colours, logo and features. Private label means an unmodified existing design with your branding. The model changes the development cost and the timeline, so it should be settled before the first sample.
Can you handle a premium line across several bag categories?
Yes. Premium backpacks, laptop backpacks, hiking backpacks, travel bags, duffel bags, waterproof bags, tote bags, golf bags and medical bags are all in-house categories, so a premium collection can be developed across categories on one supplier relationship with consistent materials and finishing standards.
Start Your Premium Backpack Programme
Send us one of three things and we can move: a tech pack, a physical reference sample, or a written brief with your target retail price and quantity. From any of those we will come back with a costed specification, a material recommendation, and a timeline you can put in front of your board.
Contact JUNYUAN BAGSEmail: [email protected]WhatsApp / Phone: +86 17750020688Address: C201-207, Huachuang Park, Tiyu Street, Huada Street, Fengze District, Quanzhou City, Fujian Province, ChinaCompany: QUANZHOU JUNYUAN COMMERCIAL AND TRADING CO., LTD.Response time: within 12 hours on business days